Automotive sheet metal parts form the structural skeleton, protective enclosures, and mechanical mounting framework of modern passenger vehicles, commercial trucks, and electric vehicles (EVs). From high-strength body-in-white (BIW) reinforcements and chassis subframe crossmembers to intricate sensor brackets and deep-drawn battery module covers, sheet metal components deliver an optimized balance of structural rigidity, impact energy absorption, and lightweight performance. Global automotive original equipment manufacturers (OEMs) and Tier 1/Tier 2 suppliers rely on dedicated stamping dies and automated press lines to cold-form raw steel and aluminum coils into millions of uniform, high-precision parts each year.
1. Automotive Sheet Metal Parts: Definition and Manufacturing Scope
1.1 What Are Automotive Sheet Metal Parts?
1.1.1 Definition and role in automotive manufacturing
Automotive sheet metal parts are custom-formed components produced from thin-to-medium gauge flat metal sheets or continuous coils (typically 0.6 mm to 6.0 mm thick) through cold-forming operations such as stamping, shearing, bending, and deep drawing. These parts represent over 50% of the total metallic weight in a typical passenger car, providing structural integrity, aerodynamic profiles, mounting points, and crash safety barriers throughout the vehicle.
1.1.2 Automotive sheet metal parts vs fabricated sheet metal components
Automotive stamped sheet metal parts differ significantly from general fabricated sheet metal components. General fabrication relies on CNC laser cutting, turret punching, and manual press-brake bending, which is suitable for low-volume industrial enclosures or prototypes. In contrast, automotive sheet metal parts utilize dedicated, hardened tool-steel stamping dies and automated presses. This tooling delivers sub-second cycle times, consistent dimensional repeatability (down to ± 0.01 mm), and the structural economy required for mass-production vehicle platforms.
1.1.3 Automotive sheet metal parts vs CNC-machined components
CNC machining is a subtractive process that carves parts from solid metal blocks, producing significant scrap chips and requiring lengthy cycle times measured in minutes or hours. Automotive sheet metal stamping deforms flat stock plastically within matched die cavities in fractions of a second. This cold-forming process maximizes raw material utilization, aligns the metal’s internal grain structure to enhance fatigue strength, and yields per-part manufacturing costs that are significantly lower than machined alternatives at scale.
1.2 Where Automotive Sheet Metal Parts Are Used
1.2.1 Body-in-White (BIW) components
Body-in-White (BIW) refers to the welded sheet metal shell of a vehicle before the installation of doors, powertrain components, exterior glass, or interior trim. Stamped sheet metal forms the entire monocoque structure-including roof rails, floor pans, B-pillars, wheel arches, front crash boxes, and firewall bulkheads-engineered to manage load distribution during vehicle rollovers and collisions.
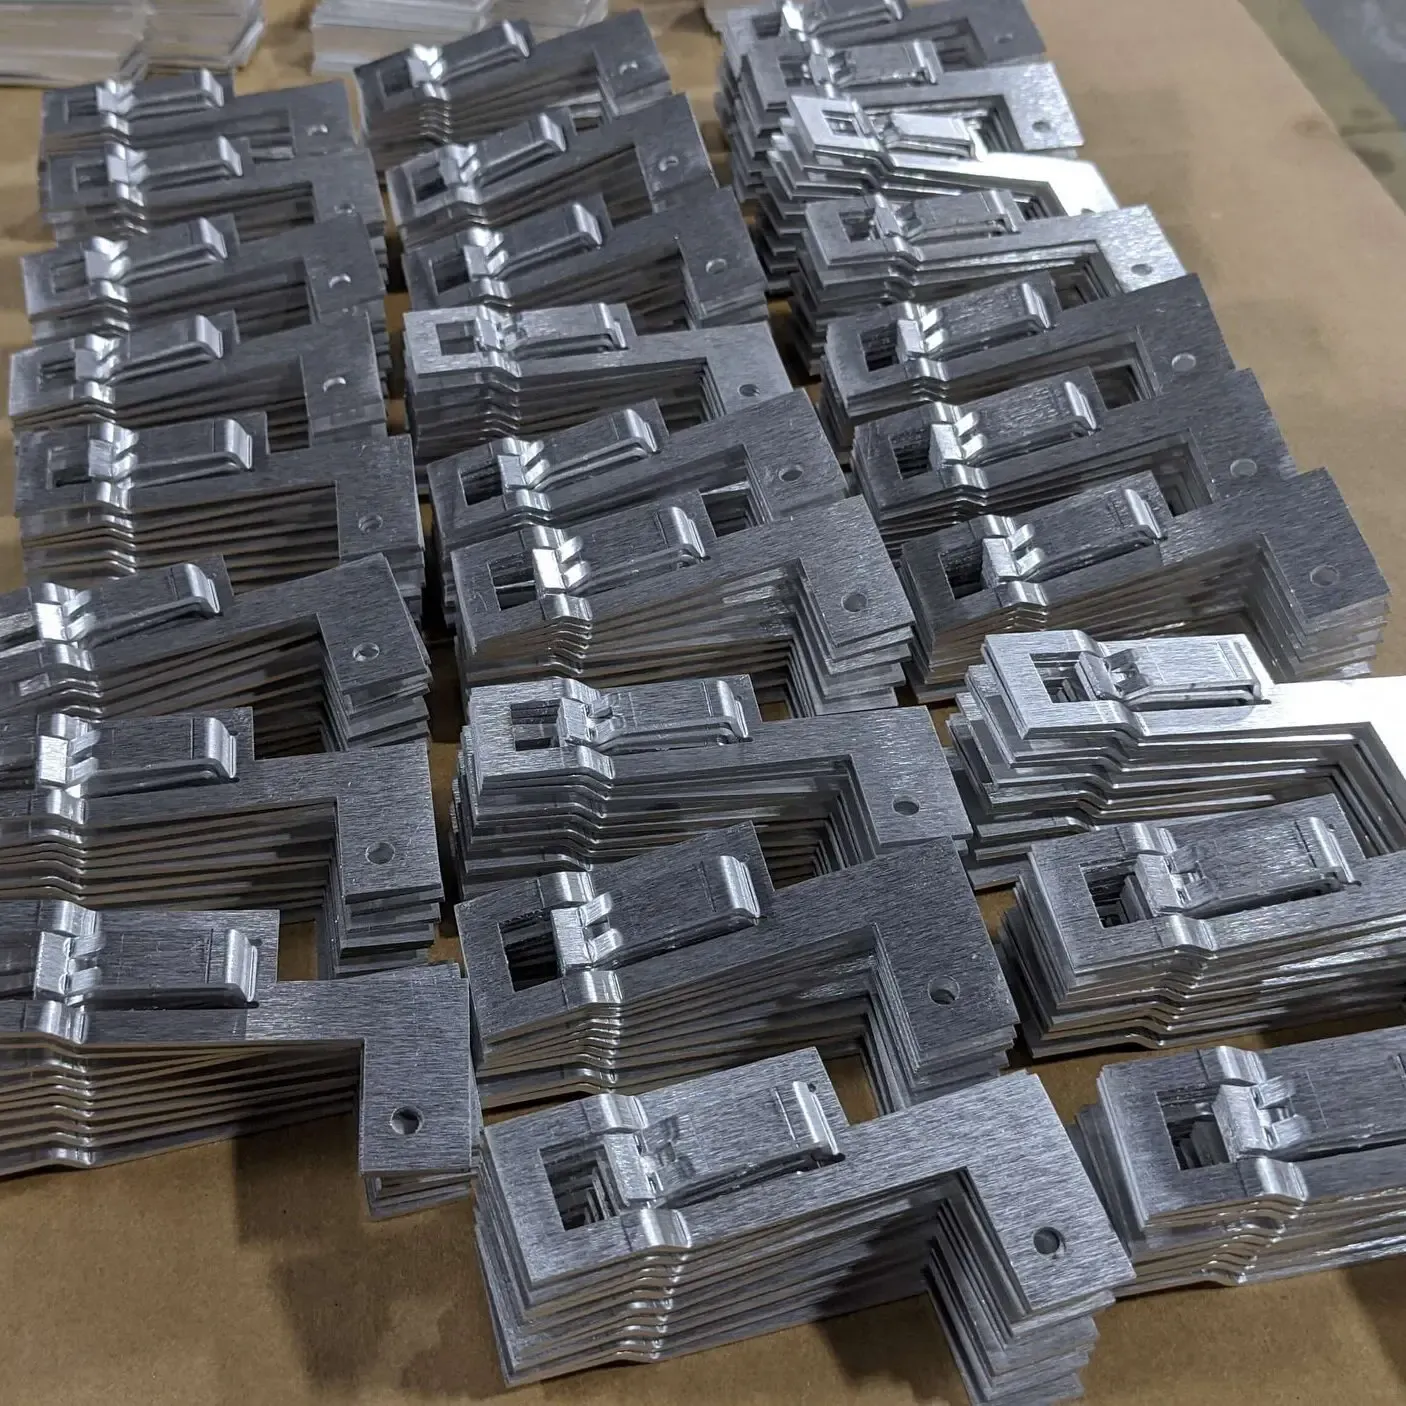
Automech utilizes advanced press systems to manufacture durable Automotive Sheet Metal Parts for the mobility sector
1.2.2 Chassis and structural components
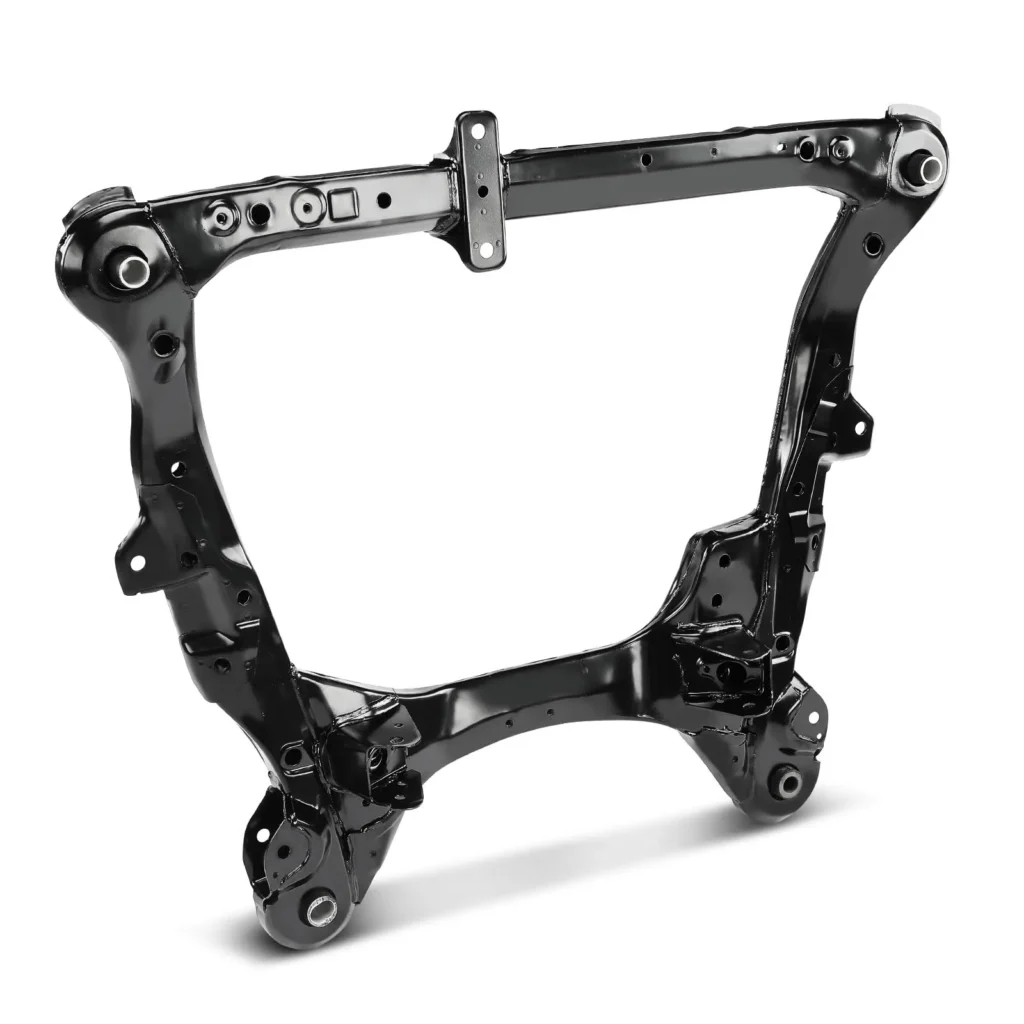
Chassis sheet metal parts carry high dynamic and torsional loads generated by road inputs, steering forces, and drivetrain torque. Heavy-gauge stamped components include subframe crossmembers, control arm reinforcement gussets, trailing arm brackets, and shock absorber tower plates. These components demand thick structural steels that resist cyclic fatigue over the vehicle’s operational lifespan.
1.2.3 Brackets, reinforcements and mounting components
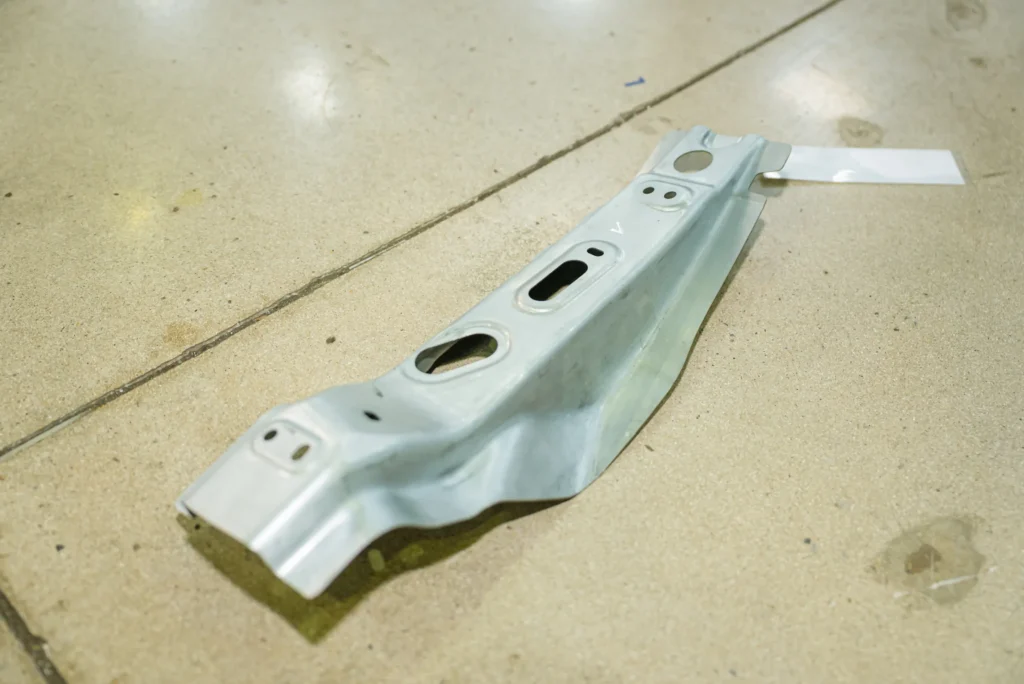
Brackets and reinforcements serve as structural bridges connecting auxiliary vehicle subsystems to the main chassis frame. Stamped brackets securely mount electronic control units (ECUs), cooling radiators, air conditioning compressors, exhaust hangers, wiring harnesses, and battery packs, preventing displacement caused by engine and road vibrations.
1.3 OEM and Tier Supplier Requirements
1.3.1 OEM metal stamping parts
Automotive OEMs mandate strict compliance with proprietary 2D technical drawings, 3D CAD nominal data, and corporate material specifications. Every stamped part must conform to rigorous geometric dimensioning and tolerancing (GD&T) callouts, hole true-position tolerances, and surface finish requirements. Tooling ownership is strictly maintained by the customer, and manufacturing parameters cannot be altered without a formal Engineering Change Notification (ECN).
1.3.2 Tier 1 and Tier 2 automotive component sourcing
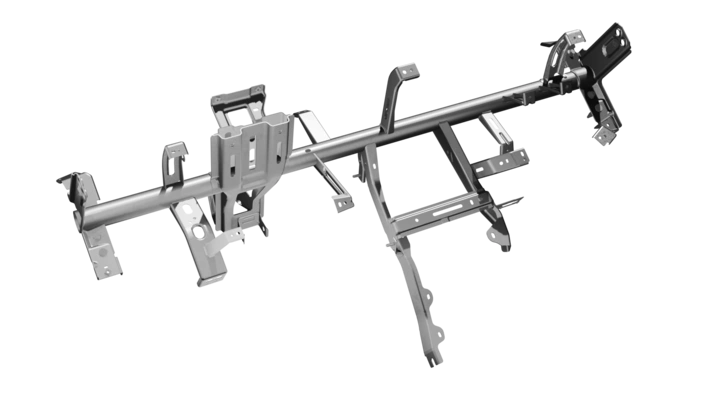
Global vehicle manufacturing operates on a multi-tiered supply chain structure. Tier 1 suppliers assemble complete functional vehicle systems-such as seat adjuster modules, instrument panel structures, and brake booster assemblies-and source stamped brackets, clips, and reinforcement plates from specialized Tier 2 stamping contract manufacturers. Suppliers must meet strict Just-In-Time (JIT) delivery windows, maintain safety buffer stocks, and provide complete batch quality documentation.
1.3.3 Prototype, pilot and mass production requirements
Automotive procurement programs require structured multi-stage validation:
- Prototype Phase: Validates part geometry, mechanical packaging, and physical crash performance using soft-tool dies, 3D laser cutting, or CNC press-brake forming (10 to 500 units).
- Pilot Phase: Tests production stamping dies on the shop floor at planned line speeds to verify automated coil feeding, sensor interlocks, and cycle repeatability (1,000 to 5,000 units).
- Mass Production Phase: Full-rate commercial manufacturing utilizing automated progressive or transfer press lines operating under Statistical Process Control (SPC) across multi-year vehicle platform lifecycles.
2. Automotive Sheet Metal Parts Manufacturing Process
2.1 Engineering and Part Development
2.1.1 Technical drawings, CAD data and material specifications
The development sequence begins with a comprehensive review of customer 3D CAD files (STEP, IGES) and 2D engineering drawings. Tooling engineers analyze linear tolerances, angular callouts, true-position hole grids, and raw material mill standards (ASTM, EN, JIS, or OEM proprietary grades) to establish the manufacturing baseline.
2.1.2 DFM review and manufacturability analysis
Design for Manufacturability (DFM) reviews optimize vehicle component geometries for pressworking. Tool designers identify potential manufacturing issues-such as excessively tight bend radii that cause cracking, holes placed too close to bend lines, or narrow web carrier sections-and propose geometry refinements that simplify die construction and reduce scrap.
2.1.3 Tooling feasibility and production planning
Engineers use finite element forming simulation software to analyze sheet metal flow, thinning limits, wrinkling tendencies, and elastic springback behavior. This digital simulation validates tooling feasibility, determines the optimal station progression, and calculates press tonnage distribution before tool steel is procured.
2.2 Primary Sheet Metal Operations
2.2.1 Blanking and piercing
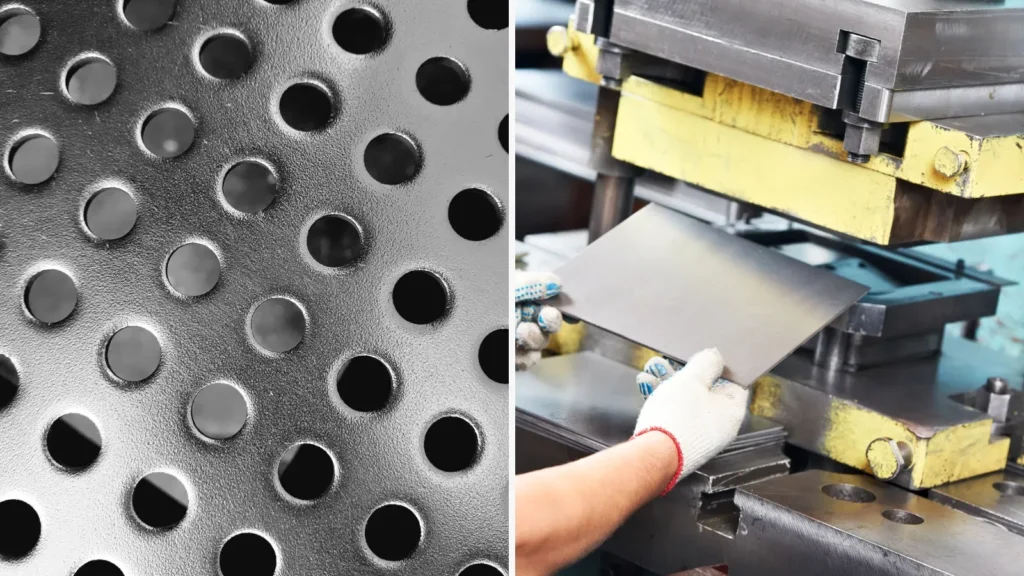
Blanking cuts the outer flat perimeter of the part from coiled sheet stock, while piercing punches internal mounting holes, alignment slots, and clearance openings. Maintaining tight, uniform punch-to-die clearances (typically 5% to 10% of sheet thickness) produces clean shear walls and prevents slug pull-up defects on the die surface.
2.2.2 Bending and forming
Bending plastically deforms flat sheet metal along straight linear axes to create angles, channels, and mounting flanges. Forming deforms metal along curved or compound contours without shearing material fibers, adding embossed stiffeners, offset steps, and multi-axis contours that improve structural rigidity.
2.2.3 Deep drawing and flanging
Deep drawing utilizes a mechanical punch to force flat sheet metal into a hollow die cavity, creating seamless, three-dimensional cup, box, or tray geometries. Flanging turns up the edge of a drawn or stamped profile to create mating surfaces for resistance spot welding or structural adhesive bonding.
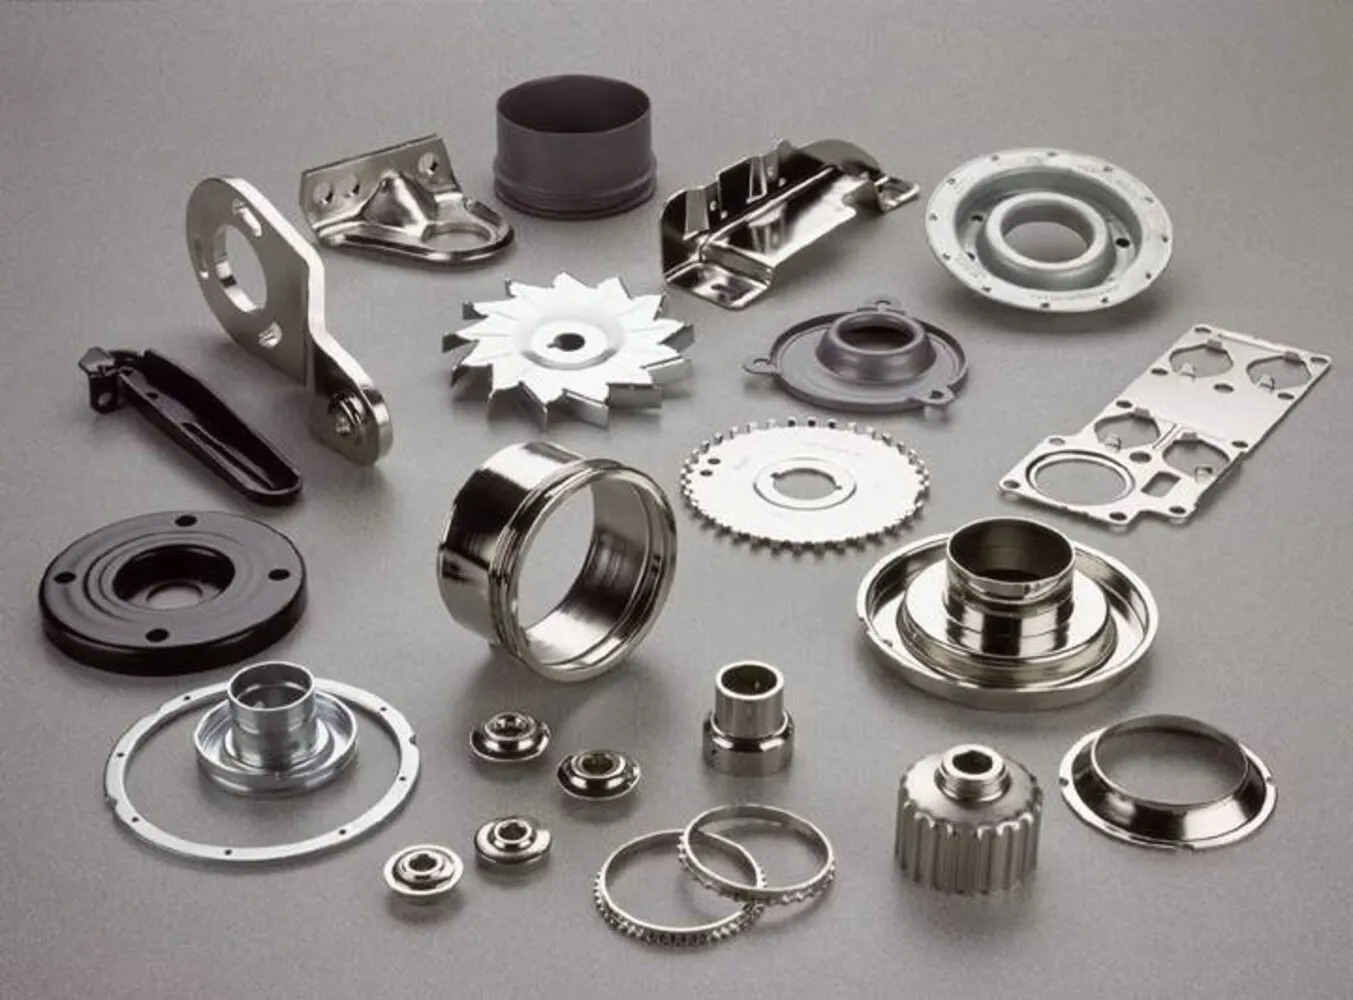
High-precision tooling ensures superior surface finish on all critical Automotive Sheet Metal Parts
2.2.4 Embossing and coining
Embossing presses raised or recessed decorative and structural features-such as part numbers, trace codes, and stiffening ribs-into the metal without altering nominal wall thickness. Coining applies heavy compressive pressure within a closed die to displace metal plastically, producing sharp corner chamfers, countersinks, and thinned datum pads.
2.3 Stamping and Forming Methods
2.3.1 Automotive sheet metal stamping
Automotive sheet metal stamping encompasses single-operation, compound, and modular die configurations mounted in mechanical or hydraulic presses. These setups provide manufacturing flexibility for low-to-medium volume parts, service replacement components, and structural plates requiring specialized secondary operations.
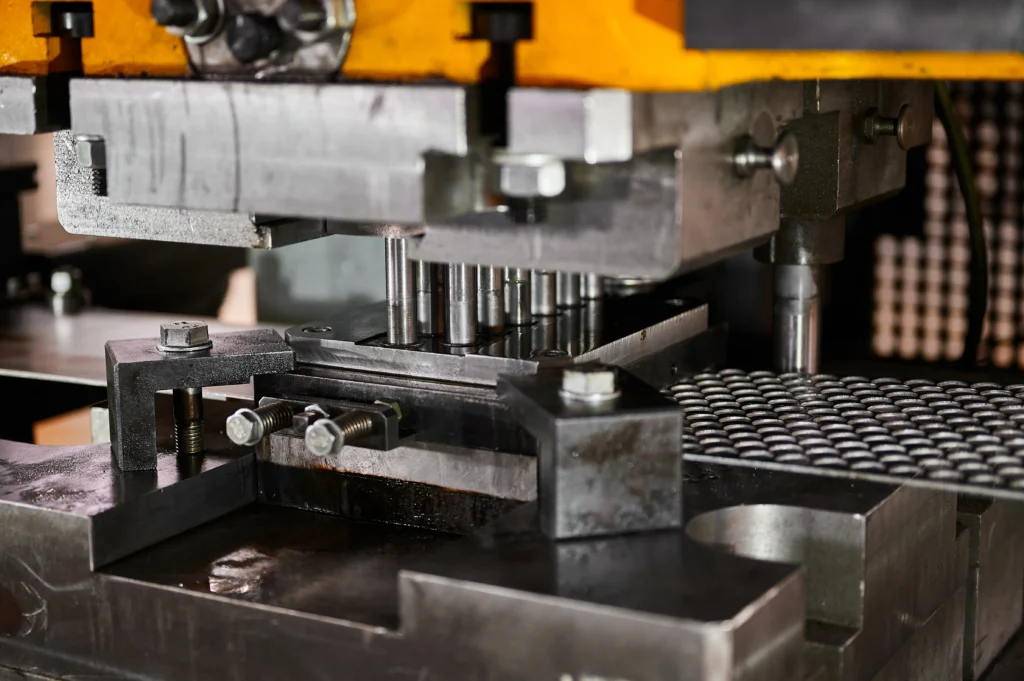
2.3.2 Progressive die stamping
Progressive die stamping feeds continuous coiled sheet metal through sequential inline stations inside a single die block. The workpiece remains attached to a carrier ribbon as it advances through punching, bending, coining, and flanging stations, with the completed part severed at the final cutoff station at speeds between 100 and 500+ strokes per minute.
2.3.3 Transfer stamping
Transfer stamping processes pre-cut discrete sheet metal blanks. Mechanical transfer rails or multi-axis robotic arms physically grip and advance the workpieces across sequential die stations. Transfer stamping is preferred for large automotive structural panels, deep oil pans, and multi-flanged crossmembers that cannot be carried on a continuous coil strip.
2.3.4 High-volume production using stamping dies
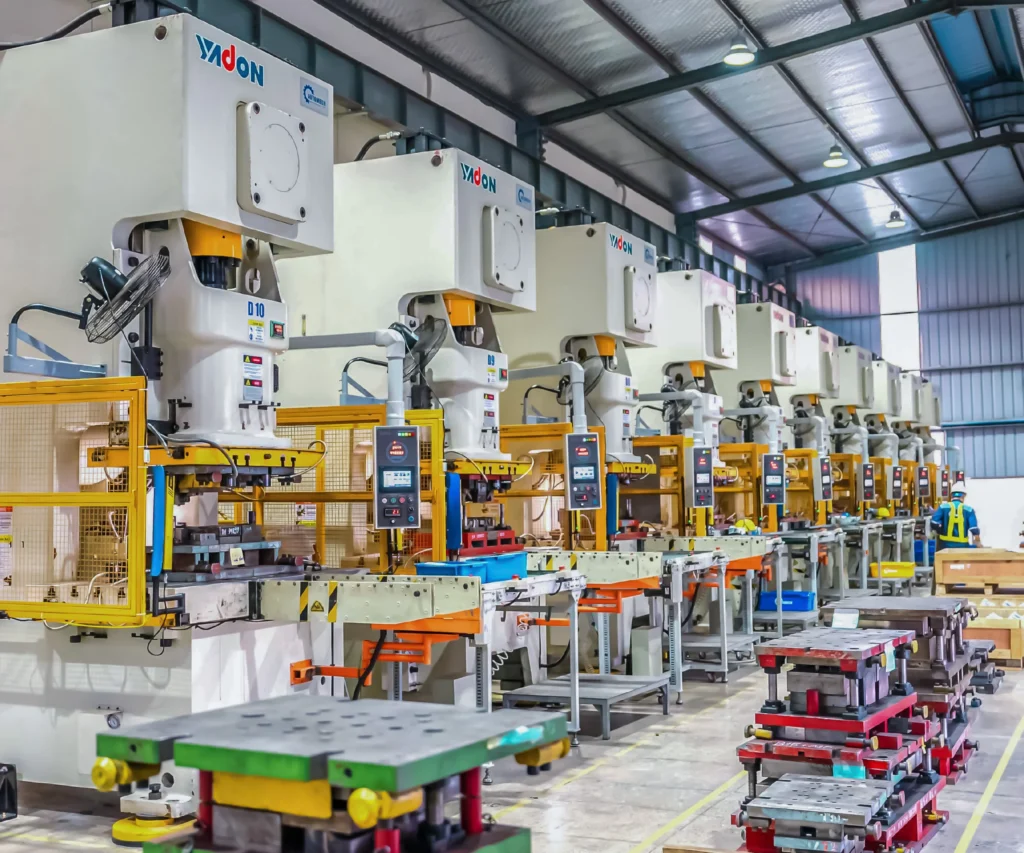
High-volume automotive manufacturing relies on automated stamping press lines running hardened tool steel dies. Automated coil payoff reels, multi-roll levelers, high-speed servo feeders, and robotic destackers ensure continuous press cycling, delivering millions of identical components with minimal manual intervention.
3. Types of Automotive Sheet Metal Parts
3.1 Automotive Body and Structural Parts
3.1.1 Body-in-White sheet metal components
Body-in-White (BIW) stamped stampings make up the unpainted monocoque vehicle structure. Key parts include roof headers, floor pan stampings, A-pillar and B-pillar inner panels, rocker panel reinforcements, and door inner frames. These parts require strict surface flatness and aperture dimensional control to ensure smooth automated robotic framing.
3.1.2 Reinforcement panels and structural members
Reinforcement panels are strategically placed at high-stress structural joints to prevent mechanical deformation during dynamic driving maneuvers or collisions. Stamped from advanced high-strength steels, these components reinforce door hinge pillars, seatbelt upper anchors, suspension strut towers, and bumper crash boxes.
3.1.3 Cross-member related components
Cross-member stampings tie the longitudinal chassis rails together, providing lateral rigidity and resisting torsional vehicle body twisting. Stamped with embossed clearance pockets and flange lips, these structural members support engine mounts, transmission linkages, and exhaust heat shield routings.
3.2 Automotive Brackets and Mounting Parts
3.2.1 Automotive bracket stamping
Automotive bracket stamping covers a wide array of mounting hardware engineered from carbon and structural alloy steels. These brackets feature precision-pierced fastener holes, extruded screw bosses, and locating alignment tabs, providing secure mechanical attachment across the vehicle.
3.2.2 Seat brackets and mounting brackets
Vehicle seating systems rely on stamped sheet metal components, including seat track runner channels, height-adjuster link plates, recliner sector gears, and floor pan anchor brackets. These stampings demand tight tolerances to ensure smooth mechanical movement and passenger safety compliance.
3.2.3 Battery brackets and EV structural brackets
Electric vehicle powertrains require specialized stamped structural brackets to secure high-voltage battery enclosures, power inverters, on-board chargers, and electric drive units. Stamped from high-strength steel or lightweight aluminum, these brackets withstand heavy battery mass under dynamic road shock loads.
3.3 Chassis and Supporting Components
3.3.1 Chassis sheet metal components
Chassis stampings include control arm reinforcement gussets, trailing arm housings, sway bar mounting clamps, and subframe link brackets. Heavy press lines process thick sheet steel (2.5 mm to 6.0 mm) to deliver dynamic fatigue resistance under cyclic vehicle braking and suspension loads.
3.3.2 Exhaust system components
Exhaust system stampings must withstand continuous thermal cycling and corrosive exhaust gases. Stamped components include exhaust pipe hanger brackets, catalytic converter shell halves, muffler end caps, and manifold heat shields manufactured from ferritic and austenitic stainless steels.
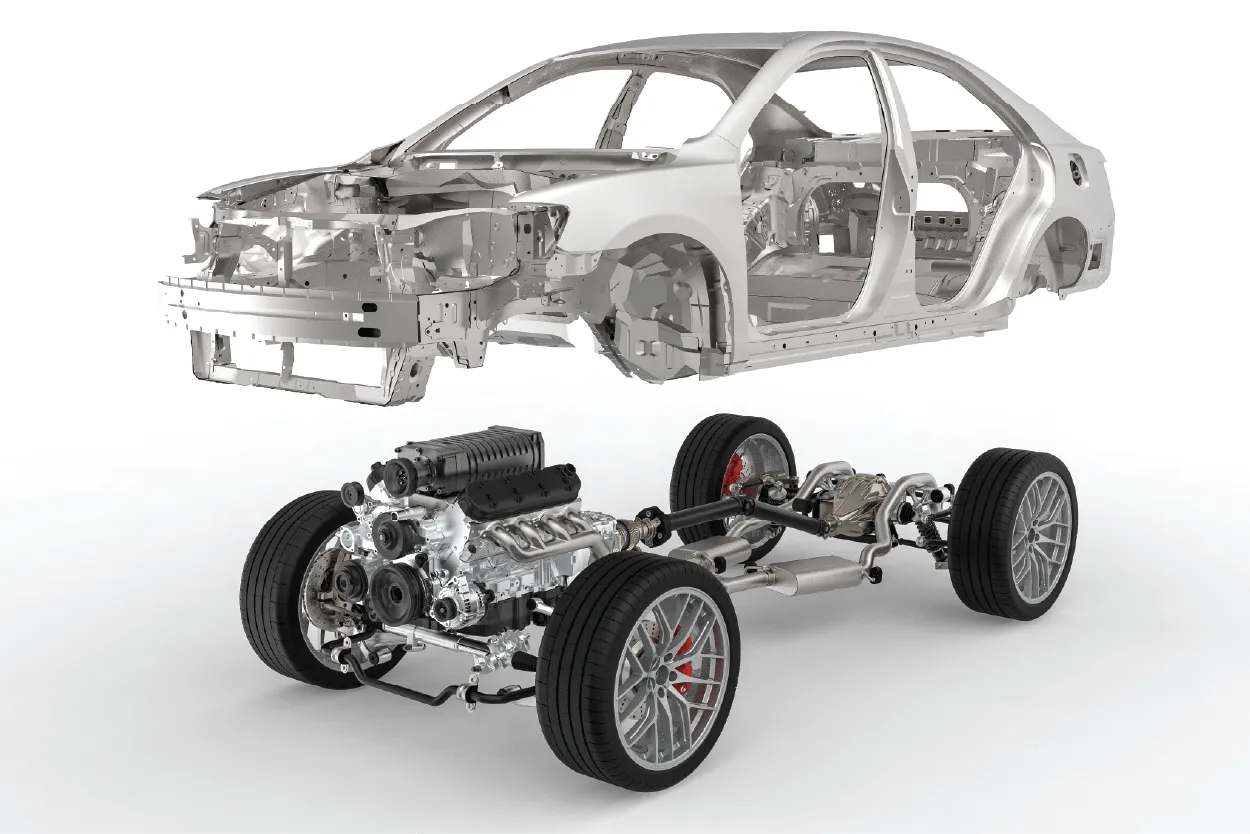
Automech provides customized tooling solutions to optimize production cycles for Automotive Sheet Metal Parts
3.3.3 Heat shields and formed sheet metal parts
Heat shields protect vulnerable components-such as brake fluid lines, fuel tanks, steering racks, and electronic sensors-from intense thermal radiation generated by the exhaust and turbocharger systems. Multi-layer stamped aluminum or aluminized steel shields feature embossed dimple patterns that improve thermal deflection and structural rigidity.
4. Materials, Thickness and Forming Performance
4.1 Materials for Automotive Sheet Metal Parts
4.1.1 Mild steel
Commercial cold-rolled low-carbon steels (SPCC, DC01, ASTM A1008) and deep-drawing quality steels (SPCD, SPCE, DC04) provide excellent formability, ductility, and weldability. They are widely used for multi-bend mounting brackets, interior cabin hardware, and deep-drawn covers.
4.1.2 High-strength steel and AHSS
High-Strength Low-Alloy (HSLA) steels and Advanced High-Strength Steels (AHSS)-including Dual-Phase (DP600, DP800, DP1000), Transformation-Induced Plasticity (TRIP), and Martensitic steels-provide yield strengths up to 1,200+ MPa. These alloys enable structural down-gauging while maximizing crash-energy absorption in passenger safety zones.
4.1.3 Stainless steel and galvanized steel
- Stainless Steel: Austenitic (SUS304, SUS316) and ferritic (SUS409, SUS430) grades provide corrosion and thermal oxidation resistance for exhaust brackets and underbody hardware.
- Galvanized Steel: Hot-dip galvanized (GI, SGCC) and electro-galvanized (EG, SECC) steels incorporate a bonded zinc layer that provides sacrificial galvanic protection against road salt and moisture.
4.1.4 Aluminum sheet metal for applicable automotive components
Structural aluminum alloys (5052-H32, 5182, and 6061-T4/T6) feature a density of ~ 2.70 g/cm³, roughly one-third that of steel. Aluminum stampings are widely utilized in electric vehicles for battery pack enclosures, module tie bars, thermal heat sinks, and exterior closure reinforcements to reduce curb weight.
4.2 Sheet Thickness and Dimensional Requirements
4.2.1 Material thickness selection
Automotive sheet metal parts utilize specific material gauges based on structural function:
- Thin Gauge (0.6 mm to 1.2 mm): Body skin closures, thermal heat shields, and electronic module covers.
- Medium Gauge (1.5 mm to 2.5 mm): Body-in-white reinforcements, seatframe linkages, and mounting brackets.
- Heavy Gauge (3.0 mm to 6.0 mm): Chassis suspension gussets, subframe crossmembers, and towing anchor plates.
4.2.2 Dimensional tolerance and flatness
Precision automotive stampings maintain linear tolerances within ± 0.02 mm to ± 0.05 mm, with hole center-to-center distances held within ± 0.02 mm. Critical mounting surfaces must maintain planar flatness within ± 0.05 mm to prevent stress concentrations when bolted or welded into automated assembly fixtures.
4.2.3 Springback control
Metals with high yield strength (such as AHSS and tempered aluminum) exhibit significant elastic recovery (springback) when forming pressure is released. Tool designers counteract springback by incorporating over-bending cam angles, bottoming relief steps, or localized coining beads into forming cavities to hold drawing angles within ± 0.25°.
4.3 Surface and Edge Quality
4.3.1 Burr control
Exit burr formation is controlled by maintaining precise punch-to-die cutting clearances (typically 5% to 8% of sheet thickness). Automated press lines and sharp tool-steel cutting edges restrict burr heights to under 5% to 10% of material thickness, preventing assembly fitment issues and eliminating safety hazards for line workers.
4.3.2 Surface finish requirements
Automotive components require defect-free surfaces free of die scratches, gouges, or galling marks. Polished die cavities, synthetic stamping lubricants, and Physical Vapor Deposition (PVD) wear coatings ensure clean surface topographies (Ra < 0.4 μm) suitable for E-coating or cosmetic painting.
4.3.3 Deburring and edge treatment
To ensure smooth edge profiles, stamped components undergo vibratory bowl deburring with ceramic media, centrifugal barrel finishing, or automated abrasive belt edge-rounding. Deburring eliminates micro-cracks along sheared edges, preventing fatigue fractures during secondary flanging or high-stress vehicle operation.
5. Precision Automotive Sheet Metal Parts and Tooling
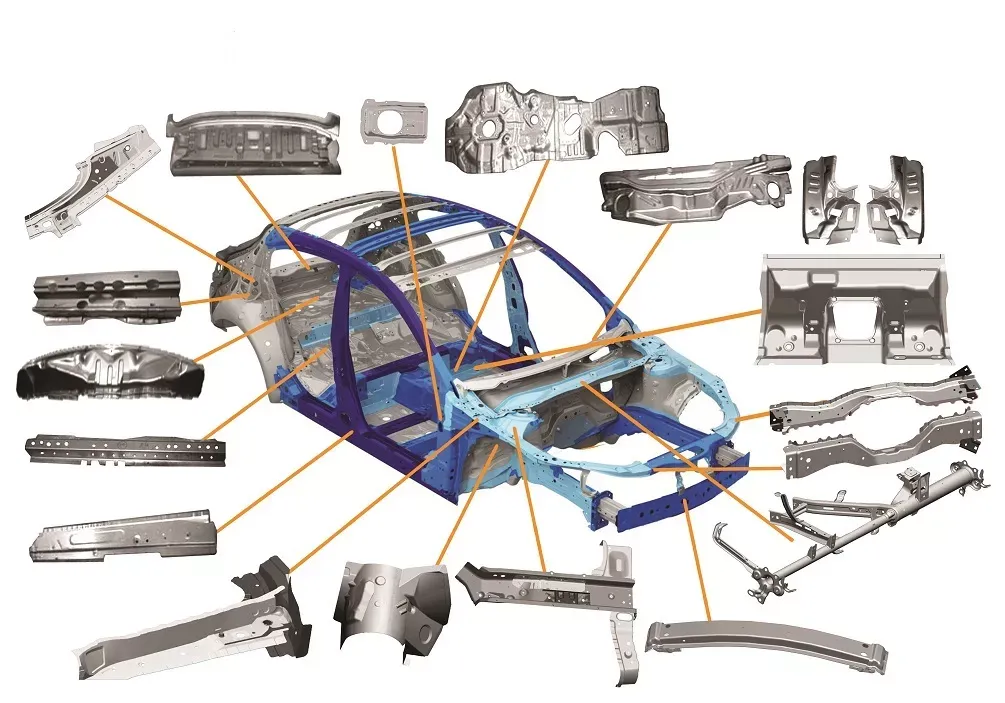
Modern vehicle architectures require lightweight Automotive Sheet Metal Parts to improve overall energy efficiency
5.1 Precision Metal Stamping
5.1.1 High-precision automotive sheet metal components
Precision metal stamping manufactures tight-tolerance automotive parts such as seatbelt latch plates, fuel injection clips, electric drive busbars, and electronic transmission sensor brackets. These components require micron-level accuracy to function properly within sensitive mechanical and electrical vehicle systems.
5.1.2 Tight tolerance and repeatability requirements
Precision stamping routinely achieves linear tolerances between ± 0.005 mm and ± 0.02 mm. Utilizing rigid press beds, guided stripper plates, and precision ball-bearing guide pillars eliminates machine deflection, ensuring that millions of consecutive parts exhibit identical dimensions with minimal process drift.
5.1.3 Precision stamping for OEM production
For OEM manufacturing, precision stamping integrates in-die fiber optic sensors, optical misfeed detectors, and automated thickness checks. These systems monitor part formation in real time, preventing defective components from advancing to customer assembly lines.
5.2 Automotive Stamping Tooling
5.2.1 Stamping die design
Stamping die design determines finished part quality. Engineering teams use 3D CAD/CAM software to model multi-station strip progressions, calculating punch clearances, stripper forces, and pilot pin locations to ensure balanced press loads across the die bed.
5.2.2 Progressive die tooling
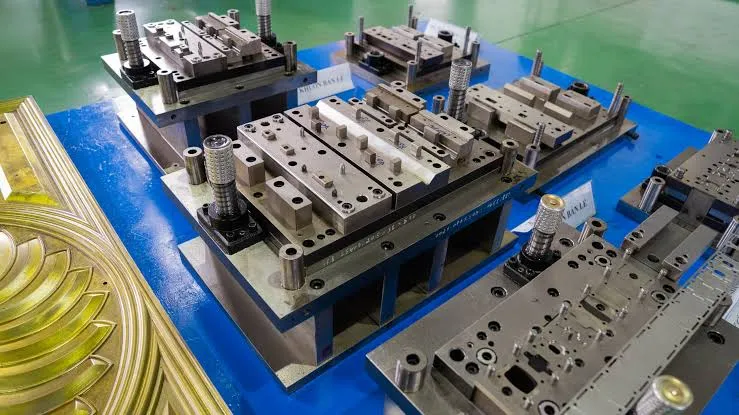
Progressive dies integrate multiple sequential piercing, coining, forming, and shearing stations into a single tool block. Advancing a continuous metal strip through the die produces completed precision components at high speeds (100 to 500+ strokes per minute) with minimal labor intervention.
5.2.3 Tool steel selection and tool life
Tool designers select premium tool steels based on wear resistance and impact toughness. Standard choices include AISI D2, DC53, and SKD11 for die blocks and punches, with tungsten carbide inserts specified for high-wear cutting edges. Applying PVD coatings such as TiAlN extends tool life to several million press strokes.
5.2.4 Die maintenance and production stability
Maintaining stable production requires structured preventive tool maintenance. Technicians inspect guide pillars, clean die cavities, check nitrogen gas springs, and regrind punch cutting edges at scheduled intervals (every 50,000 to 100,000 strokes) to prevent burr growth and punch chipping.
5.3 High Precision Automotive Die Manufacturing
5.3.1 Automotive progressive die supplier requirements
Qualified automotive die suppliers must operate modern toolrooms equipped with high-speed CNC machining centers, precision wire EDM machinery, and optical surface profile grinders. Internal die components must be machined to tolerances within ± 0.005 mm to ensure proper punch-to-die alignment.
5.3.2 Die validation and tryout
Die validation bridges digital design and physical manufacturing. Tryout presses run initial strip developments under operating conditions. Toolmakers examine metal thinning, localized necking, and springback deviations on trial stampings, making fine toolroom adjustments to punches and cavities.
5.3.3 Tooling optimization for high-volume production
Tooling optimization focuses on maximizing material utilization, streamlining station counts, and incorporating quick-change modular inserts. Standardizing wear components across die sets lowers toolmaking costs, simplifies spare parts management, and ensures rapid maintenance turnarounds during mass production.
6. Secondary Operations, Welding and Assembly
6.1 Secondary Operations
6.1.1 Deburring and edge finishing
High-speed die shearing creates micro-burrs along the cut perimeter of stamped automotive components. To prevent handling injuries during manual assembly, eliminate stress-concentration notches that cause fatigue cracks, and avoid chafing adjacent wiring harnesses, parts undergo automated deburring. Methods include vibratory bowl deburring with ceramic media, centrifugal barrel finishing, and automated abrasive belt edge-rounding that produce smooth corner breaks.
6.1.2 Form correction and dimensional adjustment
Components formed from advanced high-strength steels (AHSS) or deep-drawn geometries may retain residual internal stresses that cause slight geometric distortion. Secondary hydraulic restrike presses and automated calibration fixtures perform precision restriking, flattening critical datum surfaces and aligning flange profiles within design tolerances.
6.1.3 Secondary machining where required
When components require tight multi-axis hole clearances, fine-pitch internal threads, or precision spot faces that cannot be formed directly within the press tool, secondary machining is utilized. High-speed CNC tapping centers, multi-spindle drilling heads, and dedicated milling stations produce clean metric or unified threads, countersinks, and planar mating faces without damaging adjacent formed features.
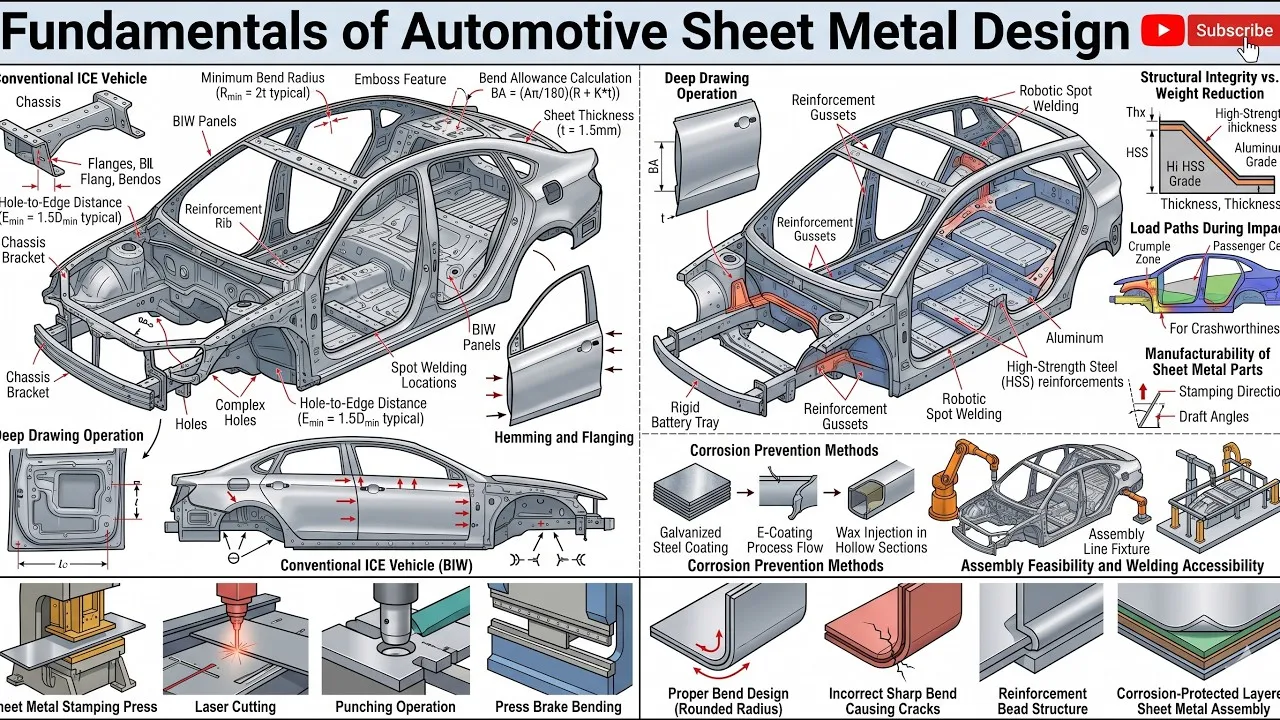
Automech implements automated transfer systems to boost throughput when forming Automotive Sheet Metal Parts
6.2 Automotive Sheet Metal Welding
6.2.1 Spot welding
Resistance spot welding joins overlapping stamped automotive sheet metal parts by passing localized electrical current through copper alloy electrodes under pneumatic or servo clamping pressure. It represents the primary joining method for body-in-white (BIW) reinforcements, mounting brackets, and structural floor assemblies, delivering clean, high-strength joints without adding filler metal weight.
6.2.2 MIG welding
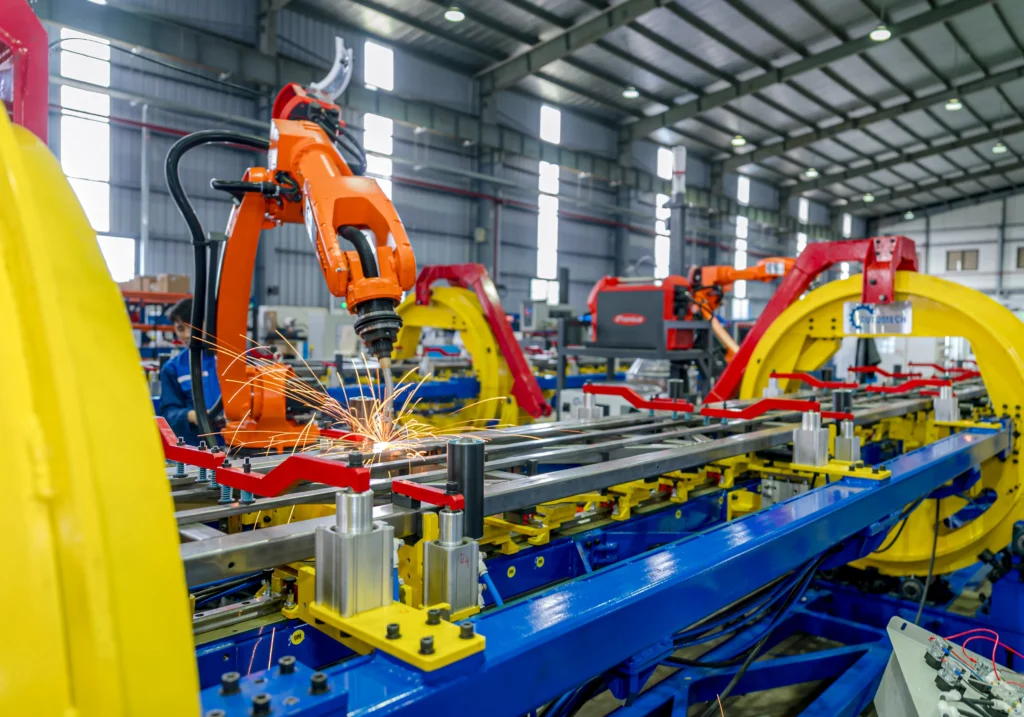
Metal Inert Gas (MIG/GMAW) welding provides continuous, deep-penetration weld seams across heavier structural stampings and chassis assemblies. Used on suspension subframe crossmembers, control arm links, and thick towing brackets, robotic MIG welding cells deliver high fatigue endurance and dynamic load resistance under severe road operating conditions.
6.2.3 Laser welding
Fiber laser welding provides a high-density, low-heat-input joining solution for critical vehicle assemblies. The narrow heat-affected zone (HAZ) minimizes thermal distortion across thin sheet metal assemblies, making laser welding suitable for joining electric vehicle (EV) battery pack enclosures, hermetically sealed fluid manifolds, and tailored blank structural panels.
6.3 Automotive Stamping Assembly
6.3.1 Fixture-controlled assembly
Custom welding and assembly fixtures utilize CNC-machined locating blocks, hardened dowel pins, and pneumatic toggle clamps to hold stamped sub-components in precise spatial alignment. High-rigidity fixture construction counteracts thermal expansion forces generated during high-amperage welding cycles, ensuring final assembly geometry conforms to CAD nominals.
6.3.2 Bracket and reinforcement assembly
Automated assembly cells combine primary structural stampings with secondary components, including threaded clinch studs, self-piercing rivets (SPR), self-clinching PEM nuts, and rubber isolation bushings. Consolidating multiple stamped brackets and hardware items into a single sub-assembly reduces assembly complexity on OEM vehicle framing lines.
6.3.3 Welding and dimensional control after assembly
Completed welded modules undergo dimensional validation using dedicated checking fixtures and Coordinate Measuring Machines (CMM). Quality technicians inspect critical mounting datums, hole true positions, and weld seam penetration to ensure assemblies interface cleanly with mating vehicle systems without mechanical binding.
7. Quality Control and Automotive Manufacturing Standards
7.1 Automotive Sheet Metal Inspection
7.1.1 CMM inspection
Coordinate Measuring Machines (CMM) located in climate-controlled quality laboratories (~ 20 °C) inspect finished production samples. Multi-axis tactile probing and non-contact laser scanning heads verify complex 3D form profiles, true positions, and geometric dimensioning and tolerancing (GD&T) datums directly against customer 3D CAD nominals.
7.1.2 Vision inspection and gauge inspection
Custom attribute checking fixtures, drop indicator gauges, and automated optical vision systems provide fast 100% dimensional verification on active production lines. In-line digital cameras inspect hole presence, slot geometries, and perimeter edge burrs at production press speeds, immediately flagging non-conforming parts.
7.1.3 First Article Inspection (FAI)
Before authorizing mass production runs, quality engineers conduct a comprehensive First Article Inspection (FAI) on initial stamped parts off the tool. FAI reports verify that die shut-height calibration, strip pitch, and punch offsets yield fully conforming components across every drawing dimension before full production release.
7.2 Process Quality Control
7.2.1 In-process SPC
Statistical Process Control (SPC) protocols govern continuous production runs. Press operators sample parts at defined hourly intervals, logging critical dimensions into X-bar and R control charts to maintain process capability indices (Cpk1.67), preventing process drift before parts fall outside tolerance limits.
7.2.2 MSA and measurement system validation
Measurement Systems Analysis (MSA), including Gage Repeatability and Reproducibility (Gage R&R) studies, verifies that inspection tools and operator techniques introduce minimal measurement error. Maintaining Gage R&R values below 10% ensures dependable dimensional verification data.
7.2.3 Traceability and production records
Digital quality management systems maintain complete lot traceability for every production batch. Laser-etched DataMatrix barcodes or stamped batch numbers link finished stampings directly to raw material master coil certifications, tool maintenance history, press machine IDs, and inspection logs for 10 to 15 years.
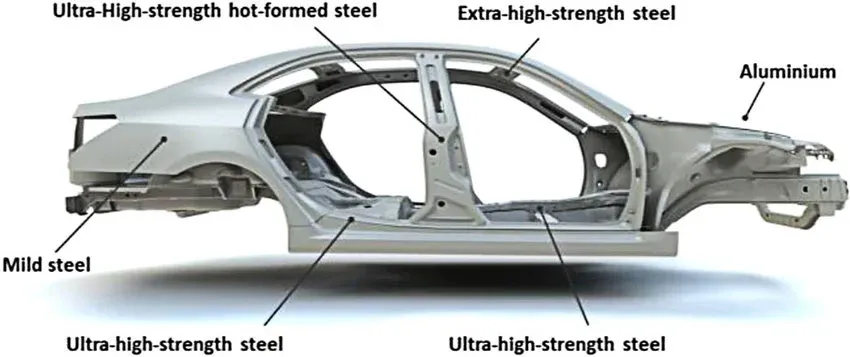
Strict IATF 16949 standards govern the quality control procedures for Automotive Sheet Metal Parts
7.3 Automotive Quality Management
7.3.1 ISO 9001 requirements
ISO 9001 establishes the foundational Quality Management System (QMS), standardizing operating procedures, raw material verification, equipment calibration, and structured continuous improvement (PDCA) routines across all manufacturing operations.
7.3.2 IATF 16949 requirements
IATF 16949 enforces automotive-specific quality management requirements focused on defect prevention, supply chain variation reduction, automated error-proofing (Poka-Yoke), and complete raw material-to-part traceability across the automotive supply chain.
7.3.3 PPAP and APQP
- APQP: Advanced Product Quality Planning aligns cross-functional teams from tool design through production launch, identifying and resolving manufacturing risks early.
- PPAP: The Production Part Approval Process provides customer confidence by submitting Level 3 packages (sample parts, dimensional results, material test reports, and process capability studies) proving the production line consistently meets all engineering requirements at line speeds.
7.3.4 FMEA and Control Plan
- FMEA: Design and Process Failure Mode and Effects Analysis (DFMEA/PFMEA) identify potential failure modes in tooling and press operations, allowing engineers to implement preventive countermeasures before tool steel is cut.
- Control Plan: Defines specific inspection checkpoints, measuring instruments, sample frequencies, and reaction protocols across every stage of production-from incoming coil receiving to packaging.
8. Automotive Sheet Metal Parts: Production Volume and Cost Factors
8.1 Production Models
8.1.1 Prototype production
Prototype production validates component geometry, mechanical fitment, and assembly clearance during early vehicle design. Manufacturers utilize laser cutting, CNC press brake forming, or soft modular tooling to produce functional prototypes (10 to 500 units) for physical crash and fit-up validation.
8.1.2 Pilot production
Pilot production runs evaluate production stamping dies under commercial operating speeds. Stamping a trial lot of several thousand parts validates automated coil feeding stability, in-die sensor interlocks, scrap evacuation, and cycle-time repeatability prior to high-volume manufacturing approval.
8.1.3 Low-volume production
Low-volume manufacturing (typically 500 to 5,000 units) accommodates specialty vehicles, commercial trucks, and niche mobility platforms. Suppliers utilize single-operation modular dies or hybrid tooling setups, balancing initial tooling investment against unit delivery schedules.
8.1.4 Mass production
Mass production represents the steady-state manufacturing phase where automated coil lines, progressive dies, and robotic welding cells produce hundreds of thousands to millions of components annually under continuous Statistical Process Control (SPC).
8.2 Key Automotive Sheet Metal Parts Pricing Factors
8.2.1 Material grade and sheet thickness
Raw material selection establishes baseline component costs. Advanced High-Strength Steels (AHSS), austenitic stainless steel (SUS304), and structural aluminum alloys command higher raw material premiums than commercial-grade cold-rolled steel (SPCC). Sheet thickness dictates press tonnage requirements and raw metal weight per thousand parts.
8.2.2 Part geometry and forming complexity
Component geometry directly dictates tooling configurations and press operational speeds. Intricate profiles featuring deep draw recesses, compound flange bends, dense piercing matrices, or embossed stiffeners require multi-station progressive or transfer dies, increasing initial tool engineering investments.
8.2.3 Tooling and die investment
Stamping die fabrication represents a significant upfront capital expenditure. Multi-station progressive dies utilizing vacuum-hardened tool steels (DC53, SKD11) or tungsten carbide inserts require higher upfront capital, but eliminate manual handling and lower piece-part rates over the lifecycle of the vehicle platform.
8.2.4 Production volume and cycle time
High-volume automotive programs amortize non-recurring engineering (NRE) setup and tooling investments across the production run, driving unit costs down to fractions of a dollar. Press cycle speeds (100 to 300+ strokes per minute) maximize machine output, significantly lowering press processing overhead per part.
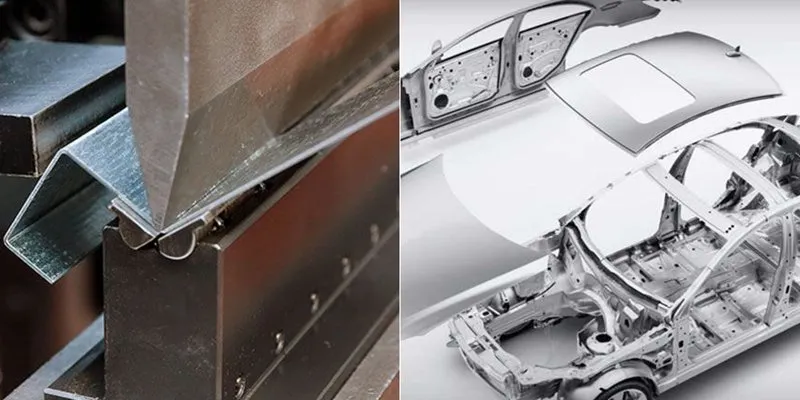
Engineers at Automech perform FEA simulations before stamping complex Automotive Sheet Metal Parts
8.2.5 Secondary operations and assembly requirements
Post-stamping processing steps-such as vibratory deburring, barrel washing, robotic spot welding, hardware fastener insertion, and E-coating-add processing stages to the workflow. Consolidating secondary processes inside automated production cells controls total finished unit costs.
8.3 Stamping vs CNC Machining
8.3.1 Automotive sheet metal stamping vs CNC machining
Automotive sheet metal stamping cold-forms flat metal coils into complex structural parts in fractions of a second using matched dies. CNC machining is a subtractive cutting process that removes metal layer by layer from solid blocks, requiring minutes or hours per component.
8.3.2 Cost and production-volume considerations
CNC machining requires minimal upfront tooling, making it economical for prototypes and runs under 1,000 units. Stamping requires significant upfront die investment, but delivers unmatched cost efficiency for volumes exceeding 10,000 to 50,000+ units due to high production speeds and minimal labor overhead.
8.3.3 Tolerance, geometry and application suitability
CNC machining accommodates thick prismatic blocks, internal bores, and variable wall thicknesses with tolerances down to ± 0.002 mm. Stamping is ideal for uniform-thickness sheet metal components (0.6 mm to 6.0 mm) requiring high strength-to-weight ratios, structural flanges, and rapid batch repeatability.
9. How to Select an Automotive Sheet Metal Parts Supplier
9.1 Technical Supplier Evaluation
9.1.1 Automotive metal stamping capability
Verify that the supplier operates a comprehensive press fleet covering mechanical, hydraulic, and servo presses with capacities ranging from 100 tons to over 1,300 tons, capable of handling thin precision skins up to heavy structural chassis plates.
9.1.2 Precision metal stamping capability
Ensure the manufacturer can achieve tight dimensional tolerances (down to ± 0.01 mm to ± 0.02 mm) across critical mounting holes, datum profiles, and functional latch interfaces with minimal exit burrs.
9.1.3 Progressive die stamping capability
Confirm the supplier operates high-speed automated progressive press lines equipped with motorized decoilers, precision straighteners, and servo roll feeders to support high-volume OEM release schedules.
9.1.4 Tooling and die manufacturing capability
Prioritize suppliers with in-house toolrooms equipped with high-precision wire EDM, CNC milling centers, and optical profile grinders. In-house toolmaking ensures direct control over die precision, fast engineering revisions, and rapid die maintenance.
9.2 Quality and Production Evaluation
9.2.1 ISO 9001 and IATF 16949
Ensure the supplier maintains active ISO 9001 and IATF 16949 certifications, proving the facility enforces structured quality management, automated error-proofing (Poka-Yoke), and continuous defect prevention.
9.2.2 PPAP, APQP, FMEA and Control Plan
Verify that the supplier’s quality engineering team routinely prepares and submits complete Level 3 PPAP packages, supported by rigorous APQP project management, Process FMEA risk assessments, and production Control Plans.
9.2.3 Inspection equipment and traceability
Ensure the facility operates a climate-controlled quality laboratory (~ 20 °C) equipped with Coordinate Measuring Machines (CMM), optical vision profile projectors, and surface roughness testers, backed by digital batch traceability systems.
9.2.4 Prototype-to-mass-production capability
Choose a partner capable of supporting the complete vehicle development lifecycle-from soft-tool prototype stamping and pilot validation to automated high-volume mass production.
9.3 Supply Chain and Export Evaluation
9.3.1 Automotive export stamping manufacturer
Prioritize contract manufacturers with a proven history of exporting precision stampings to North America and Europe, demonstrating compliance with international trade protocols and protective export packaging standards (VCI).
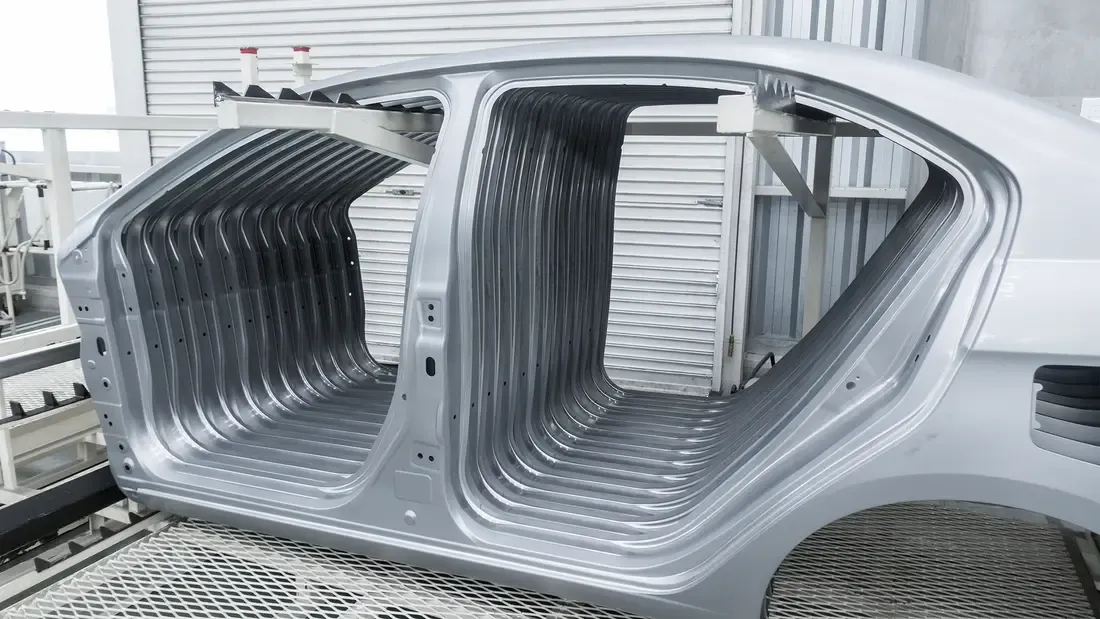
Vehicle crash structures integrate high-strength Automotive Sheet Metal Parts to maximize occupant safety
9.3.2 Production capacity and delivery reliability
Evaluate press utilization rates, facility footprint, and multi-shift operating capacity to ensure the supplier can absorb volume surges and maintain Just-In-Time (JIT) delivery reliability.
9.3.3 Automotive stamping supply chain diversification
Global automotive buyers require resilient supply chain frameworks. Partnering with qualified Southeast Asian contract manufacturers builds supply redundancy and mitigates single-region dependency.
9.3.4 Vietnam as a China+1 sourcing option
Vietnam provides an established manufacturing destination under corporate “China+1” sourcing strategies, offering competitive operational costs, stable political governance, modern deep-water port access, and growing automotive supplier integration.
10. Automotive Sheet Metal Parts RFQ and OEM Sourcing
10.1 Automotive Sheet Metal Parts RFQ Requirements
10.1.1 Technical drawings and CAD files
A complete RFQ package requires clean 3D CAD models (STEP, IGES) alongside 2D PDF technical drawings indicating critical tolerances, linear dimensions, thread callouts, and geometric dimensioning and tolerancing (GD&T) datums.
10.1.2 Material specifications and annual volume
Explicitly define raw material specifications (such as ASTM, EN, or JIS alloy designations), temper/hardness conditions, and sheet gauge thickness. Disclose projected annual usage (EAU) alongside expected order batch sizes and prototype requirements.
10.1.3 Tolerances, surface requirements and inspection standards
Distinguish critical functional mating dimensions from non-critical exterior features. Clearly state required secondary finishing processes (deburring, zinc plating, E-coating) and quality inspection deliverables (such as Level 3 PPAP).
10.1.4 Tooling and packaging requirements
Outline customer-specific tooling guidelines (die component standardization, nitrogen spring preferences) and packaging needs (VCI anti-rust wrapping, returnable plastic dunnage trays).
10.2 Automotive Stamping OEM Sourcing Process
10.2.1 Supplier technical feasibility review
Upon receiving an RFQ, engineering teams evaluate the design using finite element forming simulation software to analyze material stretch limits, draw depths, internal corner radii, and springback behavior.
10.2.2 DFM and tooling feasibility review
Tool designers review the CAD models, evaluating bend radii, hole clearances, and blank profiles to identify cost-reduction opportunities and verify whether progressive, transfer, or compound tooling is optimal.
10.2.3 Prototype and sample validation
The supplier builds prototype tooling or trial production dies, running sample stampings to conduct First Article Inspection (FAI) and verify dimensional alignment against engineering drawings.
10.2.4 PPAP and production approval
The supplier submits sample parts alongside full Level 3 PPAP documentation for customer approval. Once the customer validates the samples and signs the Part Submission Warrant (PSW), the tooling is formally approved for automated mass production.
10.3 RFQ Automotive Stamping Supplier Evaluation
10.3.1 Tooling quotation
Evaluate the transparency of the tooling quotation, verifying tool steel selections, estimated die life, station progression counts, and clear non-recurring engineering (NRE) cost allocations.
10.3.2 Part pricing and production capacity
Compare piece-part unit rates across volume tiers, verifying that the supplier has allocated sufficient press machine hours and tonnage capacity to fulfill forecasted vehicle build rates.
10.3.3 Quality and delivery capability
Confirm the supplier’s track record of quality performance (measured in PPM defect rates) and on-time delivery metrics across past OEM manufacturing contracts.
Automech delivers turnkey manufacturing lines dedicated to fabricating high-volume Automotive Sheet Metal Parts
10.3.4 Export and supply-chain requirements
Verify the supplier’s export experience, international trade documentation handling, customs compliance, and protective packaging methods for international transit.
11. Automotive Sheet Metal Parts Manufacturing in Vietnam – Automech
11.1 Why Source Automotive Sheet Metal Parts from Vietnam?
11.1.1 Automotive manufacturing supply chain diversification
Vietnam’s industrial manufacturing sector has developed a comprehensive supporting ecosystem for metalworking, precision toolmaking, and metal finishing. Global OEMs leverage Vietnam’s modern pressworking infrastructure to build supply chain resilience.
11.1.2 China+1 sourcing strategy
Vietnam serves as a primary hub for corporate China+1 supply chain diversification. International automotive buyers mitigate tariff exposures, reduce geopolitical risks, and secure dependable secondary production capacity without compromising manufacturing quality.
11.1.3 Export manufacturing for US and European buyers
Vietnam benefits from extensive Free Trade Agreements and modern deep-water ocean ports (such as Lach Huyen and Cai Mep) offering direct container routes to North America and Western Europe, ensuring predictable transit timelines.
11.2 Automech Automotive Sheet Metal Manufacturing Capabilities
11.2.1 Automotive metal stamping and precision metal stamping
Established in 2020, Automech (Automech Mechanical Equipment and Solutions Joint Stock Company) provides comprehensive automotive metal stamping services. Operating modern mechanical, hydraulic, and servo press machinery, Automech processes flat sheets and coils into high-precision structural and functional components with tight dimensional tolerances.
11.2.2 Progressive die stamping and tooling support
Automech designs, builds, and operates automated progressive die stamping systems. Equipped with automated decoilers, levelers, and servo roll feeders, the company’s progressive press lines deliver high-speed, continuous manufacturing for automotive brackets, reinforcements, and safety components.
11.2.3 Automotive bracket manufacturing and OEM components
Automech manufactures motor mounts, suspension brackets, sensor holders, chassis gussets, and custom OEM stampings tailored strictly to customer engineering drawings across mass production batches.
11.2.4 Sheet metal forming, welding and assembly
Automech integrates press stamping directly with secondary joining processes. Production assets include automated 800-ton to 1,300-ton tandem stamping press lines with ABB industrial robots, alongside robotic welding cells equipped with KUKA articulated robots and Fronius welding systems.
11.2.5 Prototype-to-mass-production support
Automech supports every stage of the automotive product lifecycle. Factory 1 in Bac Ninh (10,500 m²) focuses on custom tooling, jigs, and prototype trial production, while Factory 2 in Bac Ninh (10,000 m², inaugurated June 2026) is dedicated to high-volume automotive parts manufacturing with an 80% target automation rate.
11.3 Engineering, Quality and Export Support
11.3.1 Engineering and DFM support
Automech’s technical engineering team conducts upfront Design for Manufacturability (DFM) reviews to identify opportunities for material optimization, bend radius standardization, and die complexity reduction before tool steel is cut.
11.3.2 Quality inspection and dimensional validation
Operating climate-controlled quality laboratories (~ 20 °C) equipped with Coordinate Measuring Machines (CMM) and optical profile projectors, Automech validates complex GD&T parameters directly against customer CAD models.
11.3.3 US/EU export manufacturing support
Automech prepares export orders with protective Vapor Corrosion Inhibitor (VCI) packaging, custom palletizing, clear labeling, and comprehensive customs export documentation for global delivery.
11.3.4 ISO 9001 / IATF 16949 compliance where applicable
Automech operates under certified quality management systems aligned with ISO 9001 and automotive IATF 16949 requirements, delivering full Level 3 PPAP packages, process capability studies (Cpk1.67), and complete batch traceability. Major industrial clients include VinFast, VinES, Hoa Phat, Kim Long Motors, and Seojin.
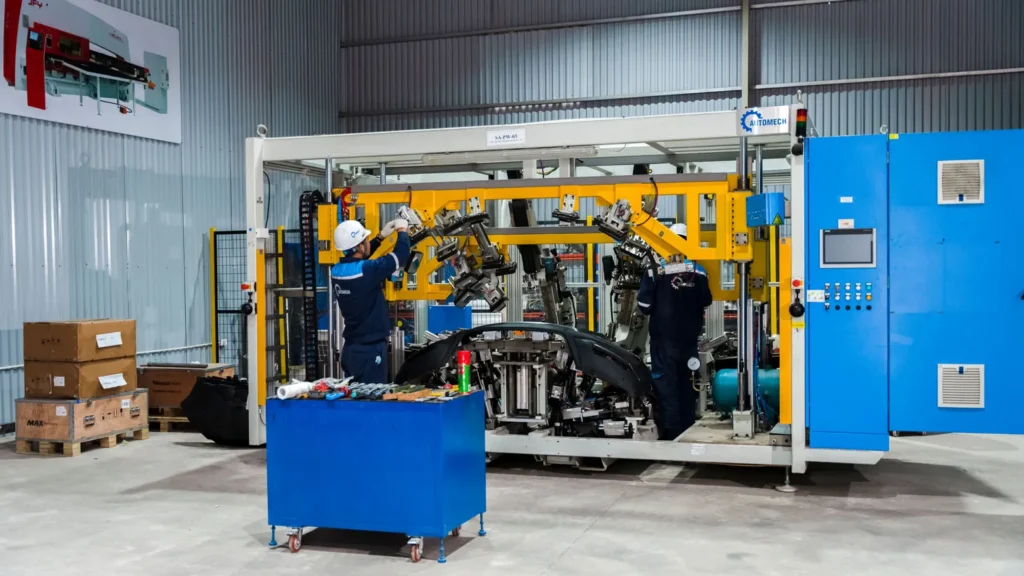
Progressive stamping dies enable fast and cost-effective mass production of Automotive Sheet Metal Parts
11.4 Request an Automotive Sheet Metal Parts RFQ
11.4.1 Upload technical drawings or CAD files
Submit your 3D CAD files (STEP, IGES) and 2D engineering drawings (PDF) detailing critical tolerances, GD&T callouts, and material specifications through Automech’s online portal.
11.4.2 Request DFM and tooling feasibility review
Obtain an upfront tooling feasibility assessment and DFM review analyzing metal stretch limits, springback behavior, and press tonnage distribution.
11.4.3 Request sample parts and production feasibility analysis
Request prototype sample stampings and a comprehensive production cost analysis evaluating coil nesting layouts and progressive die economics.
11.4.4 Get automotive sheet metal parts quotation
Contact Automech today to receive a competitive, volume-tiered quotation for prototype development, pre-series runs, or mass-production automotive sheet metal stamping projects in Vietnam.
12. Automotive Sheet Metal Parts FAQ
12.1 Automotive Sheet Metal Parts Basics
12.1.1 What are automotive sheet metal parts?
Automotive sheet metal parts are custom-formed components produced from flat sheet metal coils or blanks (typically 0.6 mm to 6.0 mm thick) through cold-forming operations such as stamping, shearing, bending, and deep drawing. They form the structural body, chassis frames, and mounting brackets of modern vehicles.
12.1.2 What automotive parts are made from sheet metal?
Common sheet metal parts include body-in-white (BIW) panels, B-pillar reinforcements, floor pan crossmembers, bumper crash boxes, engine mounting brackets, chassis suspension links, EV battery tray enclosures, seat adjuster frames, and exhaust heat shields.
12.1.3 What materials are used for automotive sheet metal parts?
Materials include cold-rolled low-carbon steel (SPCC), deep-drawing steel (SPCE), high-strength low-alloy (HSLA) steel, advanced high-strength steel (AHSS, Dual-Phase), stainless steel (SUS304, SUS409), structural aluminum alloys (5052, 6061-T4/T6), and electro- or hot-dip galvanized steel.
12.2 Manufacturing and Quality
12.2.1 How are automotive sheet metal parts manufactured?
Sheet metal parts are manufactured by uncoiling raw metal strip, leveling it, and feeding it into mechanical, hydraulic, or servo press lines equipped with custom stamping dies. Punches and cavities execute blanking, piercing, bending, and forming operations, followed by automated deburring, robotic welding, and protective surface finishing.
12.2.2 What is automotive sheet metal stamping?
Automotive sheet metal stamping is the high-speed cold-forming pressworking process that uses matched male punches and female die cavities to shape sheet metal into precise three-dimensional vehicle components in fractions of a second.
12.2.3 How accurate are automotive sheet metal parts?
Precision automotive stampings achieve linear and hole tolerances between ± 0.01 mm and ± 0.05 mm, with hole center-to-center distances held within ± 0.02 mm. General structural stampings hold tolerances of ± 0.10 mm to ± 0.20 mm.
12.3 Supplier and Sourcing
12.3.1 How do I choose an automotive sheet metal parts supplier?
Select a supplier based on press tonnage capacity (100T to 1,300T+), in-house wire EDM toolroom assets, active IATF 16949 and ISO 9001 certifications, climate-controlled CMM inspection labs, upfront DFM engineering support, robotic welding integration, and proven export experience.
12.3.2 How do I request an automotive sheet metal parts RFQ?
Submit your 3D CAD files (STEP/IGES) and 2D engineering drawings (PDF) detailing critical dimensions, tolerances, and GD&T datums. Specify raw material alloy grades, sheet thickness, required surface finishes, annual production volume forecasts, and quality documentation requirements (such as Level 3 PPAP).
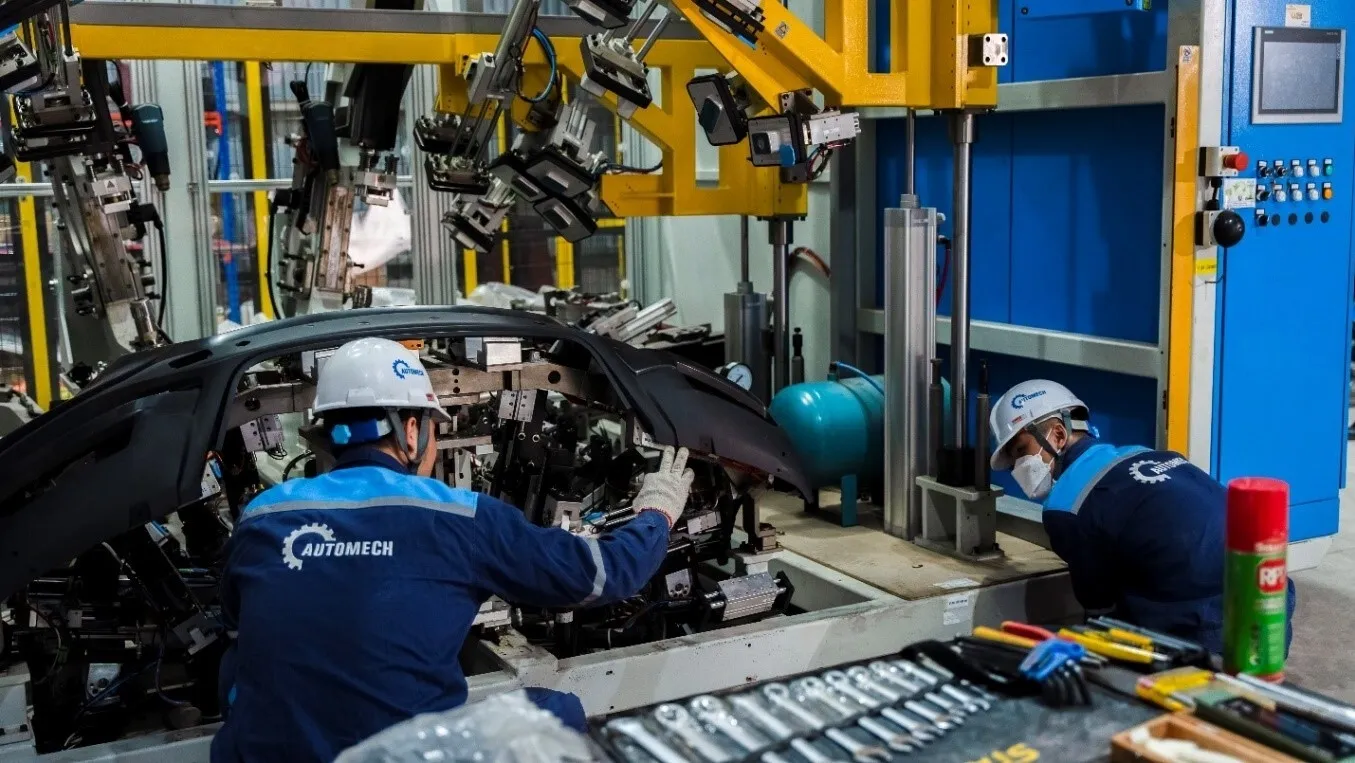
Automech maintains tight dimensional tolerances when machining dies for Automotive Sheet Metal Parts
12.3.3 Why source automotive sheet metal parts from Vietnam?
Vietnam offers competitive production costs, an expanding network of modern high-tonnage press facilities, skilled toolmaking talent, and direct maritime container routes to Western markets. It serves as a dependable “China+1” supply chain diversification hub for international automotive buyers.
12.3.4 What information should be included in an automotive stamping RFQ?
An RFQ must include fully dimensioned 2D drawings, 3D CAD models, material specifications, gauge thickness, annual volume forecasts (EAU), critical GD&T datums, secondary welding or assembly requirements, surface coating callouts, target delivery schedules, and required PPAP submission levels.
Automech Mechanical Equipment and Solutions Joint Stock Company
Head Office: No. 285 Phuc Loi Street, Phuc Loi Ward, Hanoi City
Da Nang Branch: No. 20 Nguyen Sinh Sac Street, Hoa Khanh Ward, Da Nang City
Ho Chi Minh Branch: No. 84, Street No. 10, Van Phuc Urban Area, Hiep Binh Ward, Ho Chi Minh City
Factory No. 1: Automech Automation Equipment, Mold & Tool Manufacturing Factory – Automech Demo Center: Dinh Tram Industrial Park, Nenh Ward, Bac Ninh City, Vietnam
Factory No. 2: Automech Parts Manufacturing & Component Fabrication Factory: Viet Nhat Industrial Cluster, Xuan Cam Commune, Bac Ninh City, Vietnam
Hotline: 0987 899 347
Website: https://automechmfg.com/
Fanpage: https://www.facebook.com/automech.mfg/
YouTube: https://www.youtube.com/@Automechmfg