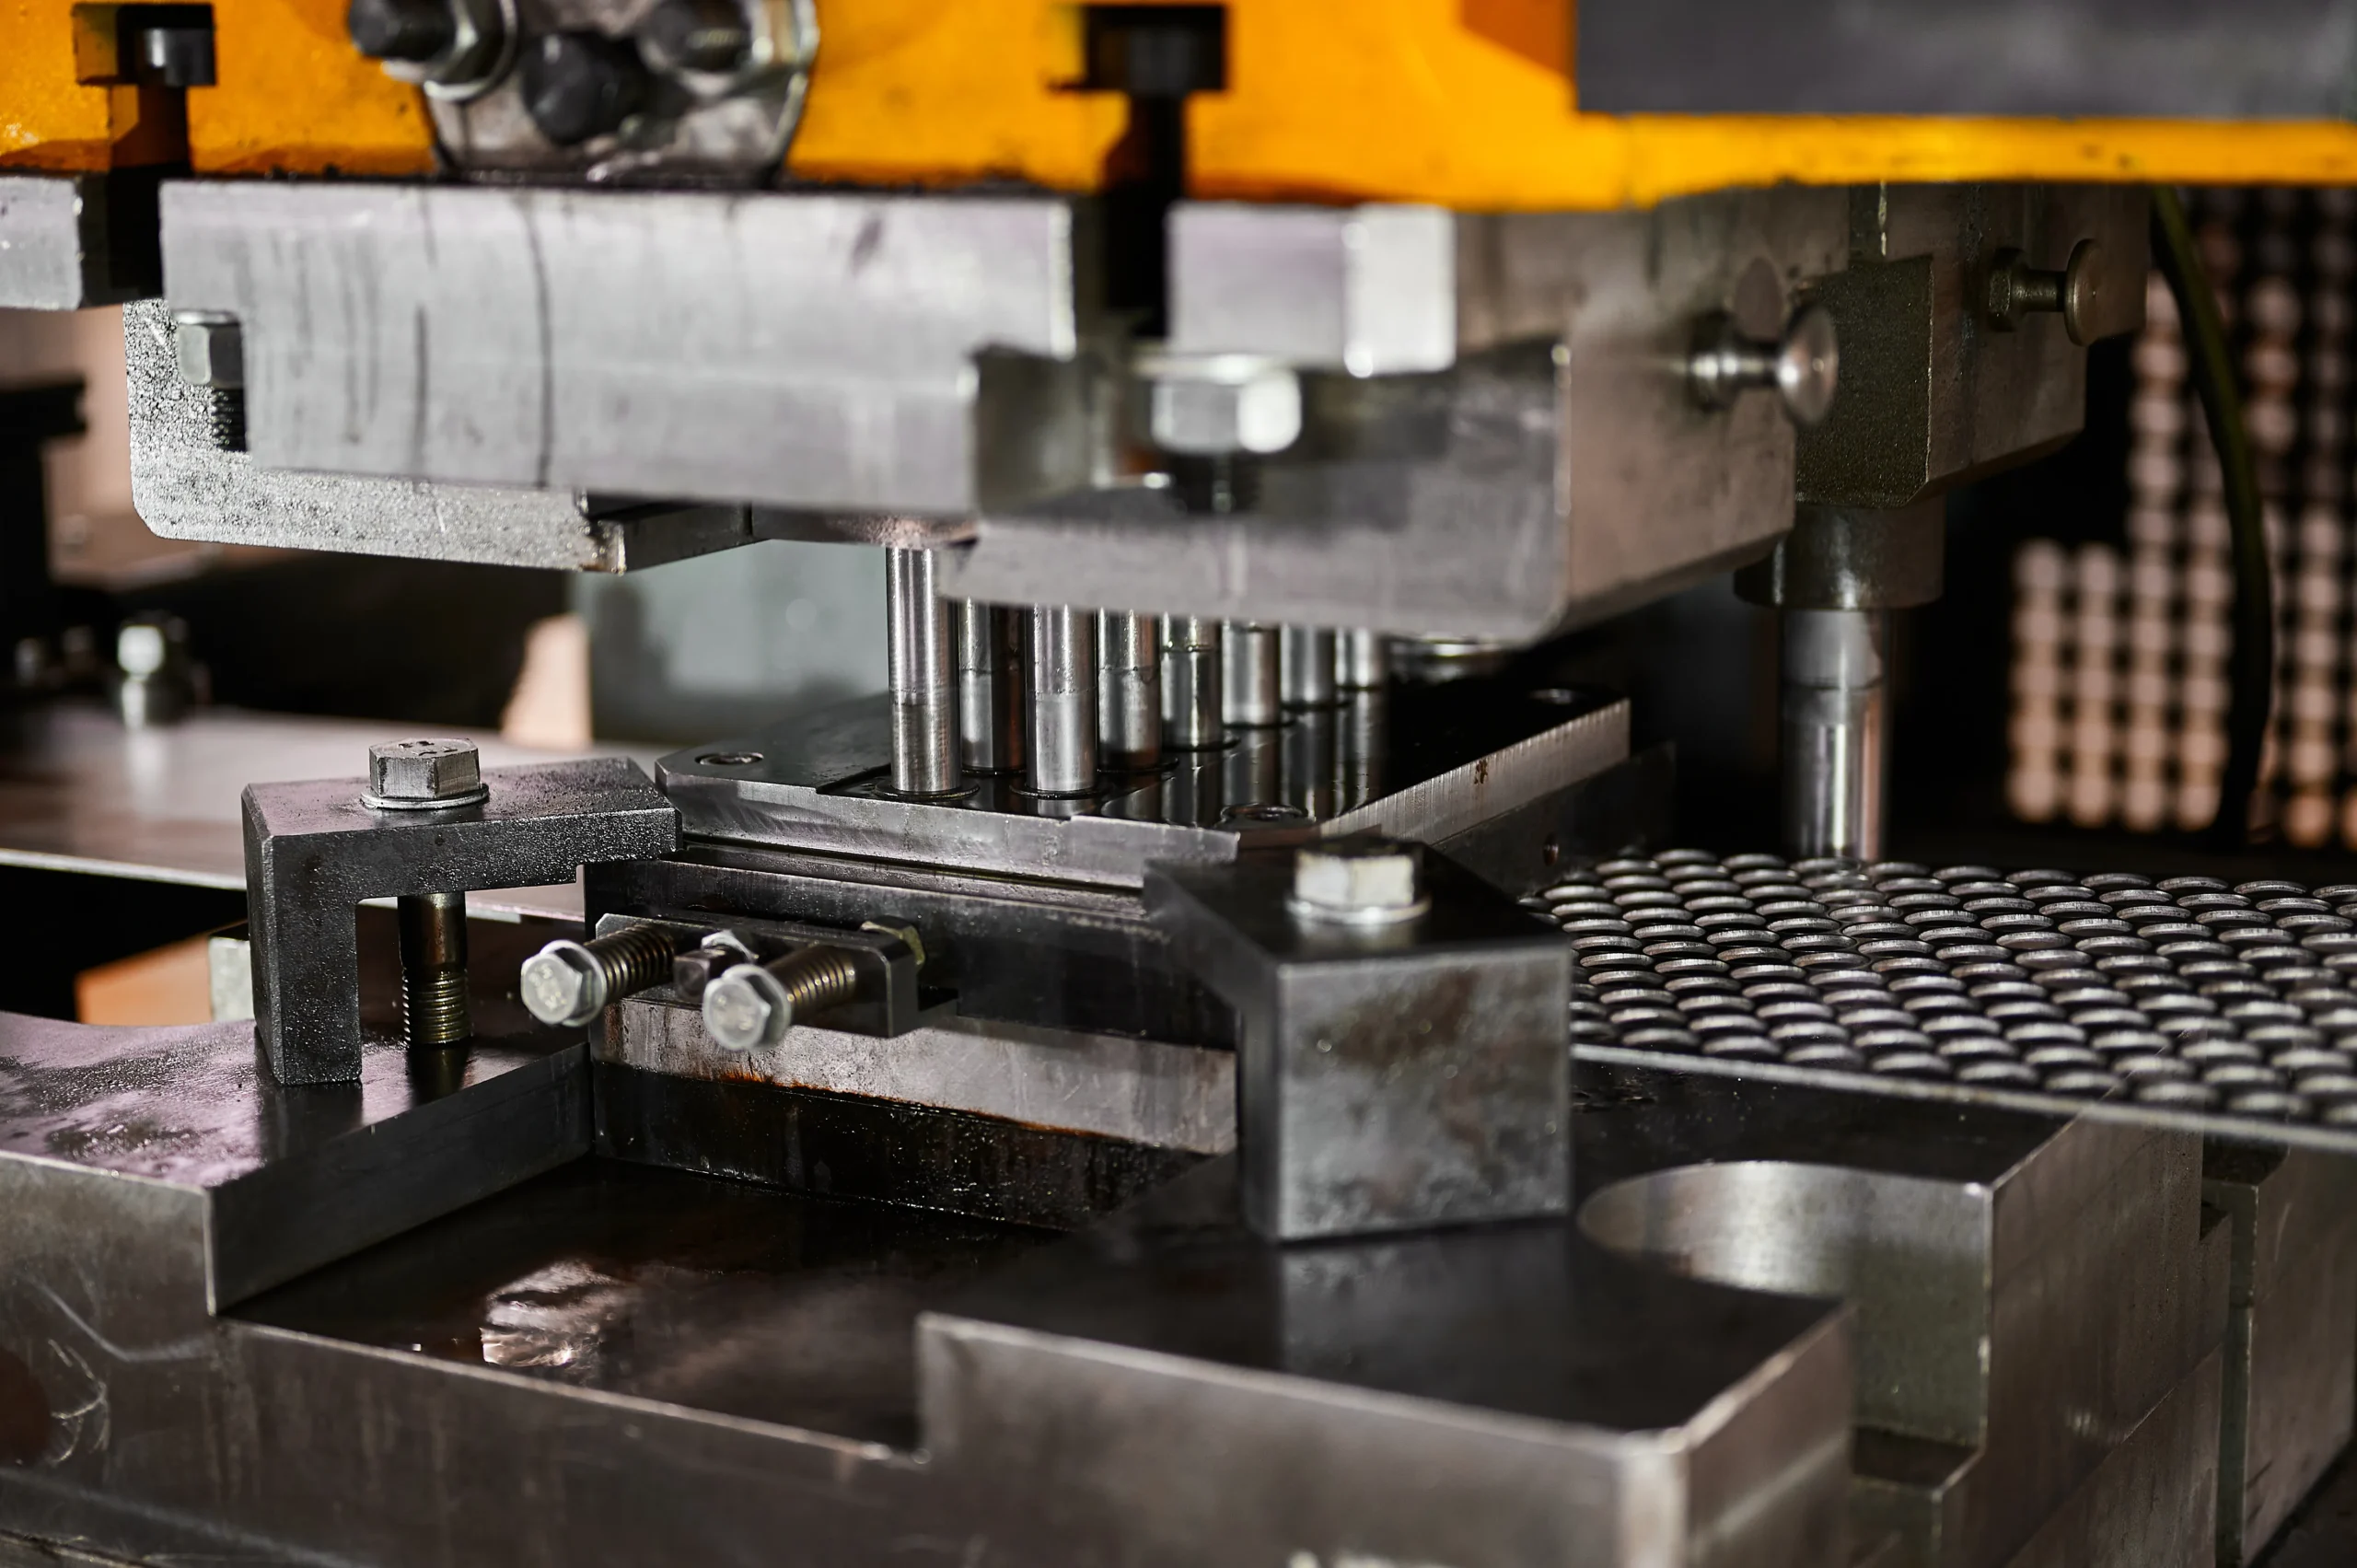
Progressive die stamping is an automated, high-precision metalworking process engineered to mass-produce complex sheet metal parts across continuous, uninterrupted production cycles. By feeding continuous coiled strip through a sequence of synchronized die stations, manufacturers execute multiple shearing, punching, and forming operations within a single press stroke. Global automotive and industrial OEMs depend on progressive die stamping to achieve tight dimensional tolerances, high structural rigidity, and uniform batch-to-batch repeatability while driving down per-unit manufacturing costs.
1. Progressive Die Stamping: High-Volume Precision Manufacturing for Automotive & Industrial OEMs
1.1 What Is Progressive Die Stamping?
1.1.1 Definition of progressive die stamping
Progressive die stamping is a cold-forming manufacturing technique that advances continuous coiled sheet metal through multiple aligned tooling stations within a single die block. Each individual station performs a distinct mechanical operation such as piercing, coining, or bending until the final station cuts the completed part free from the strip carrier.
1.1.2 How progressive die stamping differs from conventional stamping
Conventional stamping typically relies on single-operation or compound dies that require manual or robotic transfer of individual blanks between separate press beds. Progressive die stamping retains the workpiece on a continuous carrier ribbon, advancing the metal strip automatically through all fabrication stages to eliminate intermediate handling.
1.1.3 When progressive die stamping is the ideal manufacturing solution
Progressive die stamping represents the optimal production route for components requiring multiple complex geometries, high dimensional repeatability, and annual production volumes exceeding 50,000 units. The high upfront investment in multi-station tooling is quickly amortized by rapid press cycle speeds and minimal labor overhead.
1.1.4 Industries that rely on progressive die stamping
Automotive vehicle manufacturers, consumer electronics producers, industrial machinery builders, appliance brands, and medical device suppliers rely on progressive die stamping. These sectors require continuous streams of precision terminals, structural brackets, shielding cans, and safety-critical fasteners.
Progressive die stamping feeds continuous coiled sheet metal through multiple aligned tooling stations
1.2 Why Global OEMs Choose Progressive Die Stamping
1.2.1 High-volume production with consistent quality
Automotive assembly lines demand zero-defect component batches delivered in multimillion-unit quantities. Progressive die tooling maintains uniform cutting and forming dynamics across continuous production shifts, ensuring that parts produced at stroke 500,000 match the dimensional profile of stroke one.
1.2.2 Reduced cost per part
Progressive die stamping delivers one of the lowest piece-part costs in modern manufacturing. By automating coil feeding, strip positioning, and part ejection, the process minimizes direct labor expenses and maximizes machine stroke efficiency.
1.2.3 High repeatability and dimensional consistency
Because the workpiece remains mechanically anchored to the strip carrier ribbon until the final cutoff station, positional errors between forming stages are eliminated. Rigid pilot pins align the strip before every stroke, keeping dimensional tolerances locked within micron-level bands.
1.2.4 Improved production efficiency
Combining multiple stamping operations into a single press stroke shortens manufacturing lead times. Manufacturers eliminate work-in-progress (WIP) storage and secondary transit between separate forming machines, establishing a continuous, lean manufacturing flow.
1.2.5 Lower material waste and optimized strip utilization
Advanced strip layout software arranges blank profiles to maximize raw metal usage. Optimizing the nesting angle, carrier ribbon geometry, and station progression minimizes the scrap skeleton left after component cutoff, directly lowering raw coil expenditures.
2. How Progressive Die Stamping Works
2.1 Progressive Die Stamping Process
2.1.1 Coil feeding system
The manufacturing workflow begins at the coil handling line, where an uncoiler unrolls continuous raw metal strip. The coil passes through precision straightening rollers to eliminate coil set curvature before a high-speed servo feeder indexes the strip into the die set with pitch accuracy held within ± 0.01 mm.
2.1.2 Strip layout design
Before die fabrication, tooling engineers design a 2D and 3D strip progression layout. This blueprint defines the exact mechanical action occurring at each station, the position of pilot holes for strip location, and the configuration of the carrier ribbons supporting the workpiece.
2.1.3 Multi-station stamping sequence
As the press ram cycles downward, matched upper punches enter corresponding lower die cavities across all stations simultaneously. Internal holes are pierced, perimeter notches are cut, tabs are coined, and flanges are bent along the advancing strip in synchronized succession.
2.1.4 Finished part separation
At the final die station, a dedicated cutoff or blanking punch severs the completed component from the carrier ribbon. The finished part drops through an exit chute onto automated part conveyors, while the empty scrap skeleton is chopped into manageable segments for automated recycling.
2.2 Typical Operations Performed
2.2.1 Blanking
Blanking shears the exterior contour of a part section from the sheet metal strip. In progressive die setups, partial blanking creates reliefs around the workpiece, allowing adjacent metal to flow freely during subsequent forming stages while keeping the part attached to the carrier.
2.2.2 Piercing
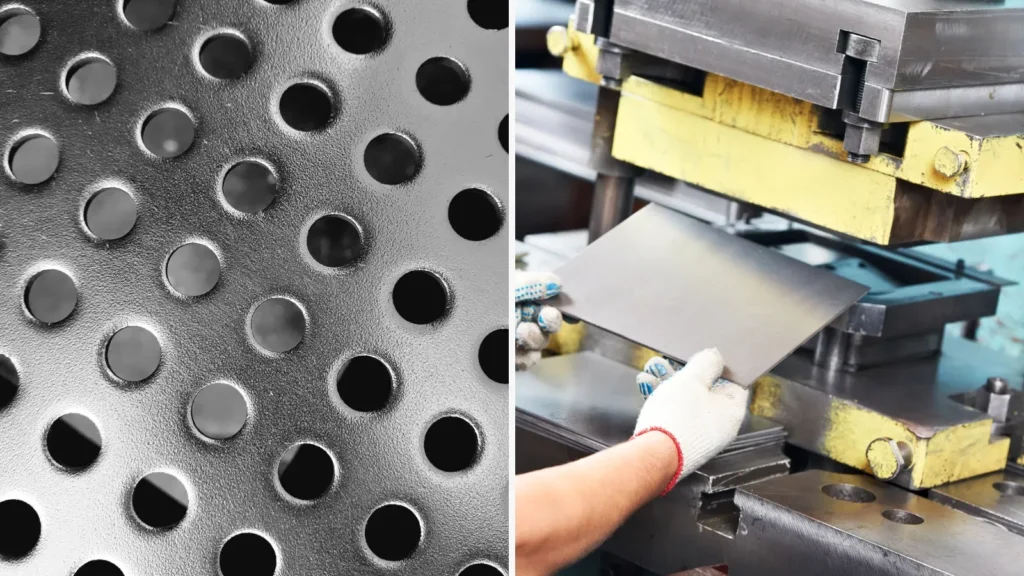
Piercing punches holes, slots, and complex cutouts through the strip. Slugs created during piercing drop through clearance holes in the lower die block and are evacuated downward, preventing slug pull-back defects on the die surface.
2.2.3 Bending
Bending deforms flat sheet metal along straight axes to create angles, U-channels, and edge flanges. High-precision progressive dies calculate elastic springback characteristics, integrating over-bending angles to achieve drawing-specified tolerances.
2.2.4 Forming
Forming deforms sheet metal along compound or curved contours without intentionally shearing material fibers. It produces complex contours, step-downs, and stiffening ribs, improving component rigidity without requiring heavier-gauge sheet stock.
2.2.5 Coining
Coining applies high compressive force to displace metal plastically within a closed die cavity. It produces sharp corner profiles, bevels, countersinks, and thinned sections, eliminating secondary countersink machining or deburring operations.
High-volume automotive parts achieve significant unit cost efficiency through progressive die stamping
2.2.6 Embossing
Embossing presses raised or recessed surface profiles such as part numbers, trace codes, stiffening patterns, or decorative ribbing into sheet metal using matched male and female dies without altering the nominal wall thickness.
2.2.7 Cutoff operations
The cutoff station separates the finished part from the carrier strip. Cutoff punches can execute simple straight shears or intricate parting lines, leaving smooth, burr-free edges on final assembly mating faces.
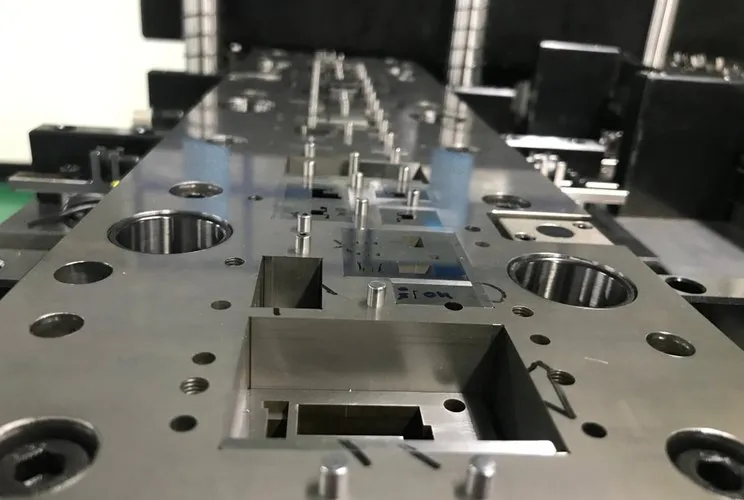
2.3 Components of a Progressive Die
2.3.1 Die set
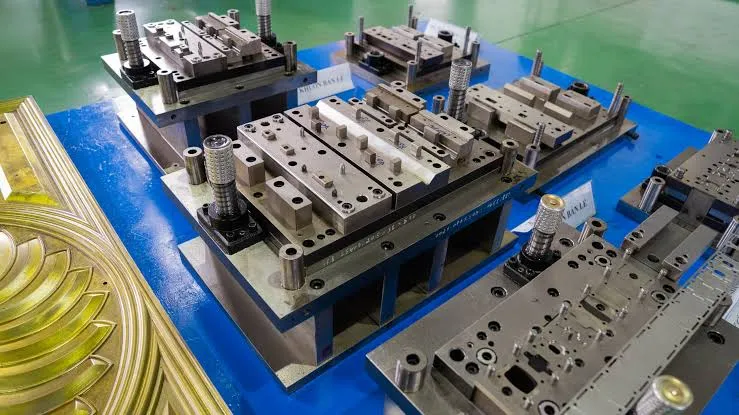
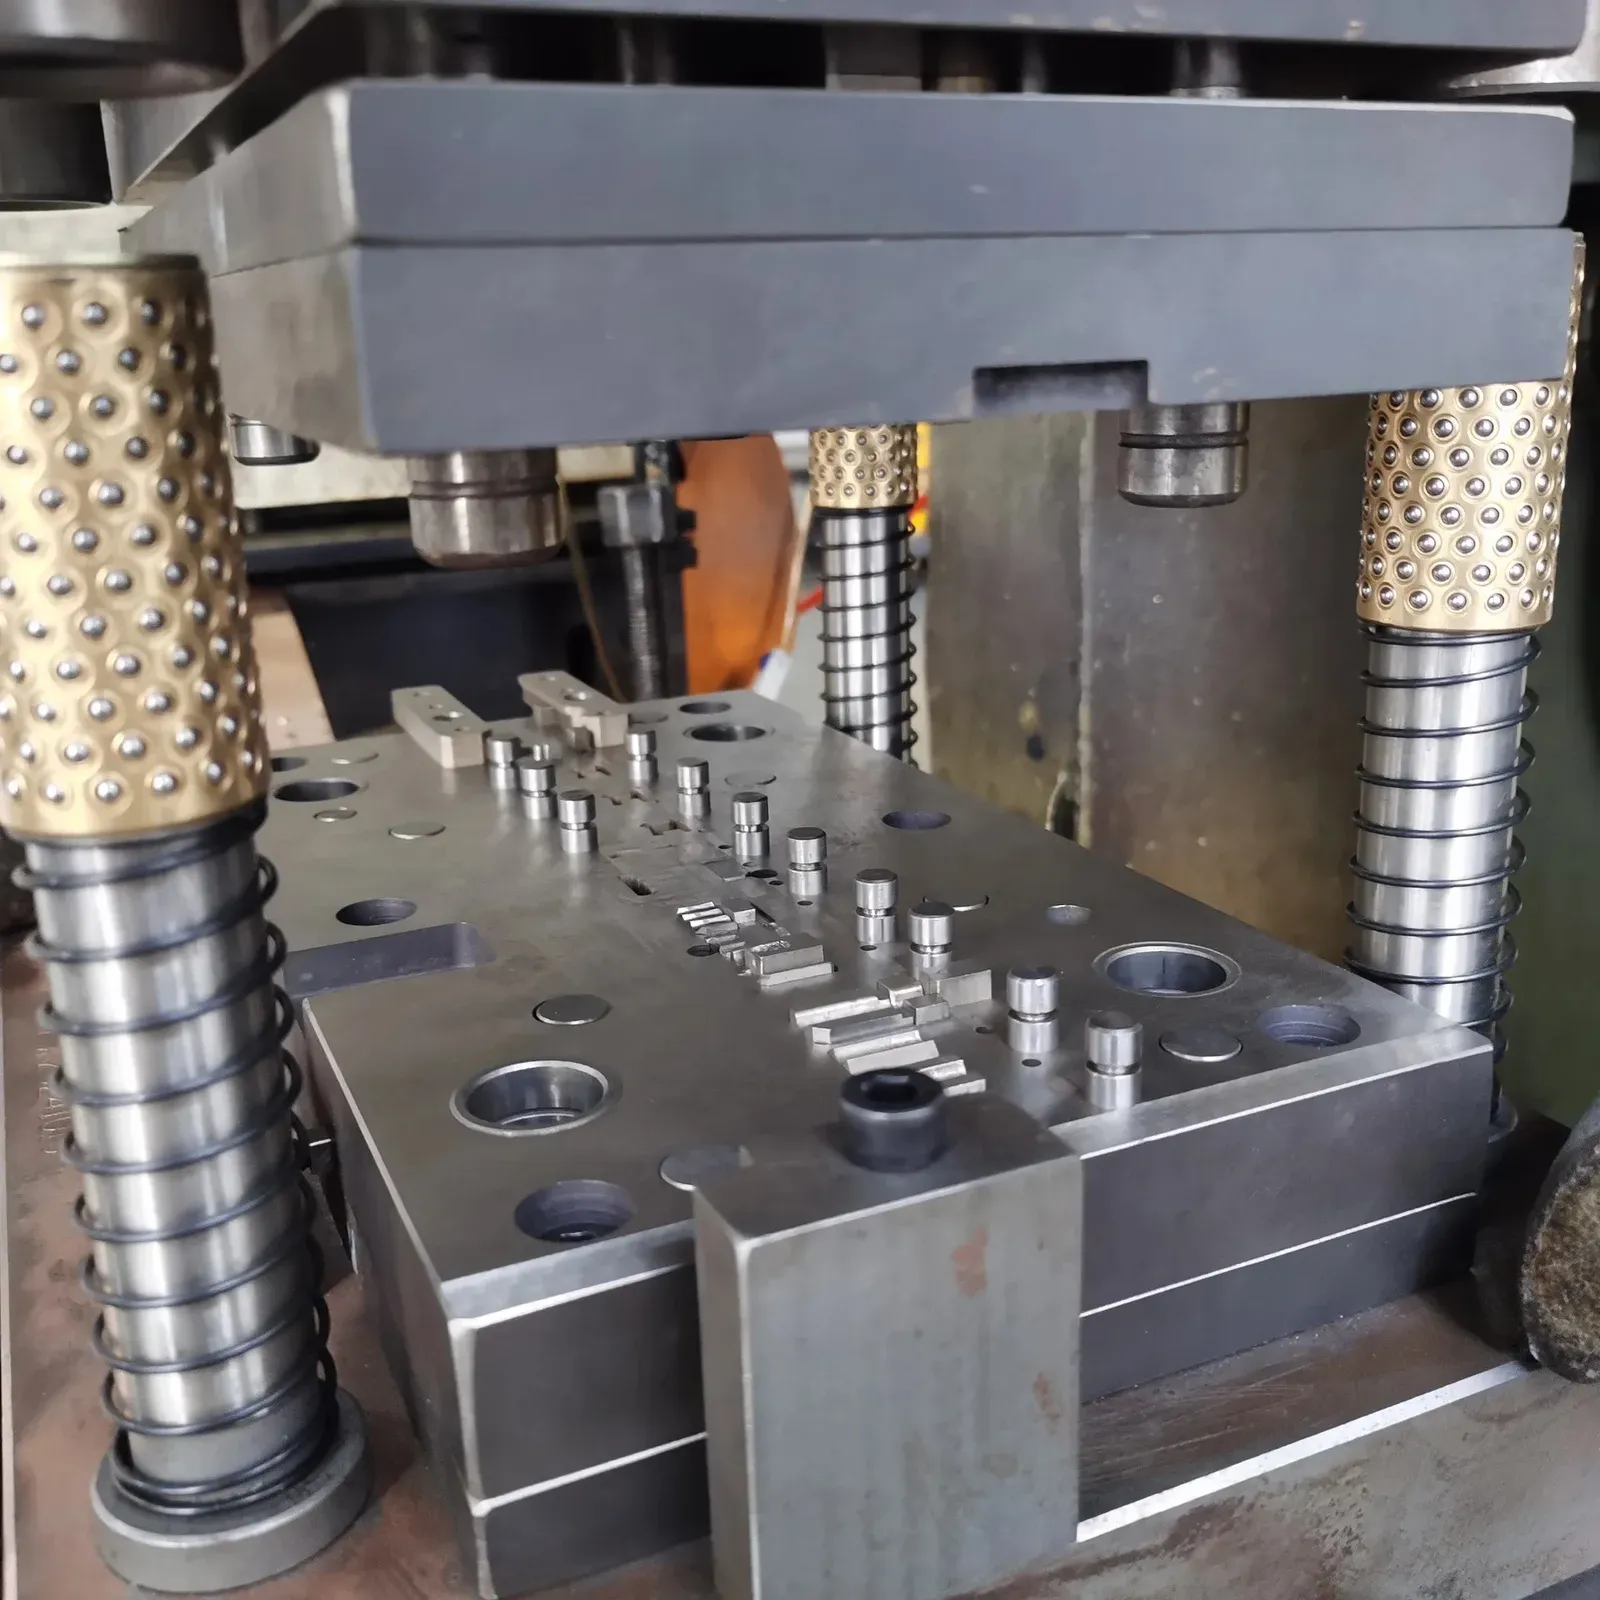
The die set comprises upper and lower die shoes constructed from precision-ground steel plates. The upper shoe mounts directly to the descending press ram, while the lower shoe bolts rigidly to the stationary press bolster bed.
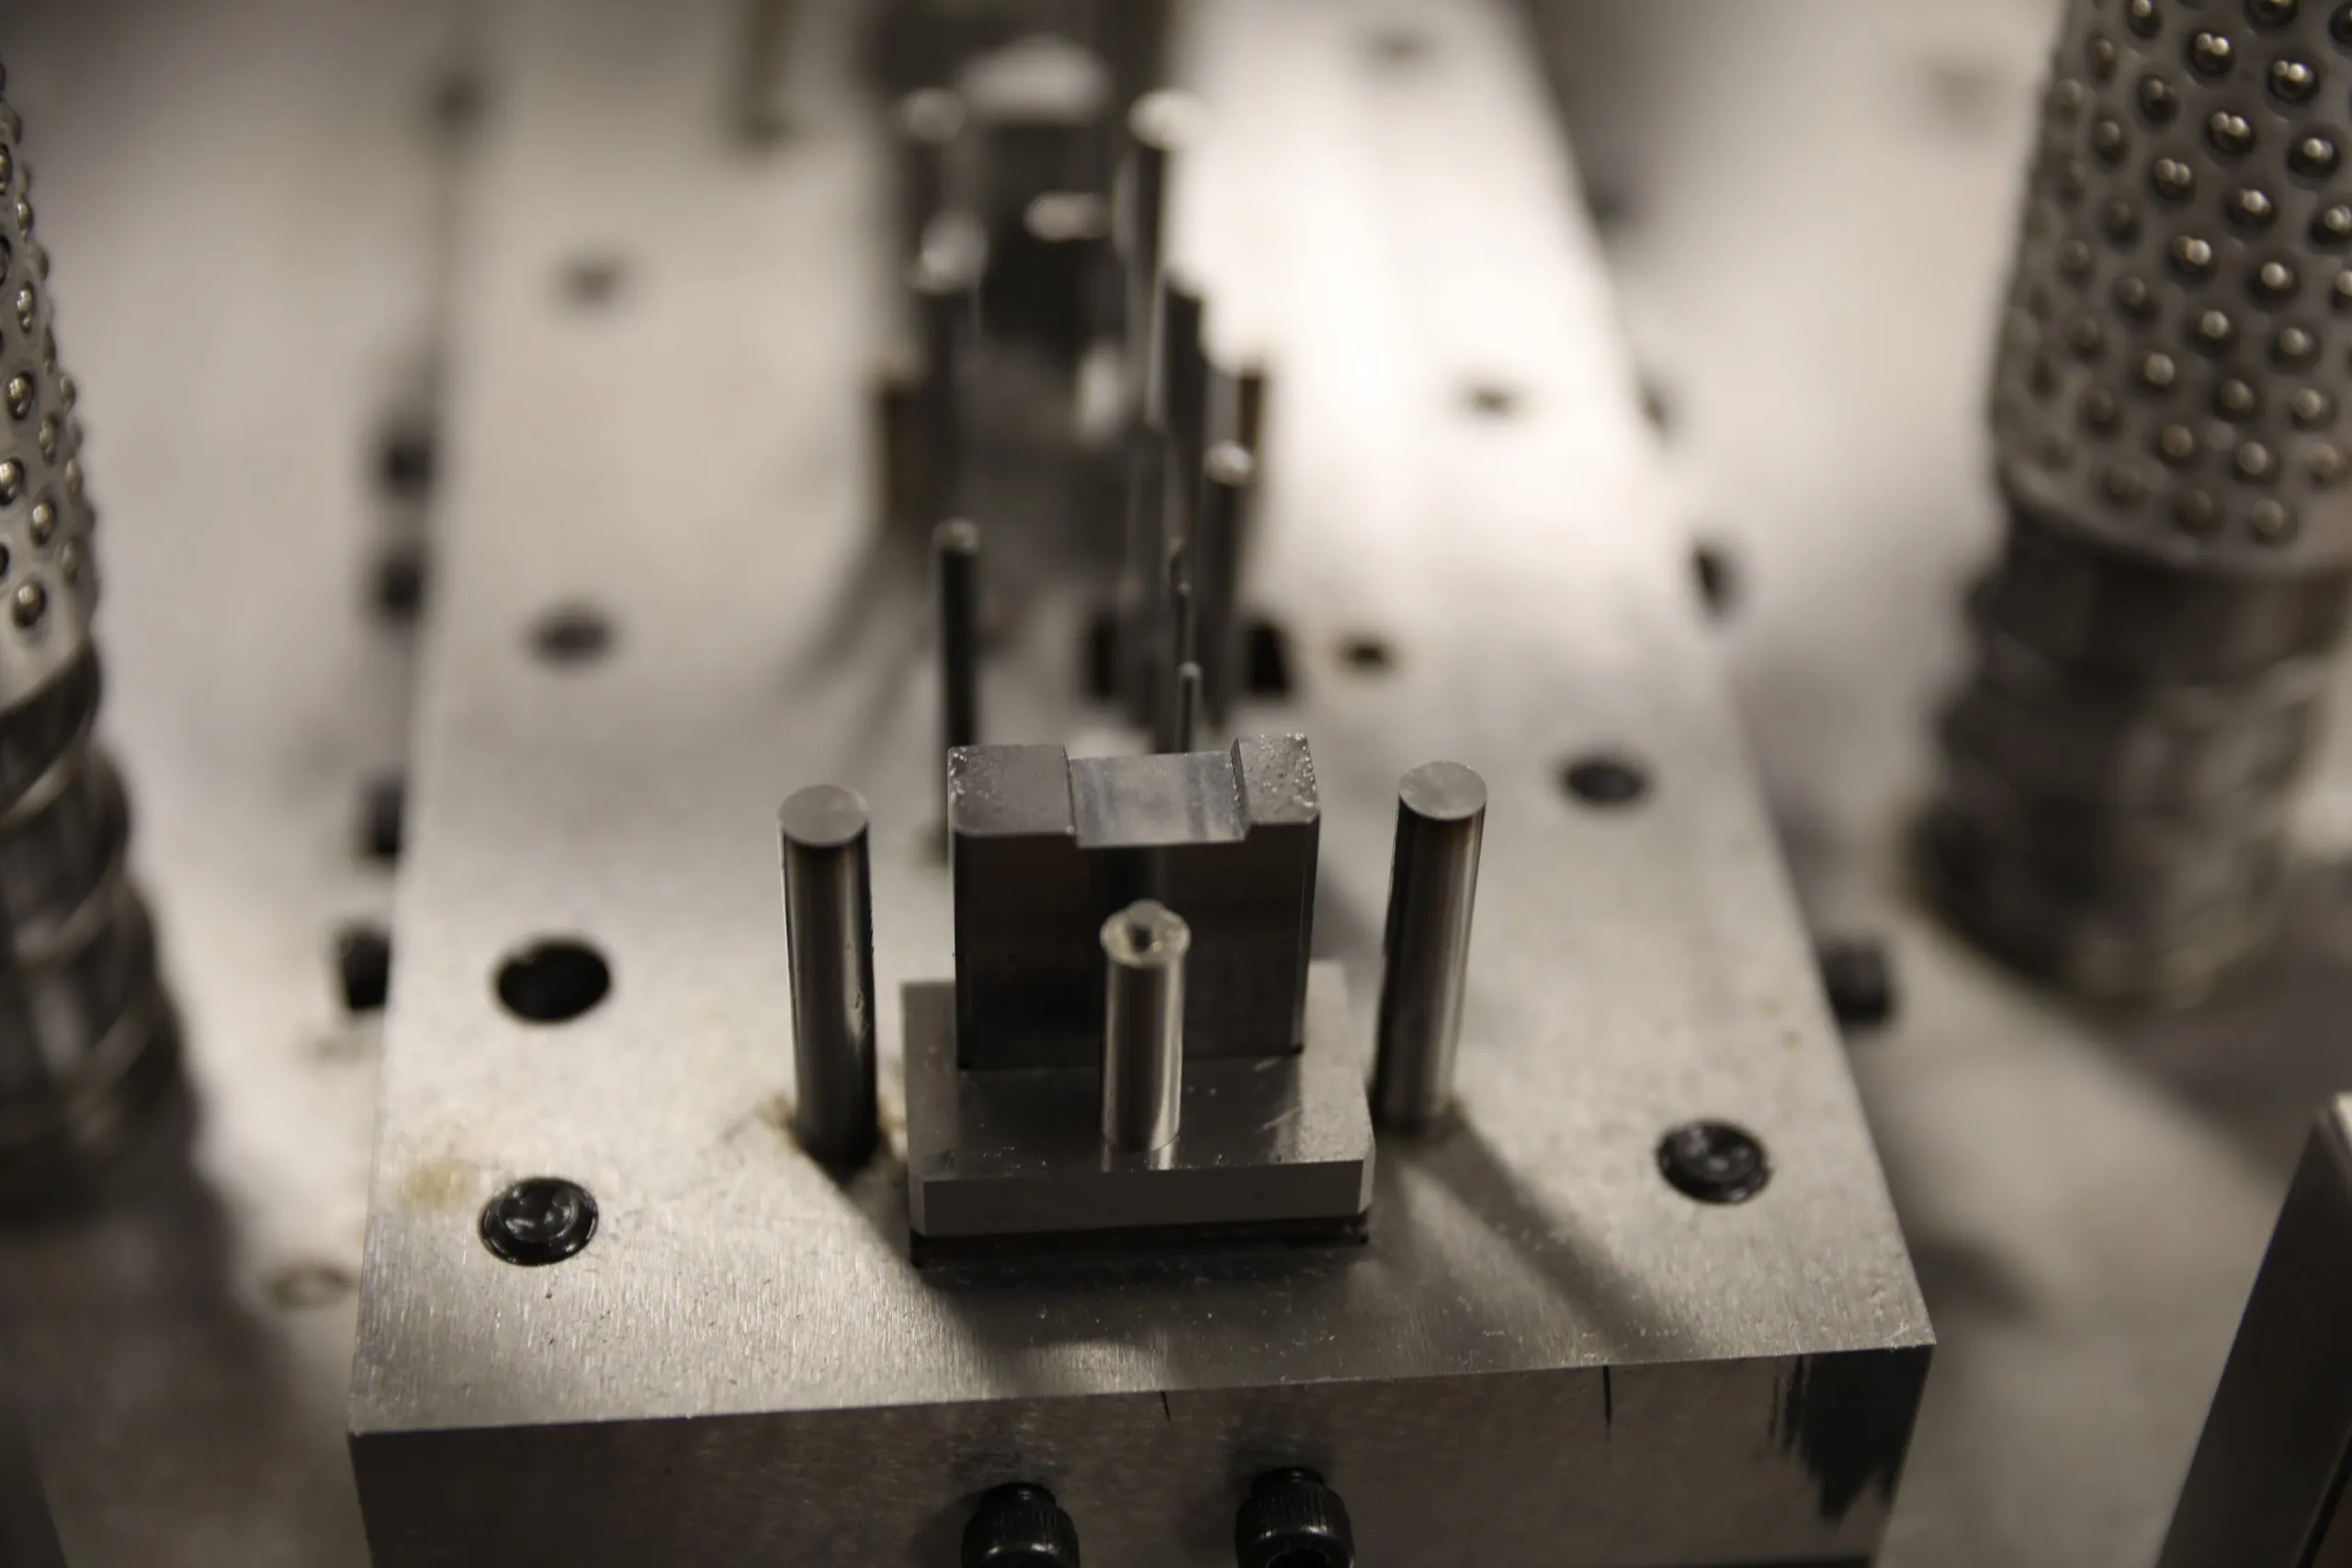
2.3.2 Punches
Punches are the male tooling components mounted to the upper die shoe. Machined from hardened tool steel or tungsten carbide, they contact the sheet metal to pierce holes, shear profiles, coin surfaces, or form bend angles.
2.3.3 Dies
Die blocks and matrix inserts are the female tooling elements housed within the lower die shoe. They feature matching openings and cavity geometries that accept the descending punches to shear, hold, and shape the material.
2.3.4 Guide pins
Hardened guide pins (pillars) and precision ball-bearing bushings connect the upper and lower die shoes. They eliminate lateral play during high-speed press strokes, maintaining punch-to-die alignment within ± 0.005 mm.
2.3.5 Stripper plates
Spring-loaded or nitrogen-actuated stripper plates clamp the sheet metal flat against the lower die block before punches make contact. After shearing, the plate strips the metal strip off the ascending punch bodies, preventing strip jams.
2.3.6 Coil feeder and press system
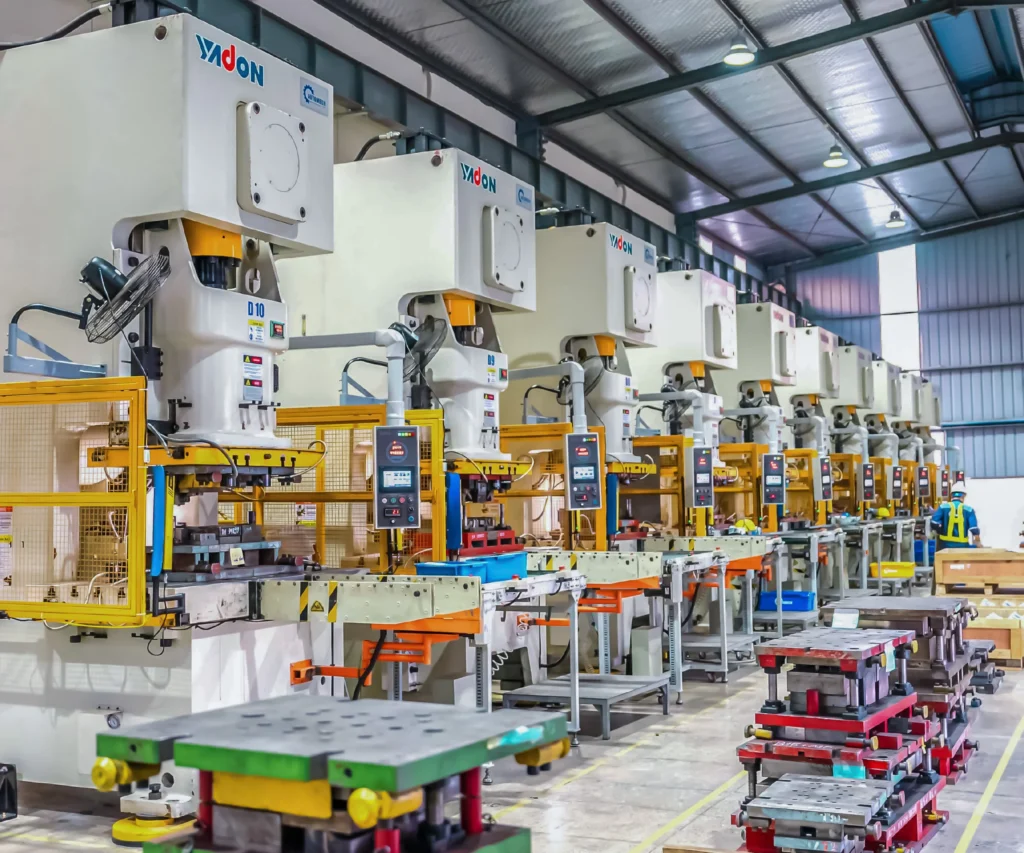
The mechanical or servo press system provides the structural tonnage, stroke speed, and motion control. Synchronized automated coil uncoilers, straighteners, and servo roll feeders advance the strip precisely between consecutive press strokes.
3. Progressive Die Tooling Design
3.1 Progressive Die Tooling Fundamentals
3.1.1 Progressive stamping dies
Progressive stamping dies are engineered systems integrating dozens of individual cutting and forming inserts into a single tool assembly. Their construction requires high structural rigidity to absorb cyclic impact loads and thermal stresses during long automated runs.
3.1.2 Progressive die tooling design
Tooling design begins with analyzing part geometries to determine the minimum number of stations required to form the part safely. Toolmakers balance the forming sequence across multiple stations to distribute press tonnage evenly across the die center of force.
3.1.3 CAD/CAM engineering workflow
Engineers model the complete die set in 3D CAD environments, simulating dynamic interference, stripper travel, and slug clearance. The digital models transfer to CAM software to generate high-speed CNC milling, grinding, and wire EDM toolpaths for hardened die components.
3.1.4 DFM considerations
Design for Manufacturability (DFM) reviews assess component geometries before die fabrication. Engineers evaluate corner radii, hole-to-edge clearances, and bend orientations relative to the sheet metal grain structure to eliminate tearing risks and reduce tool wear.
3.2 Tool Steel Selection
Progressive die stamping retains the metal workpiece on a continuous strip carrier ribbon
3.2.1 Common tool steel grades
Selecting the appropriate tool steel depends on the material being stamped and the expected production volume. Widely used grades include AISI D2, DC53, SKD11, and A2 for standard punches and die cavities, while tungsten carbide is chosen for high-wear cutting edges.
3.2.2 Wear resistance
Progressive dies experience abrasive and adhesive wear during high-speed shearing. High-carbon, high-chromium tool steels provide excellent edge retention, preventing premature punch rounding and burr formation across millions of strokes.
3.2.3 Heat treatment
Machined die components undergo vacuum heat treatment, followed by cryogenic stabilization and multiple tempering cycles. This thermal processing achieves hardness ratings between 58 and 62 HRC while preserving core impact toughness.
3.2.4 Tool life optimization
Applying Physical Vapor Deposition (PVD) surface coatings such as Titanium Aluminum Nitride (TiAlN) or Diamond-Like Carbon (DLC) reduces friction coefficients. Surface coatings prevent galling when stamping abrasive stainless steels or gummy aluminum alloys.
3.3 Strip Layout Optimization
3.3.1 Material utilization
Material utilization calculations determine the percentage of raw coil converted into finished parts versus scrap skeleton. Sophisticated CAD nesting algorithms evaluate nested, angular, or interlocking layouts to achieve utilization rates above 75% to 85%.
3.3.2 Scrap reduction
Scrap reduction strategies focus on minimizing web carrier widths, reducing station progression pitch, and combining adjacent blank perimeters. Lower scrap generation yields immediate cost savings on large production contracts.
3.3.3 Cost optimization
Optimizing strip progression minimizes the total die length, which allows toolmakers to use smaller press beds and lower-tonnage machines. Lower press operating rates and optimized raw material consumption lower total manufacturing costs.
4. Materials Used in Progressive Die Stamping
4.1 Carbon Steel
4.1.1 Low-carbon steel
Low-carbon cold-rolled steels (such as SPCC, ASTM A1008, and DC01) provide excellent formability, ductility, and weldability. They are widely used for deep drawing, multi-bend brackets, chassis clips, and functional hardware.
4.1.2 High-strength steel
High-Strength Low-Alloy (HSLA) steels deliver elevated yield strengths (300 to 550 MPa), allowing engineers to down-gauge sheet thickness while preserving mechanical rigidity in automotive structural brackets and chassis gussets.
4.2 Stainless Steel
Austenitic grades (AISI 301, 304, 316) and ferritic grades (AISI 430) provide corrosion resistance, high tensile strength, and heat tolerance. Progressive stamping of stainless steel is common for exhaust brackets, fuel system components, electrical contact springs, and medical clips, requiring rigid tooling to manage high cutting forces and work-hardening.
4.3 Aluminum Alloys
Aluminum alloys including 1100, 3003, 5052-H32, and 6061-T4 provide lightweight construction, high thermal conductivity, and natural corrosion resistance. Progressive dies stamp aluminum for EV battery module frames, electronic heat sinks, EMI shielding covers, and automotive body reinforcements.
4.4 Copper & Brass
Copper and copper-alloy strip stock (such as C1100 electrolytic tough pitch copper, C2600 cartridge brass, and C5191 phosphor bronze) offer superior electrical and thermal conductivity. These materials are stamped into automotive terminal connectors, EV busbars, relay contacts, switchgears, and lead frames.
4.5 High-Strength Automotive Materials
Modern automotive platforms require advanced high-strength steels (AHSS), such as Dual-Phase (DP600, DP800) and Martensitic grades, for crash-critical reinforcements, seatbelt latch mechanisms, and intrusion beams. Progressive dies for these materials utilize reinforced die shoes, premium carbide inserts, and high-tonnage servo presses to manage high yield strengths and severe springback behavior.
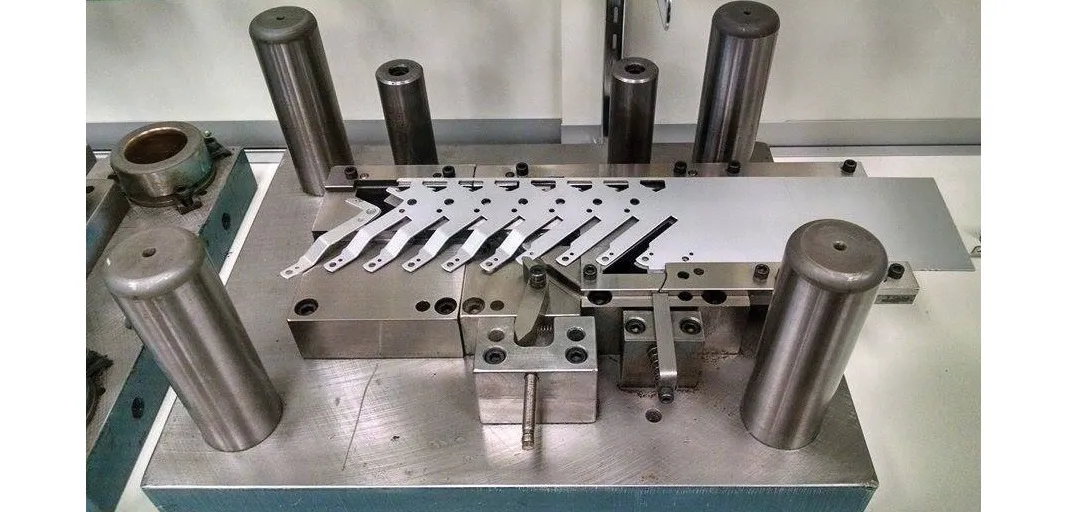
Modern progressive die stamping press lines operate at speeds exceeding five hundred strokes per minute
5. Progressive Die Stamping vs Other Manufacturing Methods
5.1 Progressive Die Stamping vs Transfer Stamping
5.1.1 Process comparison
Progressive die stamping retains the workpiece on a continuous metal carrier ribbon as it indexes through sequential stations inside a single die shoe. Transfer stamping utilizes mechanical transfer fingers, vacuum suction bars, or multi-axis robots to transport pre-cut discrete blanks between separate die stations or distinct press beds.
5.1.2 Production volume
Progressive die stamping delivers maximum efficiency for high-volume orders exceeding 50,000 to millions of parts annually, operating at high stroke speeds. Transfer stamping is typically selected for medium-to-high volume runs of larger, heavier components where carrier strip connection is mechanically unfeasible.
5.1.3 Tooling complexity
Progressive die tooling integrates cutting, forming, and cam-activated bending mechanisms into a single continuous tool block with tight station pitches. Transfer tooling utilizes discrete, modular die sets positioned across multiple stations, requiring synchronized transfer rail programming and clearance management.
5.1.4 Cost comparison
Progressive dies involve higher upfront tool design and fabrication costs, but achieve the lowest unit cost for small-to-medium parts. Transfer stamping requires higher press tonnage investments and transfer automation, yet saves material expenses on large parts by eliminating the scrap carrier ribbon.
| Comparison Parameter | Progressive Die Stamping | Transfer Stamping |
| Workpiece Handling | Continuous strip carrier ribbon | Discrete blanks moved via transfer rails |
| Production Speed | High (100 to 500+ parts/minute) | Moderate (15 to 40 parts/minute) |
| Max Part Size | Small to Medium (Limited by coil width) | Large structural panels and deep shells |
| Material Utilization | Moderate (Produces scrap carrier web) | High (Optimized standalone blank nesting) |
| Initial Tooling Cost | High (Single integrated multi-station die) | High (Multiple die sets plus transfer tooling) |
| Optimal Annual Volume | > 50,000 units | 20,000 to 100,000+ units |
5.2 Progressive Die Stamping vs Single-Stage Stamping
5.2.1 Cycle time
Progressive die stamping completes an entire finished part with every stroke of the press ram, achieving cycle times measured in fractions of a second. Single-stage stamping requires separate press setups for each operation, resulting in significantly longer cumulative cycle times per part.
5.2.2 Productivity
Automated coil-fed progressive stamping operates continuously without operator handling, delivering hundreds of parts per minute. Single-stage stamping requires manual or robotic loading and unloading between individual presses, limiting hourly output and increasing work-in-progress inventory.
5.2.3 Tooling investment
Single-stage dies carry lower upfront tooling costs, making them economical for prototypes, pilot production, or low-volume custom manufacturing. Progressive dies demand substantial upfront toolroom capital, which is amortized over high-volume mass production runs to deliver low piece-part costs.
5.3 Progressive Die Stamping vs CNC Machining
5.3.1 Production speed
Progressive die stamping forms finished sheet metal components in seconds, producing thousands of parts per hour. Subtractive CNC milling or turning removes material incrementally via rotary cutters, requiring minutes or hours to machine a single component from solid billet stock.
5.3.2 Precision
CNC machining delivers ultra-tight tolerances (down to ± 0.002 mm) across complex 3D prismatic features, deep bores, and contoured surfaces. Progressive die stamping maintains repeatable sheet metal tolerances of ± 0.01 mm to ± 0.02 mm, satisfying automotive functional assembly standards.
5.3.3 Part complexity
Progressive die stamping is restricted to uniform-thickness sheet metal geometries featuring pierced holes, formed flanges, shallow recesses, and coined edges. CNC machining accommodates complex three-dimensional contours, solid blocks, variable wall thicknesses, and undercut geometries.
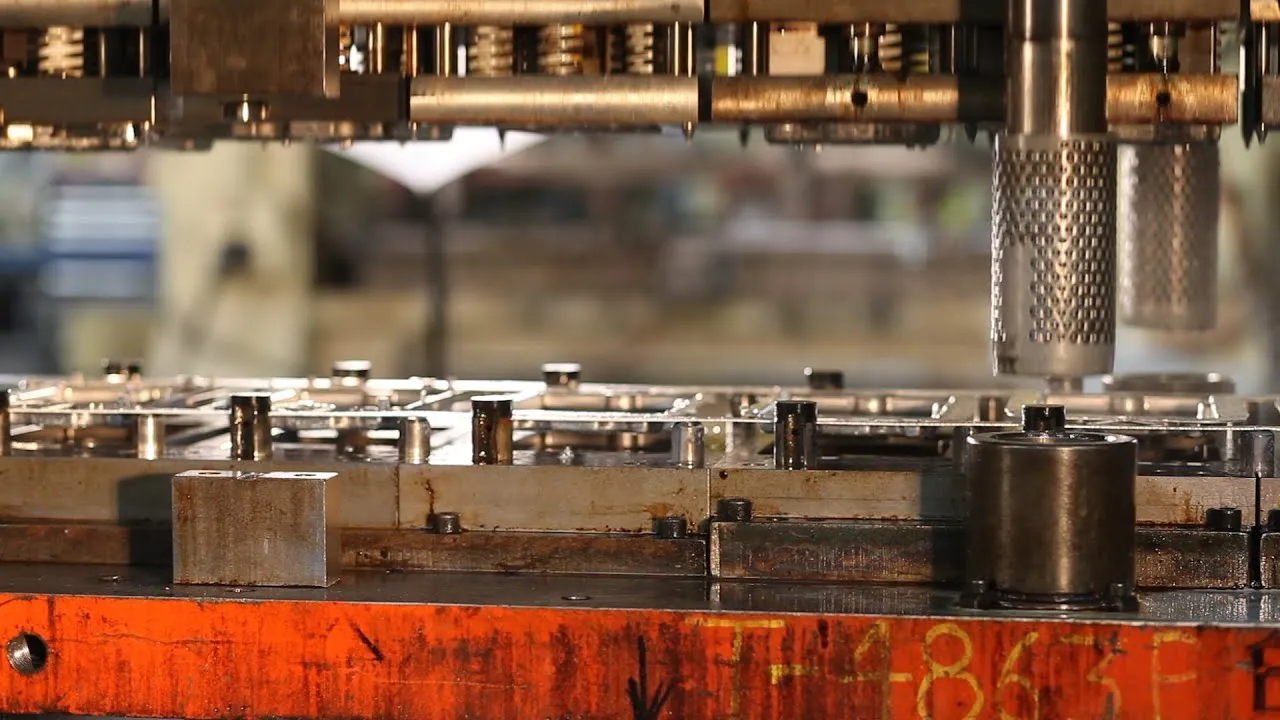
Automotive suppliers utilize progressive die stamping to manufacture rigid engine mounting brackets
5.3.4 Unit cost
Progressive die stamping delivers unit costs measured in pennies at high production volumes due to rapid press cycles and minimal material waste. CNC machining unit costs remain relatively flat regardless of batch size due to machine cycle time, cutting tool consumption, and chip generation.
5.3.5 Suitable production volumes
CNC machining is the preferred choice for rapid prototypes, custom fixtures, and low-volume production runs under 1,000 units. Progressive die stamping requires large production runs exceeding 50,000 units to offset non-recurring engineering (NRE) and tooling investments.
| Manufacturing Metric | Progressive Die Stamping | CNC Machining |
| Material State | Sheet metal coil or strip | Solid billet, plate, or bar stock |
| Cycle Time | Fractions of a second (< 1 sec) | Minutes to hours per part |
| Unit Cost at Scale | Extremely Low | Moderate to High |
| Tooling Investment | High (Dedicated stamping die) | Low (Standard cutters & modular fixtures) |
| Ideal Production Volume | High Volume (> 50,000 parts) | Prototype to Low Volume (< 1,000 parts) |
| Material Scrap | Low to Moderate (Scrap skeleton) | High (Subtractive chips) |
6. Precision, Quality & Manufacturing Control
6.1 Dimensional Accuracy
6.1.1 Tight tolerances
High-precision progressive stamping dies achieve linear tolerances down to ± 0.01 mm and hole positional tolerances within ± 0.02 mm. Achieving this precision requires precision guide pillars, ground tungsten carbide punches, and hardened pilot pins that locate strip progression before every stroke.
6.1.2 Burr control
Exit burr formation is controlled by maintaining precise punch-to-die cutting clearances, calculated between 5% and 10% of material thickness. Integrating in-die shaving stations and regular punch sharpening maintains burr heights below 10% of sheet thickness, eliminating secondary edge-finishing steps.
6.1.3 Flatness control
Relieving internal stresses during strip progression prevents part warping and oil-canning. Die designers incorporate in-die coining, reverse bending, and spring-loaded pressure pads across flattening stations to ensure finished brackets and mounting plates maintain critical planar datums.
6.1.4 Surface finish requirements
Functional sealing faces, busbar contact surfaces, and cosmetic brackets require defect-free surfaces free of die marks or galling. Utilizing synthetic stamping lubricants, polished die cavities, and hardened PVD-coated tooling components ensures finished surface roughness profiles below Ra 0.4 µm.
6.2 High-Speed Production
6.2.1 High-speed stamping
High-speed progressive presses operate at speeds ranging from 150 to 500+ strokes per minute for heavy automotive parts, and up to 1,500 strokes per minute for miniature electronic connectors. Dynamic balancing and counterweighted rams absorb inertial forces during high-speed operation.
6.2.2 Press tonnage selection
Selecting appropriate press tonnage requires calculating total shear resistance, forming force, coining pressure, and stripping force across all active stations. Applying a 25% to 30% safety margin ensures the press frame resists deflection under dynamic cyclic loads.
6.2.3 Production efficiency
High-speed stamping lines optimize Overall Equipment Effectiveness (OEE) through automated coil handling, straighteners, and servo feeders. Scrap choppers evacuate scrap skeletons continuously, while acoustic and optical part-ejection sensors prevent die jams.
6.3 Die Maintenance
6.3.1 Preventive maintenance
Preventive maintenance protocols follow strict press stroke intervals. Toolmakers dismantle die blocks to clean internal guide tracks, lubricate mechanical cam slides, inspect nitrogen springs, and verify punch alignment before micro-cracks propagate.
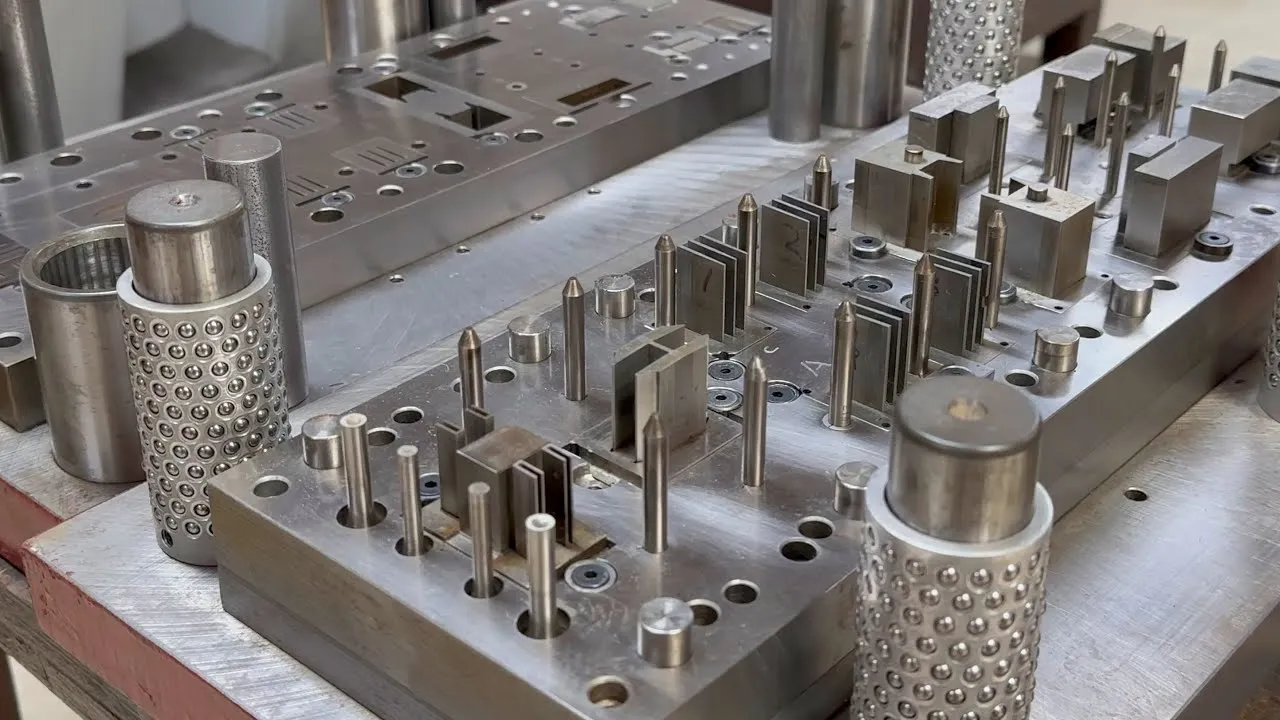
Progressive die stamping eliminates manual part handling between successive punching and bending stations
6.3.2 Tool wear monitoring
Optical toolmakers’ microscopes and contact profilometers measure punch cutting-edge radii during scheduled stops. Tracking edge breakdown and monitoring burr growth on sample parts allows technicians to schedule die regrinding before dimensional drift causes non-conformance.
6.3.3 Predictive maintenance
Modern progressive stamping lines integrate in-die piezoelectric tonnage sensors and vibration monitors. Detecting abnormal tonnage spikes or unbalanced eccentric loads alerts operators to strip misfeeds or punch dulling, enabling predictive maintenance that prevents catastrophic tool failure.
7. Secondary Operations & Assembly
7.1 Secondary Manufacturing Processes
7.1.1 Deburring
Centrifugal barrel finishing, vibratory tumbling, and automated abrasive belt sanding eliminate micro-burrs along sheared edges. Deburring creates smooth edge breaks, ensuring safe handling on assembly lines and preventing stress cracks during subsequent forming operations.
7.1.2 Tapping
In-die mechanical or servo-driven tapping units thread holes directly inside the progressive die before final part cutoff. For heavy structural components, secondary multi-spindle CNC tapping machines produce clean, chip-free internal threads according to standard metric or inch pitch specifications.
7.1.3 Welding
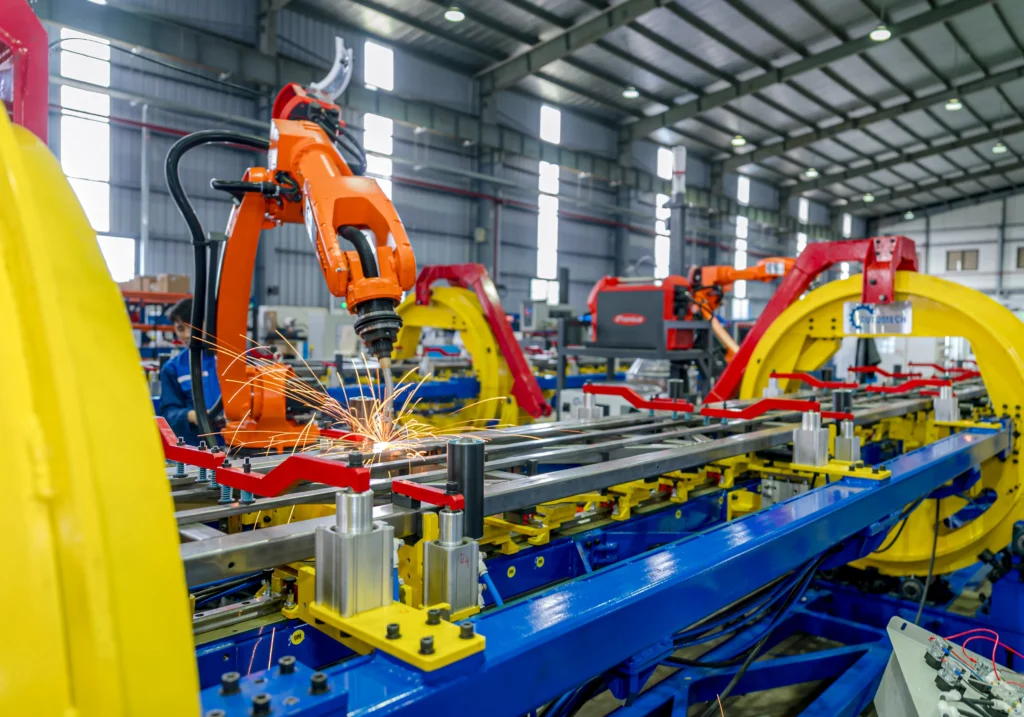
Stamped sub-components are welded into rigid structural modules using resistance spot welding, MIG (GMAW), TIG (GTAW), or laser welding. Robotic welding cells deliver repeatable seam quality and high weld penetration across structural automotive chassis nodes.
7.1.4 Riveting
Automated mechanical joining integrates self-piercing rivets (SPR), blind rivets, and solid rivets to join stamped brackets with cast or extruded sub-assemblies. In-die and secondary fastener installation heads insert threaded PEM nuts, studs, and standoffs into pre-pierced holes.
7.1.5 Surface treatment
Corrosion resistance and surface hardness are enhanced through electro-zinc plating, hot-dip galvanizing, cataphoresis (E-coating), powder coating, or anodizing. Surface conversion treatments satisfy 480-hour to 1,000-hour salt spray corrosion test standards for automotive underbody components.
7.2 Welding & Assembly Integration
7.2.1 Automotive stamping assembly
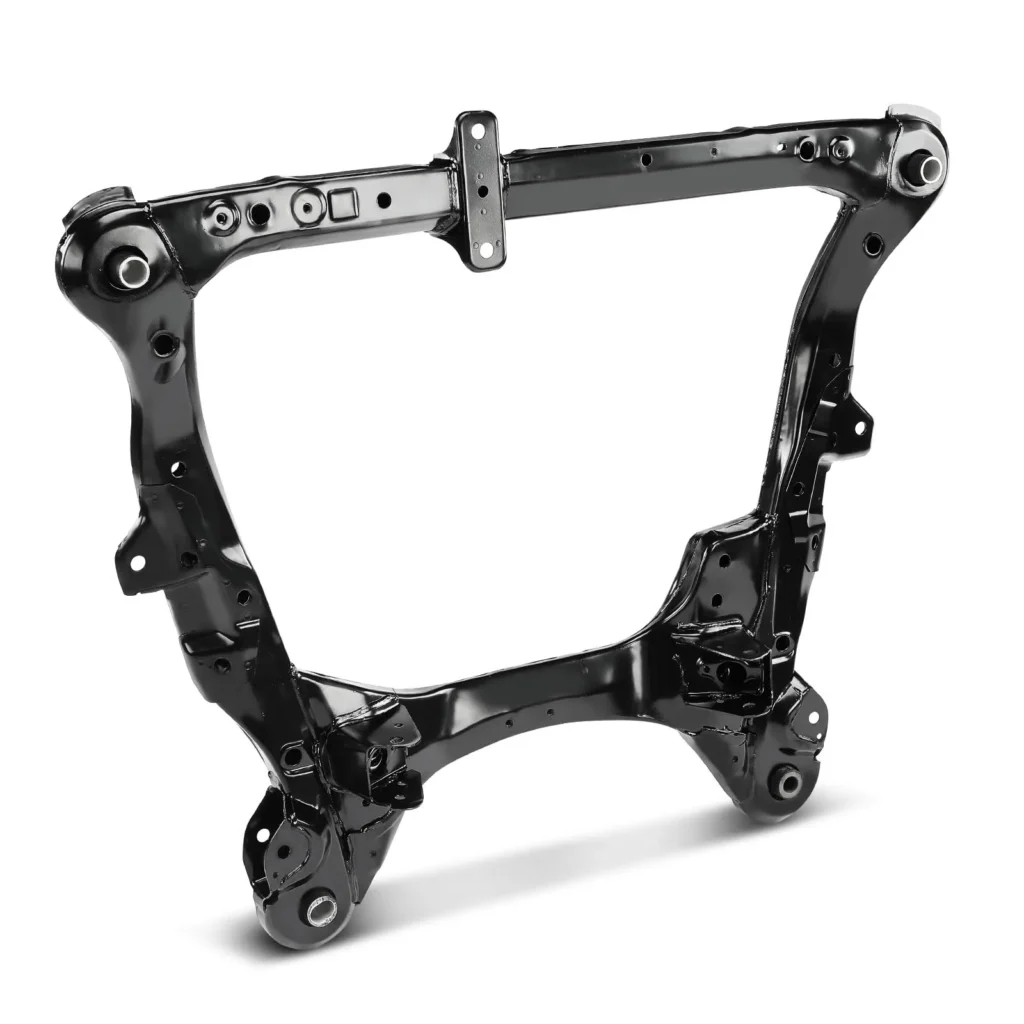
Automotive stamping assembly merges multiple stamped sheet metal parts such as gussets, brackets, channels, and plates into cohesive functional modules. Synchronizing press outputs with assembly operations streamlines production of seat tracks, crossmembers, and suspension links.
7.2.2 Fixture-controlled assembly
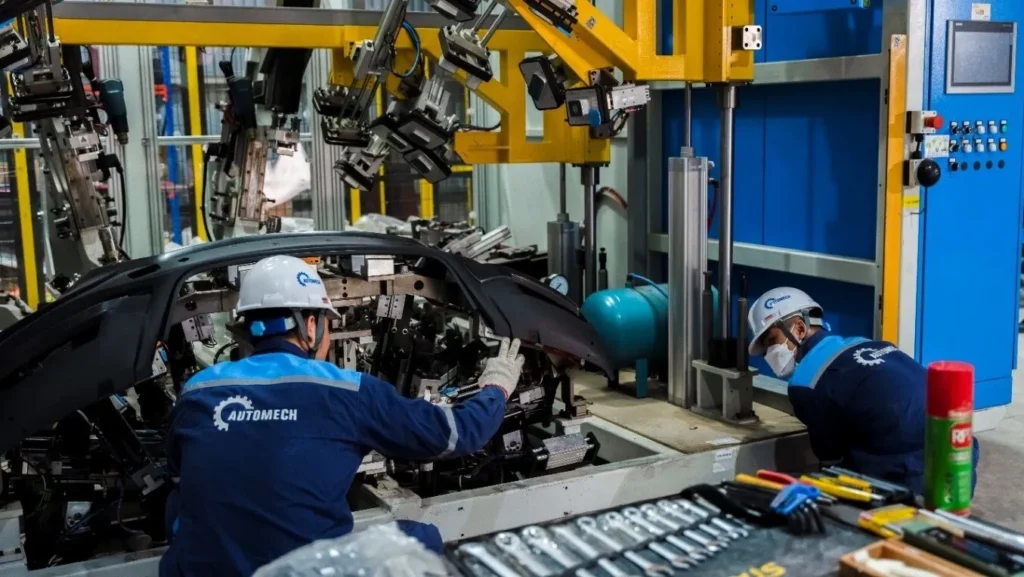
Custom welding and assembly jigs utilize CNC-machined locating blocks, hardened dowel pins, and pneumatic clamps to hold stamped sub-components in precise alignment. Rigid fixture structures counteract thermal weld distortion and ensure final assembly dimensions remain within drawing tolerances.
7.2.3 OEM sub-assembly manufacturing
Full-service contract manufacturers provide turnkey sub-assembly production, delivering ready-to-install modules directly to OEM vehicle assembly lines. Single-source delivery reduces supply chain complexity, lowers inbound logistics costs, and consolidates quality assurance accountability.
8. Automotive Applications of Progressive Die Stamping
8.1 Common Automotive Stamped Components
8.1.1 Automotive brackets
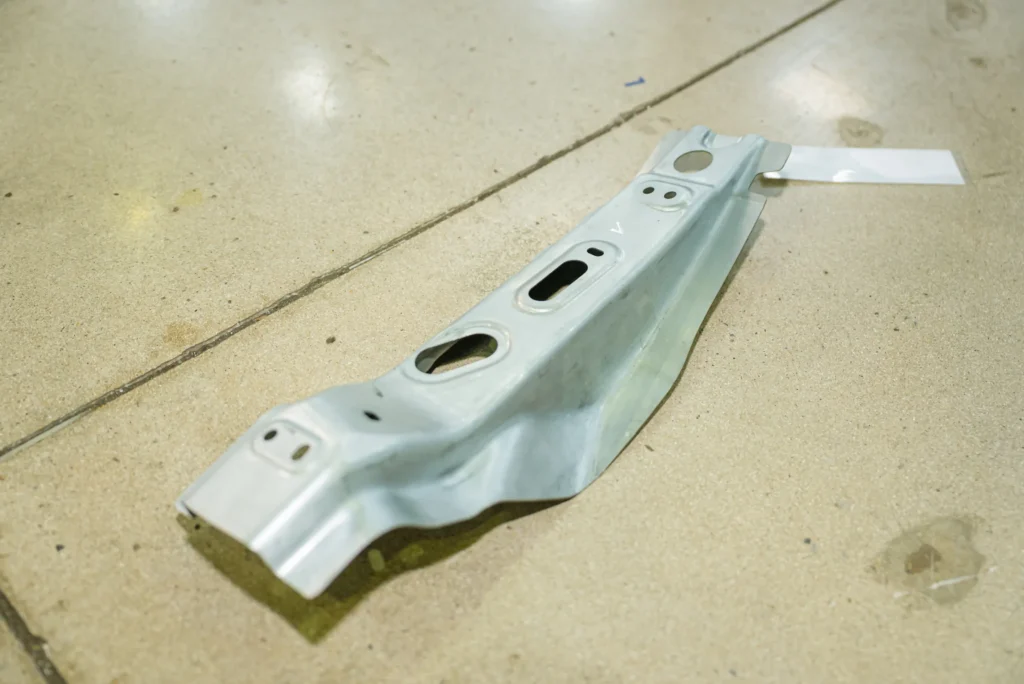
Progressive die stamping mass-produces engine mounting brackets, alternator supports, and exhaust hanger brackets from thick-gauge carbon steel. These structural brackets endure continuous mechanical vibration, thermal expansion cycles, and road shock loads.
8.1.2 Reinforcement parts
Safety-critical reinforcement components including door intrusion beams, B-pillar stiffeners, and bumper beam reinforcements are stamped from advanced high-strength steels (AHSS). Progressive dies form stiffening ribs and flanges that optimize dynamic energy absorption during vehicle collisions.
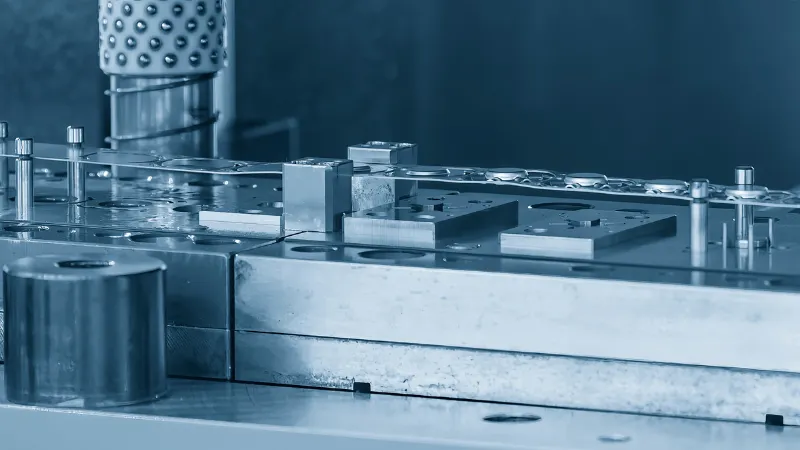
Toolmakers optimize strip nesting layout in progressive die stamping to minimize scrap waste
8.1.3 Mounting brackets
Precision mounting brackets secure electronic control units (ECUs), ADAS radar sensors, camera modules, and cooling lines throughout the engine bay and chassis. Multi-station progressive dies stamp intricate mounting tabs and locating features held to tight positional tolerances.
8.1.4 Seat components
Automotive seating mechanisms rely on progressive die stamping to manufacture seat recliner plates, height adjuster brackets, seat track rails, and belt anchor latches. These components require tight dimensional tolerances to ensure smooth mechanical movement and passenger safety compliance.
8.1.5 Chassis parts
Chassis assemblies utilize stamped subframe connectors, control arm reinforcement gussets, and shock tower brackets. High-tonnage progressive dies process heavy-gauge sheet steels (3.0 mm to 6.0 mm thick) to deliver high dynamic fatigue resistance.
8.1.6 Body structural components
Body-in-white (BIW) structures utilize progressive stampings for floor pan crossmembers, roof rail brackets, wheelhouse reinforcements, and firewall mounting plates. Stamped parts provide high torsional stiffness to modern automotive body frames.
8.2 OEM Metal Stamping Parts
8.2.1 Tier 1 production
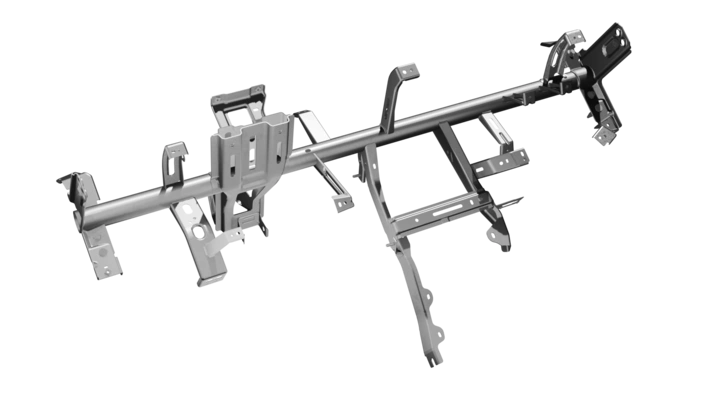
Tier 1 suppliers integrate progressive stamped components into complete brake boosters, steering columns, dashboard cross-beams, and transmission modules. Contract stamping partners deliver zero-defect batches aligned with Just-In-Time (JIT) delivery schedules.
8.2.2 Tier 2 production
Tier 2 stamping manufacturers produce specialized clips, clamps, spring washers, and functional brackets for Tier 1 modular sub-systems. High-speed progressive tooling ensures consistent dimensional compliance across multimillion-unit annual production contracts.
8.2.3 EV component manufacturing
The transition to electric mobility has accelerated demand for progressive die stamped EV components. Precision dies stamp copper and aluminum battery busbars, battery cell terminal tabs, module tie rods, thermal management heat sinks, and high-voltage shielding cans.
9. Quality Systems for Progressive Die Stamping
9.1 International Quality Standards
9.1.1 ISO 9001
ISO 9001 establishes the foundational Quality Management System (QMS) for contract metal stamping facilities. It provides standardized frameworks for document control, material traceability, calibrated equipment maintenance, employee qualification, and structured continuous improvement (PDCA) cycles.
9.1.2 IATF 16949
IATF 16949 is the definitive quality management standard for automotive manufacturing. It builds upon ISO 9001 by enforcing automotive-specific protocols focused on defect prevention, supply chain variation reduction, automated error-proofing (Poka-Yoke), and complete batch traceability.
9.2 Automotive Core Tools
9.2.1 PPAP
The Production Part Approval Process (PPAP) demonstrates that the stamping line can produce parts meeting all engineering drawing requirements at production speeds. Tier suppliers typically submit Level 3 PPAP packages, including sample parts, dimensional results, material certifications, and process capability studies.
9.2.2 APQP
Advanced Product Quality Planning (APQP) provides a structured project management methodology from initial tool concept through mass production launch. Cross-functional teams evaluate engineering feasibility, track tooling build milestones, and resolve manufacturing risks early.
9.2.3 FMEA
Failure Mode and Effects Analysis (Design FMEA and Process FMEA) proactively identifies potential failure modes in die design and press operations. Tool designers implement preventive measures such as misfeed detection sensors, hardened punch inserts, and mechanical stops to mitigate high-risk failure modes.
9.2.4 Control Plan
The Control Plan details all inspection checkpoints, measuring equipment, sampling frequencies, and reaction protocols across every manufacturing phase. It governs raw coil receiving, press stamping, in-line sensor monitoring, secondary deburring, and final packaging.
9.2.5 SPC
Statistical Process Control (SPC) monitors critical feature dimensions during active stamping runs. Press operators sample parts at scheduled intervals, plotting measurements on X-bar and R control charts to maintain process capability indices of Cpk >= 1.67.
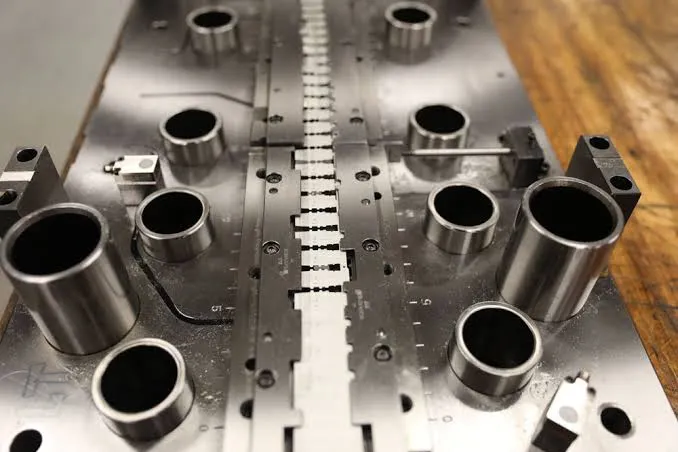
Electric vehicle battery busbars and terminals are frequently manufactured using progressive die stamping
9.2.6 MSA
Measurement Systems Analysis (MSA), including Gage Repeatability and Reproducibility (Gage R&R) studies, verifies that inspection tools and operator techniques introduce minimal measurement error. Gage R&R values maintained below 10% ensure valid dimensional inspection data.
9.3 Inspection Systems
9.3.1 CMM inspection
Coordinate Measuring Machines (CMM) located in climate-controlled quality laboratories (~ 20 °C) inspect finished production samples. High-accuracy multi-axis touch probes and laser scanners verify complex GD&T parameters, hole positions, and profile tolerances directly against 3D CAD nominals.
9.3.2 Vision inspection
High-speed optical vision systems installed directly on press ejection chutes inspect 100% of stamped components inline. Automated digital cameras verify hole presence, slot geometries, edge burr levels, and outer contours at production line speeds.
9.3.3 First Article Inspection (FAI)
Before authorizing mass production runs, quality engineers conduct a complete First Article Inspection on initial stamped components off the tool. FAI reports verify that die shut-height calibration, strip progression, and punch offsets yield fully conforming parts.
9.3.4 Traceability
Digital quality systems maintain complete lot traceability for every production batch. Laser-etched 2D DataMatrix barcodes or stamped batch numbers link finished stampings directly to raw material master coil certifications, tool maintenance history, press machine IDs, and inspection logs.
10. Progressive Die Stamping Pricing Factors
10.1 Cost Drivers
10.1.1 Tooling investment
Tooling represents the largest upfront capital expense in progressive die stamping. Complex multi-station dies integrate wire-EDM machined tool steel blocks, carbide punches, nitrogen gas springs, and in-die sensors. The number of sequential stations and dimensional tolerances directly dictate initial tool design and fabrication costs.
10.1.2 Material cost
Raw material selection establishes baseline piece-part pricing. Specialty alloys like stainless steel (SUS304) or phosphor bronze carry higher market premiums than standard commercial cold-rolled carbon steel. Strip nesting layout and carrier web design also determine the scrap percentage generated per stroke.
10.1.3 Production volume
Total order volume governs how effectively non-recurring engineering (NRE) and tooling investments amortize. Mass production runs exceeding hundreds of thousands of units distribute fixed tooling expenses across the batch, driving the per-part cost down to fractions of a dollar.
10.1.4 Press capacity
Press hourly operating rates correspond directly to machine tonnage, bed size, and mechanical sophistication. Running a high-speed, dynamic-balanced 400-ton press requires greater electrical power and facility overhead than a standard 80-ton mechanical C-frame press, influencing hourly production calculations.
10.1.5 Secondary operations
Post-stamping processing steps such as barrel deburring, electro-zinc plating, E-coating, heat treatment, and robotic hardware assembly add processing stages to the workflow. Consolidating secondary processes inside the die (such as in-die tapping or nut insertion) eliminates secondary handling expenses.
10.2 How High Volume Reduces Unit Cost
Progressive die stamping achieves exponential cost reductions as production scale increases. Initial tooling design and machining represent fixed upfront investments. Once the die is mounted and calibrated, high-speed automated presses produce finished parts at speeds ranging from 100 to 500+ strokes per minute with minimal labor intervention. This high-efficiency throughput spreads toolmaking and setup costs across millions of parts, yielding unmatched unit-cost economics compared to CNC machining or single-stage forming.
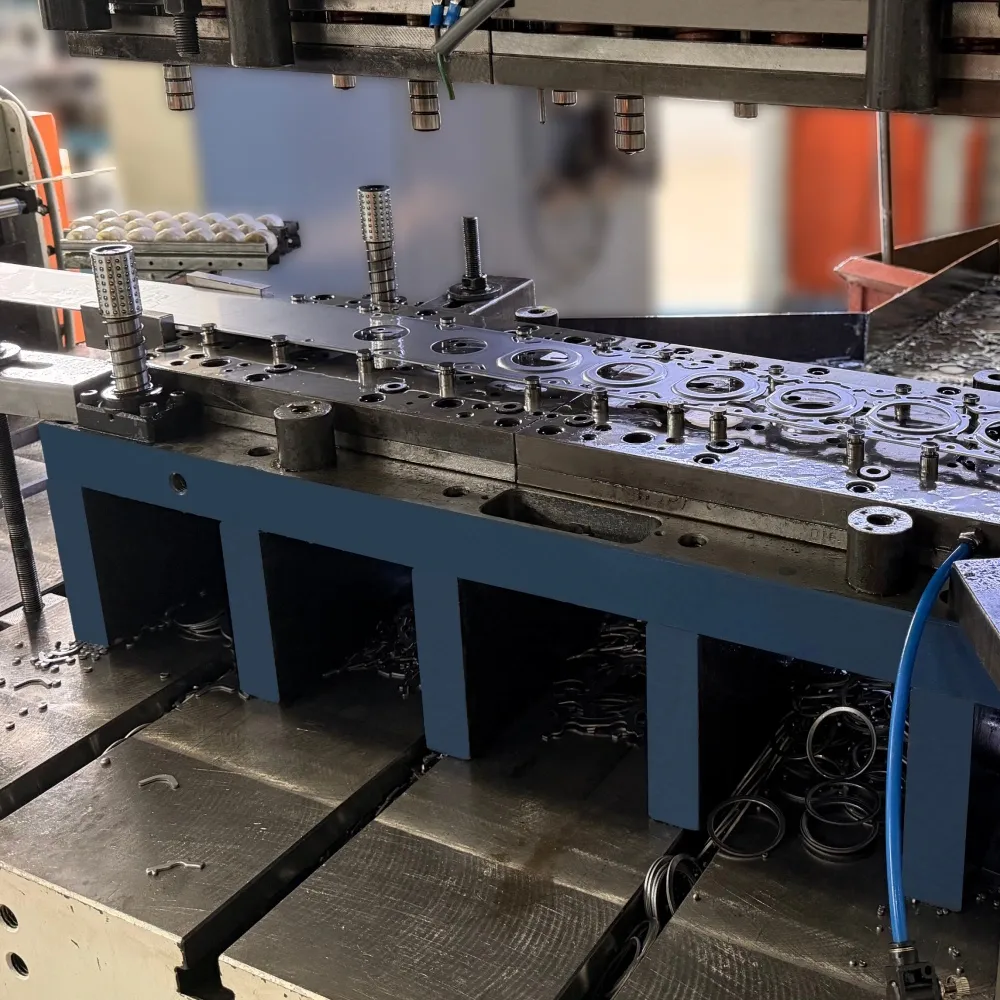
Progressive die stamping delivers exceptional dimensional repeatability across high-volume production orders
10.3 Cost Reduction Strategies for OEM Buyers
OEM buyers can optimize manufacturing expenditure by implementing several proactive strategies:
- Design for Manufacturability (DFM): Work closely with toolmakers early to standardize bend radii, increase hole-to-edge clearances, and eliminate tight dimensional callouts where not functionally critical.
- Material Strip Nesting: Re-orienting component silhouettes along the strip reduces pitch length and web carrier widths, improving material utilization rates above 80%.
- Standardized Tool Components: Specify commercial off-the-shelf die components (such as Dayton or Misumi punches, guide pins, and nitrogen cylinders) to reduce custom machining time and lower long-term replacement costs.
- Long-Term Production Forecasts: Consolidating component demand into annual rolling contracts enables suppliers to purchase raw metal coils at bulk commercial rates and schedule uninterrupted press runs.
11. How to Choose a Progressive Die Stamping Supplier
11.1 Supplier Evaluation Checklist (Featured Snippet)
11.1.1 Engineering capability
Ensure the supplier maintains an in-house engineering team proficient in 3D CAD/CAM software and finite element forming simulation. Engineers must possess the skills to calculate strip progression, springback compensation, and press tonnage distribution before metal is cut.
11.1.2 Progressive die tooling expertise
A qualified supplier must operate a dedicated toolroom equipped with high-precision CNC machining centers, precision surface grinders, and wire EDM equipment. In-house toolmaking ensures complete control over die quality, fast tryouts, and rapid die maintenance.
11.1.3 Production capacity
Evaluate the supplier’s press fleet to confirm they operate a versatile range of mechanical, hydraulic, and high-speed presses. Adequate tonnage capacity (from 40 tons to 800+ tons) ensures they can handle both delicate precision terminals and heavy structural plates.
11.1.4 Automotive certifications
For automotive supply chains, verify active IATF 16949 certification. This standard proves the supplier maintains standardized defect-prevention frameworks, automated error-proofing (Poka-Yoke), and compliance with global automotive engineering expectations.
11.1.5 Quality systems
Confirm the presence of a climate-controlled quality laboratory (~ 20 °C) equipped with Coordinate Measuring Machines (CMM), optical vision profile projectors, and surface roughness testers to ensure consistent drawing compliance across production batches.
11.1.6 Export experience
Prioritize contract manufacturers with a proven track record of shipping precision stampings to North America and Europe. Suppliers must be experienced with international B2B communication, commercial trade agreements, and protective export packaging.
11.1.7 DFM support
A dependable partner provides comprehensive Design for Manufacturability (DFM) reviews during the initial quotation stage, identifying part geometry adjustments that lower tooling complexity, prevent tearing, and reduce piece-part costs.
11.2 Questions to Ask Before Sending an RFQ
Before committing project engineering resources, procurement managers should ask prospective suppliers these critical questions:
- Do you design and fabricate progressive stamping dies in-house, or do you outsource toolmaking to third-party toolrooms?
- What are the tonnage ranges and maximum bed dimensions of your progressive stamping press fleet?
- What tool steels and PVD coatings do you specify for high-wear punch and cavity inserts?
- Are you certified to IATF 16949, and can you provide Level 3 PPAP documentation packages with full material traceability?
- What preventive die maintenance procedures do you follow, and who assumes financial responsibility for die sharpening and replacement punches?
- How do you package stamped parts to prevent rust oxidation and handling damage during transoceanic shipping?
12. Why Vietnam Is Emerging as a Progressive Die Stamping Hub
12.1 Advantages of Vietnam Manufacturing
12.1.1 Skilled workforce
Vietnam has cultivated a large talent pool of mechanical engineers, CAD/CAM programmers, toolmakers, and certified press operators. Technical universities and vocational institutions continuously supply manufacturing talent capable of executing complex progressive tool designs.
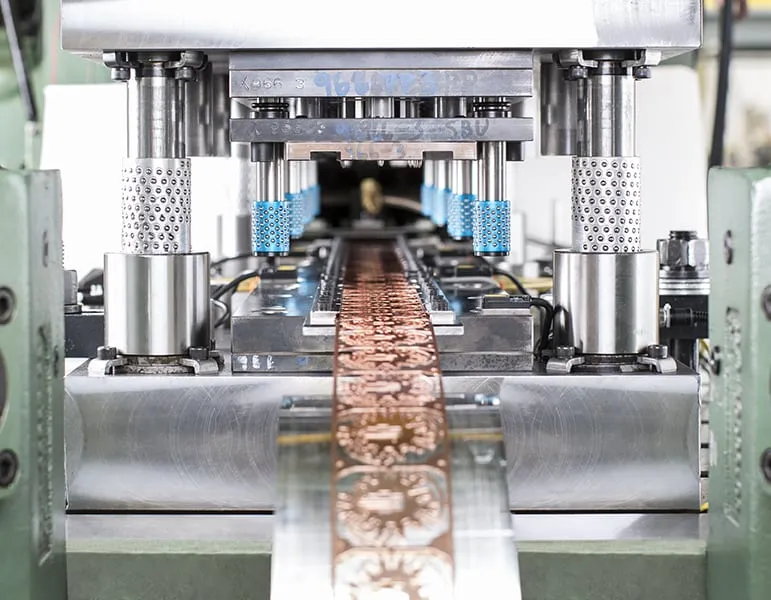
Progressive die stamping separates the finished part from the strip carrier at the final station
12.1.2 Competitive production costs
Vietnam offers a highly cost-efficient manufacturing environment. Favorable labor rates, competitive utility expenses, and lower operational overhead allow contract manufacturers to deliver high-precision stamped parts at competitive prices compared to Western or regional competitors.
12.1.3 Automotive supply chain growth
The rapid expansion of domestic and international automotive assembly operations in Vietnam has accelerated investments in tier-level component manufacturing. Local stamping suppliers increasingly support high-spec structural, interior, and electric vehicle component programs.
12.1.4 China+1 sourcing strategy
Global OEMs are actively deploying “China+1” supply chain diversification strategies to reduce trade risks, tariff burdens, and geographic concentration. Vietnam stands out as a prime destination, offering political stability, reliable business conditions, and strong industrial growth.
12.1.5 Export capability to US & Europe
Vietnam’s modern deep-water seaports (such as Lach Huyen and Cai Mep) and international airports support direct trade routes to North America and Europe. Bilateral and multilateral free trade agreements simplify customs clearances and lower import tariffs for Western buyers.
12.2 Vietnam vs China for Progressive Die Stamping
12.2.1 Manufacturing cost
While China’s labor and industrial land costs have risen steadily over the past decade, Vietnam maintains a distinct cost advantage. Contract stamping manufacturers in Vietnam deliver significant savings on both non-recurring tooling fabrication and ongoing piece-part production runs.
12.2.2 Lead time
For international buyers, tool fabrication lead times in Vietnam are competitive with Chinese toolrooms, typically averaging 6 to 10 weeks from final DFM approval to First Article Inspection. Reliable shipping schedules from Vietnamese container terminals ensure predictable logistics lead times.
12.2.3 Supply chain resilience
Diversifying progressive die stamping programs into Vietnam mitigates vulnerability to regional trade barriers, geopolitical tensions, and sudden port disruptions. Establishing redundant tooling assets in Vietnam builds long-term supply chain continuity.
12.2.4 Quality systems
Vietnamese contract manufacturing facilities operate under identical international quality management standards as top-tier global suppliers. Rigorous implementation of ISO 9001 and IATF 16949 ensures quality parity with established manufacturing hubs.
12.2.5 Logistics
Vietnam features an extensive coastline with direct access to major international maritime shipping corridors. Deep-water container ports accommodate large ocean carriers, providing efficient transit times to the United States West Coast (~ 18 to 22 days) and Western European ports.
| Strategic Metric | Progressive die metal forming in Vietnam | Progressive Stamping in China |
| Labor & Overhead Cost | Highly Competitive | Moderately High / Increasing |
| Tariff Exposure (US/EU) | Favorable / Low Trade Barriers | Elevated Trade Tariffs & Restrictions |
| Supply Chain Strategy | Preferred “China+1” Destination | Traditional Manufacturing Base |
| Toolmaking Capability | Rapidly Expanding & Advanced | Mature & Comprehensive |
| Quality Management | IATF 16949 / ISO 9001 Aligned | IATF 16949 / ISO 9001 Aligned |
13. Trusted Progressive Die Stamping Supplier in Vietnam – Automech
13.1 Progressive Die Stamping Capabilities
13.1.1 Progressive die tooling
Founded in 2020, Automech (Automech Mechanical Equipment and Solutions Joint Stock Company) provides comprehensive tool and die engineering services. Operating modern toolrooms equipped with high-precision wire EDM machinery, CNC machining centers, and surface grinders, Automech designs and fabricates custom progressive dies that deliver extended tool life and micron-level accuracy.
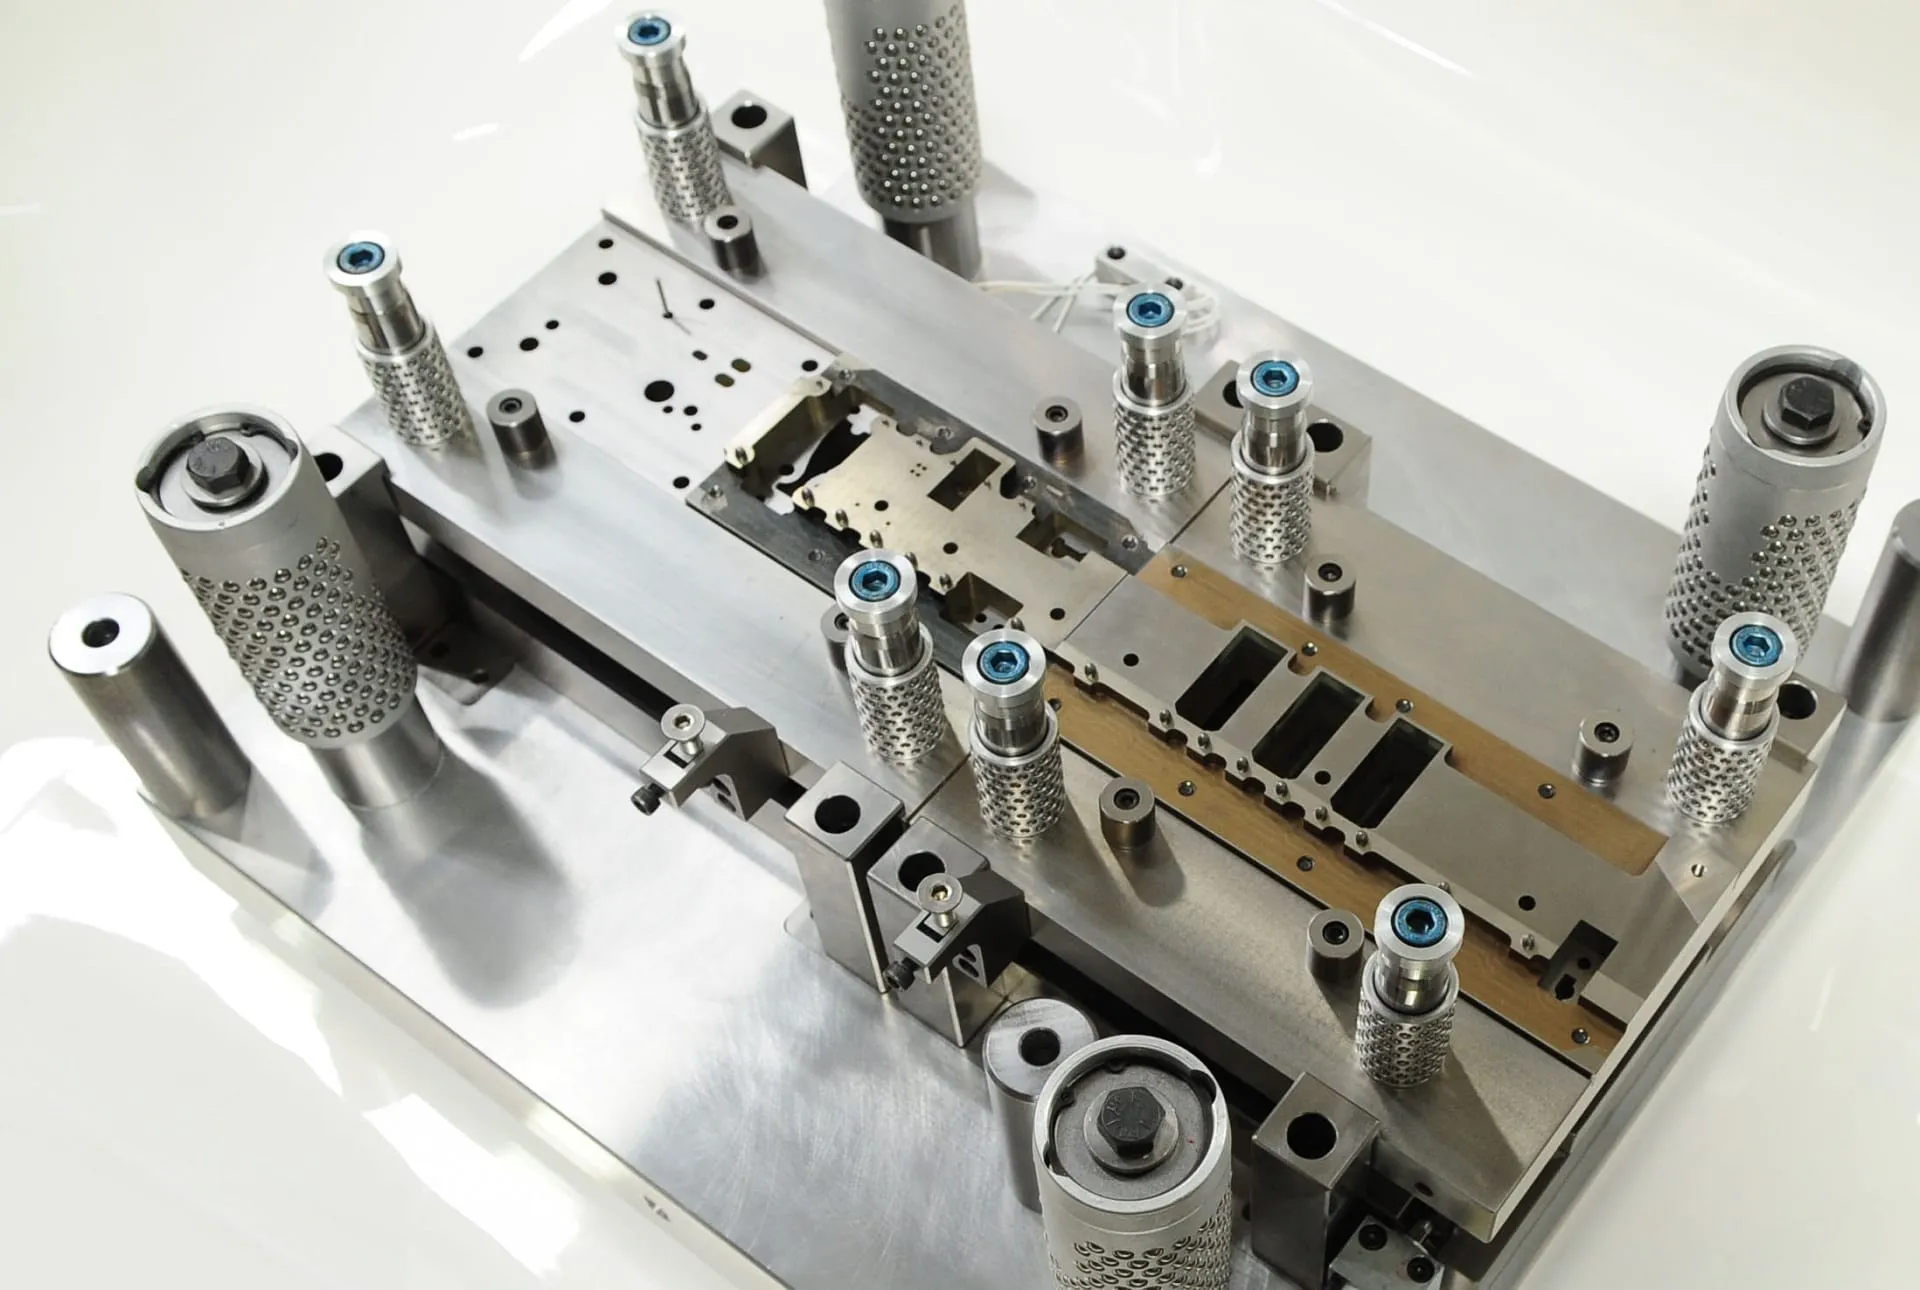
High initial tooling costs for progressive die stamping amortize effectively over mass production runs
13.1.2 High-volume precision stamping
Automech operates automated progressive press lines designed for continuous, high-speed component manufacturing. The company’s automated coil-feeding systems process diverse metal alloys into precision parts while maintaining tight tolerances across high-volume production schedules.
13.1.3 OEM component manufacturing
Automech manufactures custom sheet metal stampings tailored to OEM technical drawings and strict GD&T specifications. The company manages complete component lifecycles from initial DFM reviews and tool design through trial sampling, full-scale mass production, and final packaging.
13.1.4 Automotive stamping expertise
Automech specializes in manufacturing automotive body-in-white (BIW) reinforcements, chassis brackets, interior seat hardware, and electric vehicle (EV) battery enclosures. Its production facilities integrate automated sensor monitors to ensure zero-defect output for vehicle applications.
13.2 Engineering & Manufacturing Support
13.2.1 DFM review
Automech’s engineering and R&D team provides proactive Design for Manufacturability (DFM) reviews prior to steel cutting. Engineers analyze bend radii, piercing clearances, and forming sequences to optimize tool geometry, reduce material scrap, and lower piece-part costs.
13.2.2 Tooling feasibility analysis
Using advanced computer-aided forming simulation, Automech evaluates strip stretch limits, material springback characteristics, and press tonnage distribution. This simulation approach eliminates design flaws before die hardening, ensuring predictable tool performance during initial tryouts.
13.2.3 Prototype to mass production
Automech supports every phase of product development. Factory 1 in Bac Ninh (10,500 m²) handles custom tooling, jigs, and pilot trial stamping, while Factory 2 (10,000 m², inaugurated June 2026) provides dedicated high-volume mass production targeting an 80% automation rate.
13.2.4 Welding & assembly integration
Automech provides turnkey assembly integration, merging progressive stampings with secondary operations. The company combines automated tandem stamping lines (800 to 1,300 tons with ABB robots) with robotic welding cells (KUKA robots and Fronius welding systems) for complex automotive sub-assemblies.
13.3 Quality Assurance
13.3.1 CMM inspection
Automech operates climate-controlled quality laboratories (~ 20 °C) equipped with high-precision Coordinate Measuring Machines (CMM) and optical profile projectors. Multi-axis tactile probing verifies critical hole centers, true positions, and complex surface contours against 3D CAD models.
13.3.2 PPAP documentation
To meet strict automotive procurement requirements, Automech submits complete Production Part Approval Process (PPAP) packages up to Level 3. Documentation includes dimensional measurement results, material test reports (MTR), process flow diagrams, PFMEA logs, and control plans.
13.3.3 Traceability
Automech maintains complete batch traceability across all production runs. Finished parts and shipment containers feature traceable lot labels and laser-etched DataMatrix codes linking every component to its raw coil heat number, press operator shift, and die maintenance log.
13.3.4 Export quality management
Automech implements quality controls tailored to international export projects. Components undergo vibratory deburring, ultrasonic cleaning, and corrosion-inhibiting VCI packaging to guarantee parts arrive at overseas destinations in pristine condition.
13.4 Why Global OEMs Partner with Automech
13.4.1 Automotive manufacturing experience
Automech has proven manufacturing capabilities through major projects delivered to leading domestic and multinational corporations, including VinFast, VinES, Hoa Phat, Kim Long Motors, and Seojin. Its production teams understand OEM standards and delivery schedules.
13.4.2 Export projects for US & Europe
Automech’s engineering and project management teams possess extensive experience collaborating with international buyers across North America and Europe. They adhere to international technical standards and maintain transparent engineering communication.

Automotive safety reinforcements and seatbelt latch plates rely on precision progressive die stamping
13.4.3 Reliable delivery
With nationwide service hubs covering Hanoi, Bac Ninh, Hai Phong, Da Nang, Hue, and Southern Vietnam, alongside close proximity to major deep-water seaports, Automech ensures reliable supply continuity and on-time shipment delivery.
13.4.4 Cost optimization support
Automech combines in-house progressive toolmaking, advanced press automation, and competitive Vietnamese operational advantages. This integrated approach allows global OEMs to optimize capital investments while securing dependable manufacturing capacity.
14. RFQ Process for Progressive Die Stamping
14.1 Information Required for an RFQ
14.1.1 CAD drawings
A complete Request for Quotation (RFQ) requires fully defined 3D CAD files (STEP, IGES) along with 2D engineering drawings (PDF) detailing critical dimensions, bend angles, thread specifications, and geometric dimensioning and tolerancing (GD&T) datums.
14.1.2 Material specifications
Specify exact metal grades according to standard international designations (such as ASTM, EN, or JIS), required temper/hardness conditions, and sheet metal gauge thickness including allowable coil thickness variations.
14.1.3 Annual volume
Disclose projected annual usage (EAU) alongside expected order batch sizes and pilot prototype requirements. Stating production volume allows toolmakers to design the optimal die architecture (such as single-out vs multi-cavity dies) for cost-efficient production.
14.1.4 Tolerance requirements
Identify functional mating interfaces and critical assembly dimensions versus non-critical exterior features. Clearly defined tolerances avoid over-specifying non-functional dimensions, keeping tooling costs manageable.
14.1.5 Quality documentation
Outline required quality compliance deliverables upfront. Specify whether the project mandates Level 3 PPAP submissions, first article inspection reports, raw material mill test certificates (MTR), or specific coating thickness test data.
14.2 Engineering Review Process
Upon receiving an RFQ package, the engineering team evaluates component manufacturability using forming simulation software. The review analyzes sheet stretch limits, punch cutting clearances, station pitches, and springback behavior. The team then formulates a detailed strip progression proposal, calculates press tonnage requirements, and prepares a transparent cost breakdown covering die design, tooling build, and piece-part pricing.
14.3 Tooling Development Timeline
Progressive die development typically spans 6 to 10 weeks, structured across clear project milestones:
- Weeks 1 to 2: 3D strip progression modeling, DFM sign-off, and customer tool design freeze.
- Weeks 3 to 6: Raw tool steel procurement, vacuum heat treatment, CNC milling, and high-precision wire EDM machining of die inserts.
- Weeks 7 to 8: Tool assembly, fitting, guide pillar alignment, and installation of nitrogen gas springs.
- Weeks 9 to 10: Initial press tryouts, strip development fine-tuning, sample part stamping, and CMM First Article Inspection.
14.4 Sample Approval & Mass Production
Following successful tool tryouts, the supplier submits initial sample parts along with full FAI dimensional reports and material test certificates for customer approval. Once the customer validates the samples and signs off on the PPAP submission, the progressive die enters mass production. The press line is then scheduled for automated, high-speed stamping under strict Statistical Process Control (SPC) monitoring.
15. Frequently Asked Questions (People Also Ask)
15.1 What is progressive die stamping?
Progressive die stamping is an automated, high-speed sheet metal forming process that advances a continuous coil strip through a series of sequential stations mounted within a single die block. Each station executes specific operations (such as piercing, coining, bending, and cutting) with each press stroke, completing a finished component at the final cutoff station.
15.2 How does progressive die stamping work?
An automated servo feeder advances raw sheet metal coil into the press bed. As the press cycles downward, punches shear and shape the metal across successive inline stations while the workpiece remains attached to a carrier strip. At the final station, the finished component is severed from the carrier ribbon and ejected automatically.
15.3 What are the advantages of progressive die stamping?
The primary advantages include high production speeds (100 to 500+ parts per minute), low unit manufacturing costs at scale, tight dimensional repeatability, reduced labor requirements, and optimized raw material utilization through computer-modeled strip nesting.
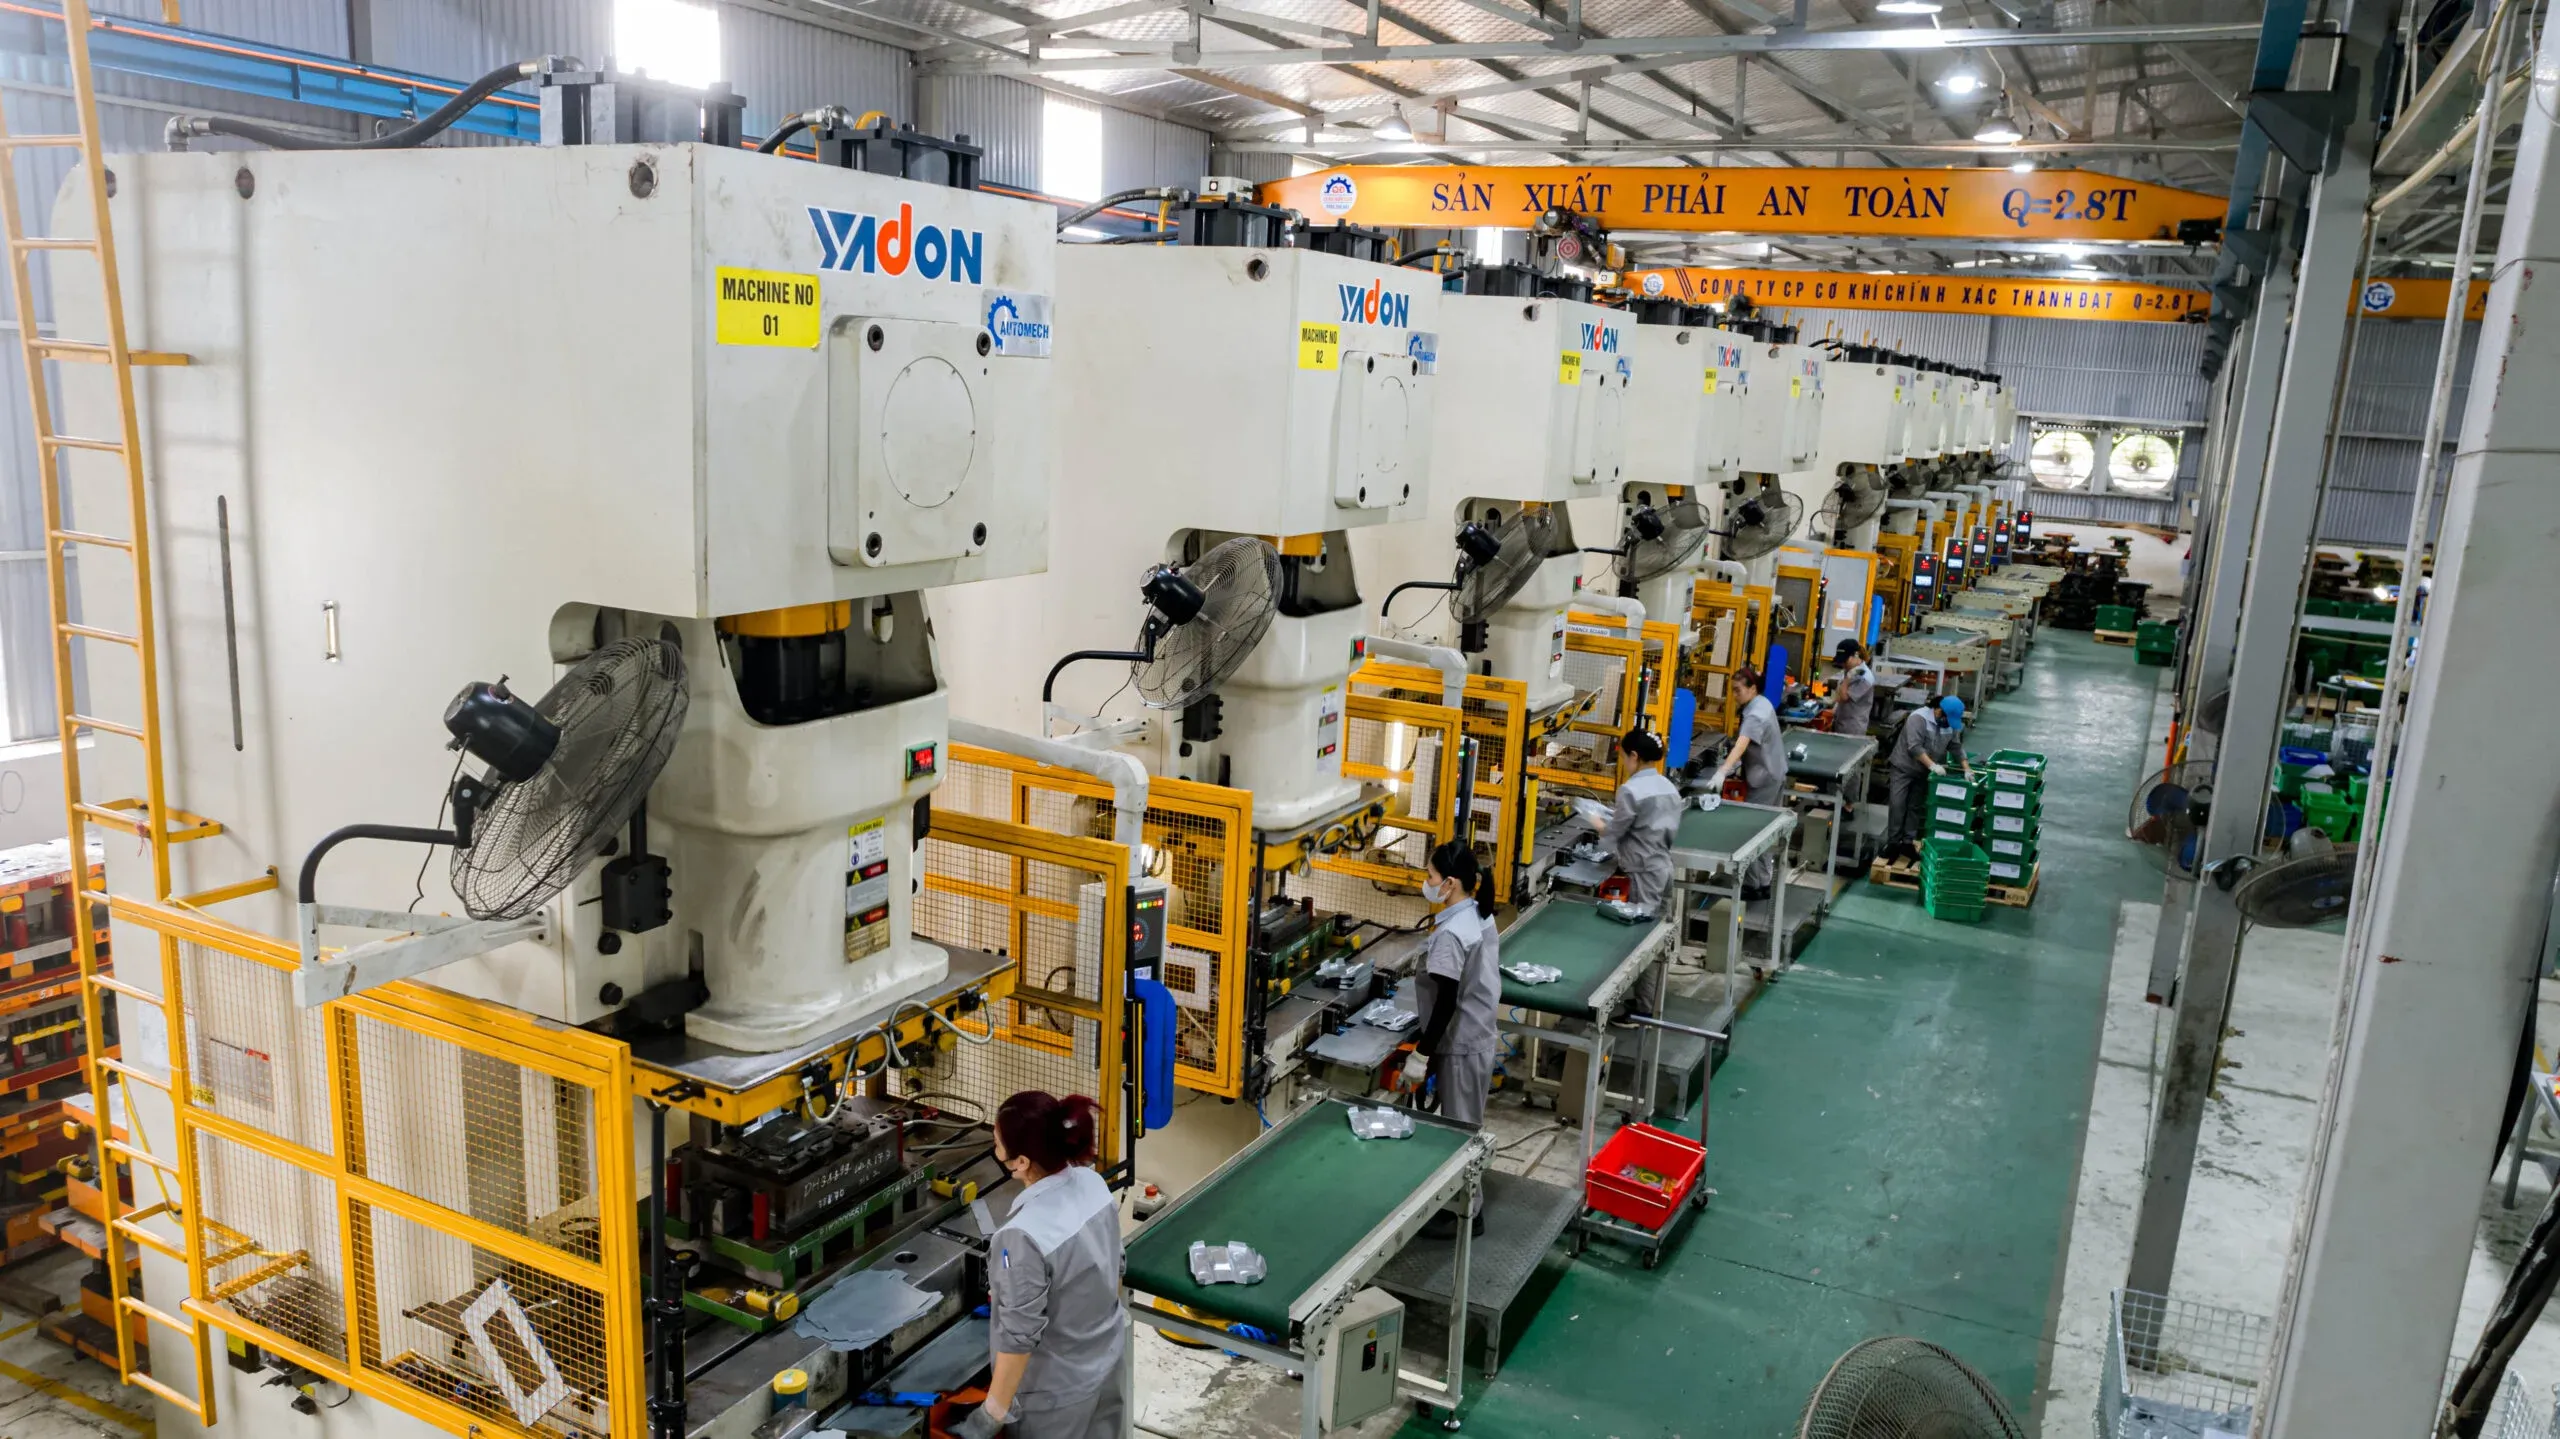
Progressive die stamping integrates piercing, coining, and flanging operations within a single press stroke
15.4 What materials are suitable for progressive die stamping?
Progressive die stamping processes a wide variety of ductile metals, including cold-rolled low-carbon steel, High-Strength Low-Alloy (HSLA) steel, advanced high-strength steel (AHSS), austenitic and ferritic stainless steel, aluminum alloys (such as 5052 and 6061-T4), copper, and brass.
15.5 What industries use progressive die stamping?
Key industries include automotive manufacturing (brackets, seat hardware, BIW reinforcements), consumer electronics (lead frames, shielding cans, connector pins), home appliances, industrial machinery, telecommunications, and aerospace hardware.
15.6 How do I choose a progressive die stamping supplier?
Select a supplier based on in-house tool and die design capabilities, wire EDM toolroom assets, adequate press tonnage range (40T to 800T+), active IATF 16949 certification, climate-controlled CMM quality inspection, and proven experience in export logistics and packaging.
15.7 How do I request a progressive die stamping RFQ?
To request an accurate quotation, submit your 3D CAD files (STEP/IGES) and 2D engineering drawings (PDF) detailing critical tolerances, material specifications, required surface finishing, annual volume forecasts, and quality documentation requirements.
16. Featured Snippet Opportunities
16.1 Definition Snippet
16.1.1 What is progressive die stamping?
Progressive die stamping is an automated, high-speed sheet metal forming process that advances coiled strip through sequential cutting, punching, bending, and forming stations mounted within a single die block. Guided by mechanical or servo presses, the system performs distinct operations at each station with every press stroke, separating the completed component at the final cutoff station.
16.2 Process Snippet
16.2.1 Progressive die stamping process steps
The progressive die stamping manufacturing workflow follows five synchronized phases:
- Coil Uncoiling & Straightening: Raw metal strip unrolls from an uncoiler, passes through precision leveler rolls to remove coil curvature, and enters the press bed.
- Servo Strip Feeding: A high-speed servo feeder indexes the strip forward with micro-pitch accuracy (within ±0.01 mm), where hardened pilot pins engage guide holes to lock positioning.
- Multi-Station Piercing & Shearing: Punches pierce internal holes, cut perimeter relief notches, and form carrier ribbons that carry the part along the strip.
- Forming & Bending: Tool stations execute compound bending, coining, embossing, or flanging operations, applying built-in springback compensation to hold tight tolerances.
- Cutoff & Automated Ejection: The final station severs the component from the carrier web, ejecting finished parts onto automated conveyors while chopping the scrap skeleton.
16.3 Comparison Table
16.3.1 Progressive die stamping vs Transfer stamping
| Feature | Progressive Die Stamping | Transfer Stamping |
| Strip / Blank State | Continuous strip carrier ribbon | Individual pre-cut blanks |
| Part Movement | Strip pulled/pushed through die stations | Mechanical grippers or transfer rails |
| Production Speed | 100 to 500+ parts per minute | 15 to 40 parts per minute |
| Maximum Part Size | Small to medium structural components | Large body panels and deep housings |
| Material Scrap Rate | Higher (Carrier ribbon scrap skeleton) | Lower (Optimized blank nesting) |
| Initial Tooling Cost | High (Integrated multi-station die block) | High (Multiple die sets + transfer tooling) |
| Target Annual Volume | > 50,000 units | 20,000 to 100,000+ units |
16.3.2 Progressive die stamping vs CNC machining
| Performance Metric | Progressive Die Stamping | CNC Machining |
| Manufacturing Principle | Cold deformation and die shearing | Subtractive cutting via rotary cutters |
| Production Cycle Time | < 1 second per finished part | Minutes to hours per part |
| Unit Cost at High Volume | Extremely low | Moderate to high |
| Tooling Investment | High dedicated die investment | Minimal (Standard cutters and soft jaws) |
| Material Utilization | High (Formed from flat sheet) | Low (Substantial chip generation) |
| Dimensional Accuracy | ±0.01 mm to ±0.02 mm | ±0.002 mm to ±0.005 mm |
| Optimal Production Run | Mass production (> 50,000 units) | Prototypes and low volume (< 1,000 units) |
16.4 List Snippet
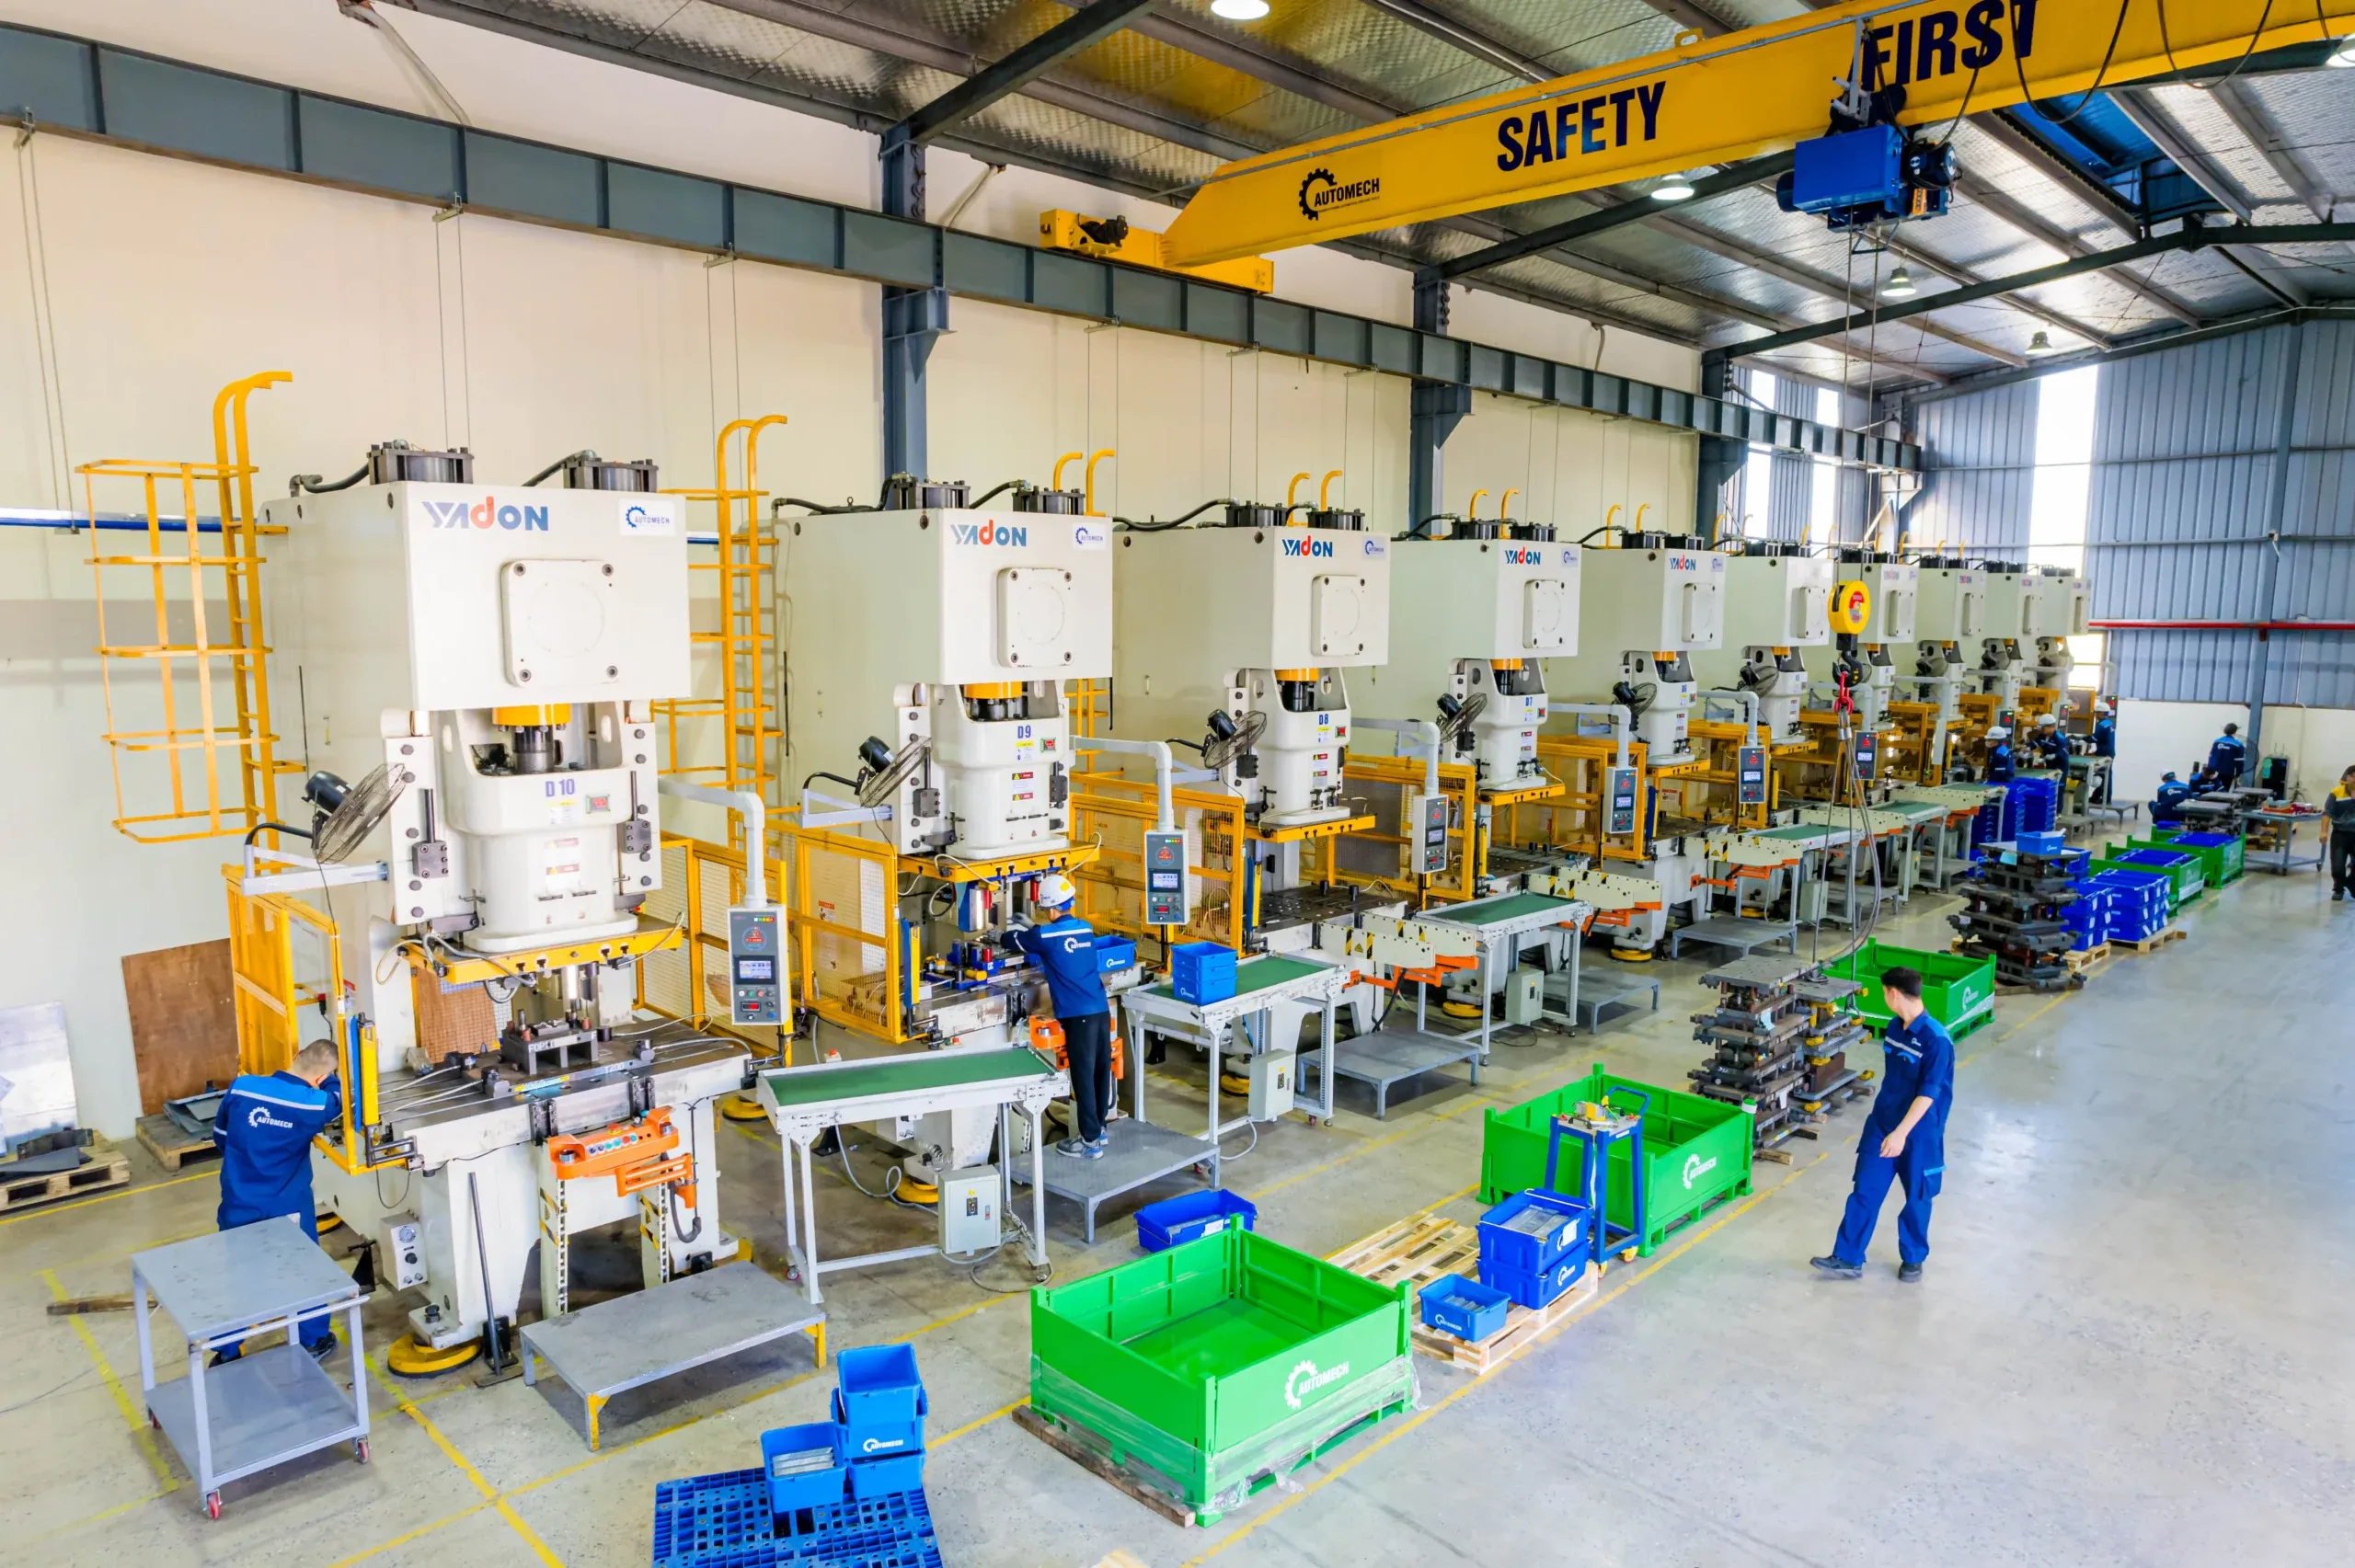
Manufacturers select progressive die stamping for sheet metal parts exceeding fifty thousand units annually
16.4.1 Top advantages of progressive die stamping
- Maximum Production Throughput: Operates at 100 to 500+ strokes per minute, producing high volumes with minimal cycle time.
- Minimal Per-Part Manufacturing Cost: Spreads non-recurring engineering and die fabrication costs over large runs to lower piece-part rates.
- Exceptional Batch Repeatability: Anchoring the workpiece to the strip eliminates manual transfer errors, holding tight dimensional tolerances.
- Optimized Material Utilization: Computer-modeled CAD nesting maximizes strip layout efficiency, keeping scrap generation low.
- Integrated Secondary Processes: Performs in-die tapping, coining, countersinking, and hardware insertion directly inside the press tool to eliminate downstream handling.
16.5 Supplier Checklist Snippet
16.5.1 How to choose a progressive die stamping supplier
When selecting an automotive or industrial progressive die stamping partner, procurement teams should evaluate several core manufacturing competencies. A qualified supplier must operate a versatile press fleet ranging from 40 to 800+ tons equipped with automated coil lines, supported by an in-house toolroom with wire EDM, CNC machining centers, and precision surface grinders for die fabrication and maintenance. In addition, the manufacturer should hold active IATF 16949 and ISO 9001 certifications, implement strict quality control through climate-controlled CMM inspection, in-line vision sensing, and comprehensive Level 3 PPAP documentation. Finally, buyers need to verify upfront engineering DFM support with strip forming simulations, alongside proven export readiness that includes anti-corrosion VCI packaging and reliable international logistics coordination.
Automech Mechanical Equipment and Solutions Joint Stock Company
Head Office: No. 285 Phuc Loi Street, Phuc Loi Ward, Hanoi City
Da Nang Branch: No. 20 Nguyen Sinh Sac Street, Hoa Khanh Ward, Da Nang City
Ho Chi Minh Branch: No. 84, Street No. 10, Van Phuc Urban Area, Hiep Binh Ward, Ho Chi Minh City
Factory No. 1: Automech Automation Equipment, Mold & Tool Manufacturing Factory – Automech Demo Center: Dinh Tram Industrial Park, Nenh Ward, Bac Ninh City, Vietnam
Factory No. 2: Automech Parts Manufacturing & Component Fabrication Factory: Viet Nhat Industrial Cluster, Xuan Cam Commune, Bac Ninh City, Vietnam
Hotline: 0987 899 347
Website: https://automechmfg.com/
Fanpage: https://www.facebook.com/automech.mfg/
YouTube: https://www.youtube.com/@Automechmfg