Sheet metal stamping is a cornerstone of modern industrial manufacturing, converting flat metal sheets and continuous coils into complex, durable components. Through high-tonnage mechanical, hydraulic, or servo press systems equipped with custom-engineered dies, manufacturers execute shearing, bending, forming, and deep drawing operations with rapid cycle times. Global OEMs and Tier suppliers rely on sheet metal stamping to achieve tight dimensional tolerances, high structural rigidity, and exceptional batch-to-batch repeatability for automotive, industrial machinery, electronics, and energy applications.
1. Sheet Metal Stamping Overview
1.1 What is sheet metal stamping?
1.1.1 Definition of sheet metal stamping
Sheet metal stamping is a cold-forming manufacturing process that applies high mechanical force to shape, shear, or draw flat sheet metal stock using dedicated die tooling. Guided by mechanical or hydraulic presses, the process converts raw sheet metal into precise three-dimensional geometries without melting the base material.
1.1.2 Role in metal part manufacturing
Stamping serves as a high-speed production engine across modern supply chains. By producing finished or semi-finished components in single or continuous multi-stage press strokes, it provides high production throughput, low unit costs, and minimal material waste compared to alternative metalworking methods.
1.1.3 Difference between sheet metal stamping and general metal forming
While general metal forming encompasses broad hot and cold techniques such as heavy forging, roll forming, and tube extrusion – sheet metal stamping specifically targets thin-to-medium gauge flat metal stock (typically 0.1 mm to 6.0 mm). Stamping utilizes closed-die sets to achieve tight geometric profiles and sharp edge features in rapid cycles.
1.2 Why global buyers use sheet metal stamping
1.2.1 Cost-efficient production for metal parts
Once die tooling is fabricated and validated, stamping delivers one of the lowest per-piece manufacturing costs in the metalworking industry. High press speeds, automated coil feeding, and optimized material nesting minimize labor overhead and raw material scrap.
1.2.2 High repeatability for OEM components
Precision tool steels and rigid press alignments ensure that every stamped part matches engineering specifications consistently. Micron-level repeatability prevents assembly line misalignments in complex OEM multi-component systems.
1.2.3 Scalability from prototype to mass production
Stamping frameworks support the complete product lifecycle. Manufacturers utilize soft tooling or modular single-stage dies for initial prototype validation before scaling seamlessly into hardened progressive or transfer dies for mass production volumes exceeding hundreds of thousands of units annually.
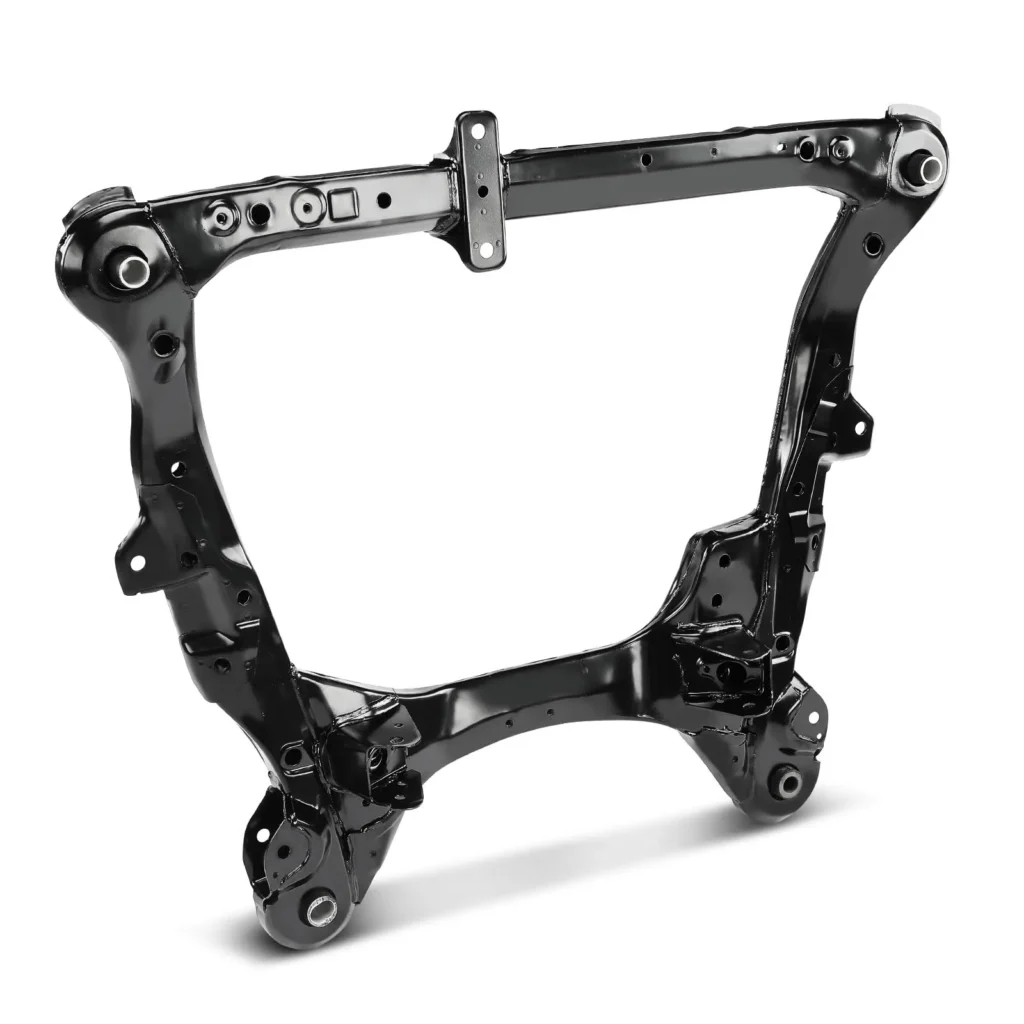
Sheet metal stamping converts flat coils into durable structural components for modern automotive vehicles
1.3 Sheet metal stamping in global manufacturing
1.3.1 Automotive and industrial applications
Automotive manufacturing represents the largest consumer of stamped sheet metal, utilizing stampings for body-in-white (BIW) structures, chassis gussets, and electric vehicle (EV) battery enclosures. Industrial sectors utilize stamped components for heavy equipment frames, HVAC enclosures, and electrical distribution cabinets.
1.3.2 Vietnam as an emerging stamping supplier base
Vietnam has expanded its manufacturing capabilities with modern press infrastructure, automated robotic integration, and advanced toolrooms. Suppliers like Automech provide global buyers with high-precision stamping and integrated welding assemblies backed by extensive local engineering expertise.
1.3.3 China+1 sourcing demand from US/EU buyers
International OEMs across the United States and Europe actively pursue “China+1” supply chain diversification strategies to mitigate geopolitical risks and tariff pressures. Vietnam provides a stable manufacturing environment, competitive operational costs, and established export logistics routes to Western markets.
2. How Sheet Metal Stamping Works
2.1 Basic sheet metal stamping principle
2.1.1 Pressing sheet metal into a desired shape using dies
At its core, sheet metal stamping relies on matching male punches and female die cavities. When placed between these hardened tooling elements, flat sheet metal yields plastically under extreme compressive and shear loads, permanently adopting the contours of the die cavity.
2.1.2 Using mechanical or hydraulic presses
Mechanical presses utilize flywheel mechanisms to deliver rapid, high-impact force ideal for high-speed blanking and piercing. Hydraulic presses provide steady, controllable tonnage throughout the full stroke length, making them preferred for deep drawing and heavy-gauge forming operations.
2.1.3 Controlling shape, tolerance, and repeatability
Maintaining tight tolerances requires precise control over press shut height, punch-to-die clearances, and strip guiding systems. In-die nitrogen gas springs and precision guide bushings absorb lateral forces, ensuring repeatable dimensional conformity across long production runs.
2.2 Main production workflow
2.2.1 Technical drawing review
Engineering teams analyze customer 2D drawings and 3D CAD models to assess material stretch limits, bend radii, hole clearances, and geometric dimensioning and tolerancing (GD&T) feasibility.
2.2.2 Material selection and blank preparation
Raw material coils or sheets are selected based on specified thickness, tensile strength, and temper. Coils pass through motorized decoilers and multi-roll levelers to eliminate coil set and residual curvature prior to press entry.
2.2.3 Tooling design and die setup
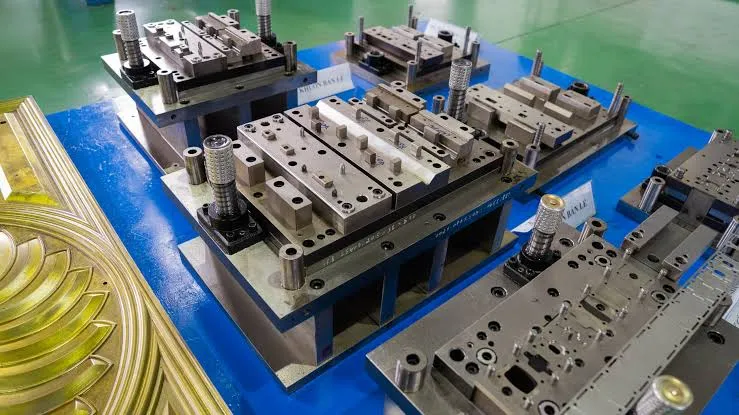
Toolmakers construct high-precision stamping dies using CNC milling, surface grinding, and wire EDM technology. Technicians then mount, align, and clamp the die sets onto the press bolster plate and slide ram.
2.2.4 Trial stamping and production validation
Initial tryout stampings undergo complete First Article Inspection (FAI) and Coordinate Measuring Machine (CMM) dimensional verification. Toolmakers fine-tune clearances and springback compensation geometry before approving mass production.
2.2.5 Mass production and inspection
Automated servo feeders advance sheet material into the stamping press at programmed speeds. In-line vision systems, acoustic sensors, and periodic statistical process control (SPC) checks ensure uninterrupted, zero-defect output.
2.3 Key production factors
Precision sheet metal stamping produces mounting brackets and chassis components with tight tolerances
2.3.1 Material thickness
Sheet thickness directly determines the required press tonnage, tool clearances, and minimum bend radii. Thicker materials demand robust tool steels and larger cutting clearances to prevent premature punch chipping.
2.3.2 Part geometry
Complex features such as deep recesses, narrow web sections, and close-proximity holes influence the number of forming stations needed. Complex geometries require progressive or transfer die architectures to prevent tearing.
2.3.3 Tooling accuracy
The dimensional precision of internal die components directly dictates finished part quality. Die components machined to tolerances within ± 0.005 mm ensure consistent edge quality and tight drawing tolerances over hundreds of thousands of cycles.
2.3.4 Press tonnage
Calculating correct press tonnage prevents machine overloading and structural die deflection. Total tonnage requirements combine the forces needed for blanking, piercing, stripping, and forming, incorporating a 20% to 30% safety margin.
3. Sheet Metal Stamping Process
3.1 Design and engineering review
3.1.1 CAD and technical drawing analysis
The engineering phase starts by importing 3D CAD files (STEP, IGES) into specialized stamping simulation software. Engineers evaluate hole-to-edge ratios, draw depths, and wall draft angles to identify potential manufacturing bottlenecks.
3.1.2 DFM review for stamping feasibility
Design for Manufacturability (DFM) reviews optimize part designs for press production. Engineers recommend standardizing bend radii, modifying slot orientations, and optimizing blank geometry to minimize die complexity and tooling cost.
3.1.3 Tolerance and material requirement review
Designers review functional mating surfaces and non-critical profiles. Establishing achievable tolerance bands prevents unnecessary secondary machining operations and ensures cost-effective production.
3.2 Tooling and die preparation
3.2.1 Stamping die design
Tool designers model multi-station strip layouts, calculating precise station pitches, carrier ribbon widths, and punch distributions to ensure balanced press loads throughout the stroke cycle.
3.2.2 Die manufacturing and validation
Toolrooms machine die shoes, punch plates, strippers, and die inserts from premium tool steels (D2, SKD11, DC53). Components undergo vacuum heat treatment to achieve hardness levels of 58 to 62 HRC prior to final precision grinding.
3.2.3 Tooling maintenance planning
A structured preventive maintenance schedule is established during tool design. Quick-change modular inserts and accessible sharpening zones allow toolmakers to regrind cutting edges with minimal press downtime.
3.3 Production process
3.3.1 Material feeding
Automated servo roll feeders advance the sheet metal strip into the die set with high indexing accuracy (± 0.02 mm). Pilot pins engage pre-punched locating holes at each station to align the strip before forming.
3.3.2 Blanking, bending, forming, or drawing
As the press cycles, synchronized punches perform cutting, embossing, flange bending, and drawing operations simultaneously across successive stations to transform the flat strip into finished components.
High speed sheet metal stamping reduces unit costs across mass industrial manufacturing runs
3.3.3 In-process inspection
Operators conduct scheduled dimensional measurements using custom check fixtures, drop indicators, and go/no-go plug gauges to monitor feature drift and detect punch wear early.
3.3.4 Final inspection and packaging
Finished stampings undergo final dimensional verification via CMM, surface finish testing, and automated optical deburr checks. Parts are then cleaned, count-verified, and packed in Vapor Corrosion Inhibitor (VCI) bags or custom returnable dunnage.
4. Types of Sheet Metal Stamping Operations
4.1 Blanking
4.1.1 Cutting flat blanks from sheet metal
Blanking is a shearing operation that cuts a predetermined flat workpiece profile out of a larger sheet or continuous coil. The sheared piece constitutes the primary workpiece for subsequent stamping and forming stages.
4.1.2 Preparing parts for further forming operations
Accurate blank geometry is critical for secondary forming steps. Controlled punch-to-die clearances ensure uniform blank perimeters, preventing uneven material draw, wrinkling, or split edges during subsequent deep drawing or bending.
4.2 Piercing
4.2.1 Creating holes or openings in sheet metal
Piercing (or punching) cuts holes, slots, or custom openings into sheet metal while the surrounding material remains intact. Unlike blanking, the punched-out slugs represent scrap and are evacuated downward through the lower die bed.
4.2.2 Maintaining burr and edge quality control
Maintaining tight punch-to-die clearances (typically 5% to 10% of material thickness) ensures clean shear zones and minimizes rollover. Regular punch maintenance prevents burr formation, ensuring clean hole tolerances for downstream fastener assembly.
4.3 Bending
4.3.1 Forming angles and flanges
Bending deforms flat sheet metal plastically along a straight axis to create V-shapes, U-channels, or edge flanges. Precision press brakes and dedicated bending dies apply localized bending moments to establish exact geometric angles.
4.3.2 Managing springback and dimensional accuracy
When bending pressure is released, metals naturally exhibit elastic recovery (springback). Tool designers compensate for this behavior by incorporating calculated over-bend angles or coin-bottoming features into the die design.
4.4 Forming
4.4.1 Creating complex stamped shapes
Forming deforms sheet metal along curved or multi-axis contours without intentionally shearing the material. This operation creates structural stiffening ribs, decorative louvers, stepped offsets, and embossed identification markings.
4.4.2 Controlling material deformation
Forming operations require precise control over blankholder clamping pressure to prevent localized material necking or wrinkling. Controlled metal stretching ensures uniform wall thicknesses across complex 3D profiles.
4.5 Drawing and deep drawing
4.5.1 Producing deeper formed parts
Drawing forces flat sheet metal into a hollow die cavity using a mechanical punch. When the depth of the resulting recess exceeds its width or diameter, the process is classified as deep drawing, producing seamless cups, cans, and shells.
4.5.2 Managing material thinning and cracking risk
Deep drawing subjects metal to severe tensile and compressive stress. Utilizing draw beads, multi-stage reduction steps, and high-performance drawing lubricants controls material flow into the die, preventing side-wall tearing and bottom cracking.
4.6 Progressive die stamping
Automotive body production utilizes sheet metal stamping to fabricate durable floor crossmembers
4.6.1 Multi-step stamping through continuous die stations
Progressive die stamping feeds a continuous coil strip through a series of sequential stations inside a single die shoe. Each press stroke performs distinct operations (piercing, bending, forming) as the strip advances incrementally.
4.6.2 Suitable for high-volume sheet metal parts
Finished components are separated from the carrier ribbon at the final cutoff station. Running at high speeds (100 to 500+ strokes per minute), progressive stamping delivers scalable manufacturing economics for large production runs.
4.7 Transfer stamping
4.7.1 Moving parts between multiple stamping stations
Transfer stamping processes pre-cut discrete metal blanks. Mechanical transfer fingers or multi-axis robotic transfer systems mechanically grip and advance the individual workpieces across separate die stations.
4.7.2 Suitable for larger or more complex parts
Because workpieces are freed from a continuous strip carrier immediately, transfer stamping accommodates large structural panels, deep oil pans, and heavy-gauge automotive subframes that cannot be processed in progressive dies.
5. Sheet Metal Stamping vs Metal Stamping
5.1 Scope of sheet metal stamping
5.1.1 Focus on sheet-based materials
Sheet metal stamping focuses specifically on processing flat coiled metal or pre-cut sheet stock with uniform thickness (typically 0.1 mm to 6.0 mm). Tooling configurations are engineered around planar material deformation mechanics, including controlled shear clearances, bend radius ratios, and draw depths tailored to sheet stock behavior.
5.1.2 Common use in brackets, panels, covers, and structural parts
Because sheet metal stamping optimizes flat raw stock, it serves as the primary method for producing mounting brackets, chassis reinforcements, outer panels, and equipment covers. The process converts flat profiles into rigid, load-bearing 3D assemblies through rapid bending and flanging operations.
5.2 Scope of metal stamping
5.2.1 Broader category covering different metal stamping methods
Metal stamping represents an umbrella manufacturing category encompassing all press-working operations that shape metal workpieces using matched die sets. It covers thin foil precision stamping, heavy plate stamping up to 20 mm thick, wire forming, and hybrid forging-stamping operations.
5.2.2 Includes sheet stamping, progressive stamping, and deep drawing
Under the broader metal stamping classification, specialized sub-processes address distinct part geometries. Progressive die stamping handles continuous multi-operation high-speed production, deep drawing forms seamless hollow cylinders and boxes, and transfer stamping manages heavy discrete components.
5.3 When to use sheet metal stamping
5.3.1 Thin to medium sheet metal components
Sheet metal stamping is the preferred choice when manufacturing components with consistent cross-sectional wall thickness between 0.5 mm and 4.0 mm. It delivers uniform structural strength across complex contours without adding excess mass.
5.3.2 High-volume stamped parts
When annual part requirements exceed tens of thousands of units, sheet metal stamping provides rapid throughput rates. Dedicated mechanical presses produce finished parts within seconds, significantly reducing machine cycle times compared to laser cutting or CNC machining.
5.3.3 Cost-sensitive OEM components
OEM procurement programs balance unit manufacturing costs against tooling investment. Sheet metal stamping maximizes raw material utilization through optimized strip nesting, lowering piece-part rates for mass-market automotive and industrial assemblies.
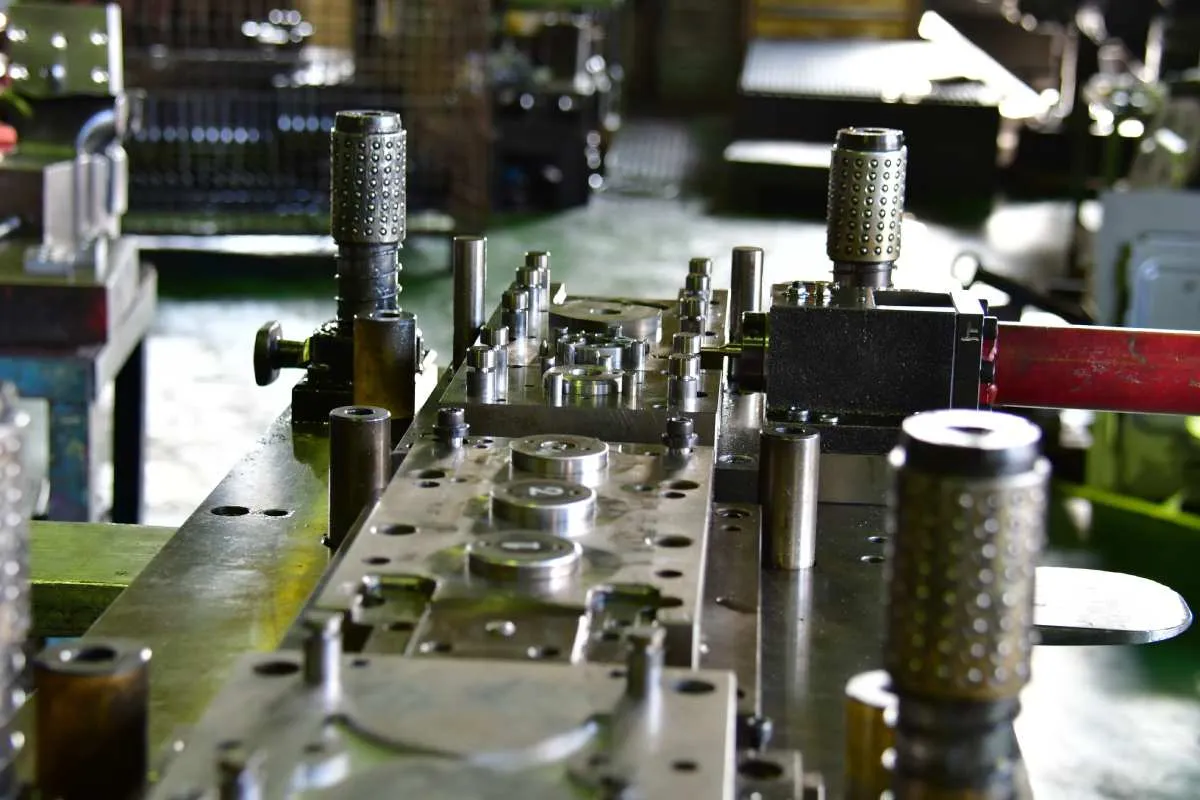
Sheet metal stamping allows manufacturers to achieve repeatable dimensional accuracy on every press stroke
6. Sheet Metal Stamping vs Progressive Die Stamping
6.1 Process comparison
6.1.1 Single or multi-operation stamping
Standard sheet metal stamping often utilizes single-stage, compound, or manual transfer setups where workpieces undergo one or two specific forming operations per press cycle. This approach provides operational flexibility when modifying intermediate part geometries or producing smaller batches.
6.1.2 Continuous multi-station stamping in progressive dies
Progressive die stamping integrates all necessary blanking, piercing, bending, and forming stages into a single continuous tool block. The strip advances automatically from station to station with each press stroke, completing a finished part at the final cutoff station.
6.2 Volume comparison
6.2.1 Sheet metal stamping for flexible production needs
Single-stage and modular sheet metal stamping setups accommodate low-to-medium production volumes (1,000 to 20,000 units annually). These setups allow manufacturers to adapt to design revisions without requiring complete tooling overhauls.
6.2.2 Progressive die stamping for high-volume production
Progressive die tooling is engineered for long-term mass production runs (50,000 to millions of parts annually). Operating at high speeds (100 to 500+ strokes per minute), it delivers consistent output for automotive platforms and consumer electronics lines.
6.3 Cost comparison
6.3.1 Tooling cost differences
Single-operation sheet metal stamping dies require lower initial capital investment due to simpler tool designs. Progressive dies represent a higher upfront engineering and toolmaking expense because they integrate complex cam mechanisms, multi-station punches, and in-die sensors.
6.3.2 Unit cost differences at scale
Despite higher initial tooling costs, progressive die stamping achieves the lowest per-piece cost at scale by eliminating manual handling, reducing labor expenses, and maximizing press stroke efficiency.
| Comparison Parameter | Standard Sheet Metal Stamping | Progressive Die Stamping |
| Tooling Architecture | Single-stage, compound, or modular dies | Integrated multi-station progressive die block |
| Upfront Tooling Cost | Low to Moderate | High initial investment |
| Production Speed | 10 to 40 parts per minute | 100 to 500+ parts per minute |
| Labor Requirement | Moderate (Manual or robotic part transfer) | Low (Fully automated coil feeding) |
| Piece-Part Cost at Scale | Moderate | Lowest unit cost |
| Optimal Annual Volume | 1,000 to 20,000 pieces | 50,000+ pieces |
| Design Flexibility | High (Easier tooling modifications) | Lower (Requires die station rework) |
6.4 Application comparison
6.4.1 Sheet metal parts for general industrial use
Standard sheet metal stamping is widely used for industrial machine enclosures, electrical panel boxes, structural baseplates, and low-volume commercial hardware where production flexibility is prioritized.
6.4.2 Progressive die parts for repeatable automotive production
Progressive die stamping dominates automotive component manufacturing, mass-producing seatbelt latches, sensor brackets, EV busbars, connector pins, and structural reinforcement clips that demand micron-level repeatability.
7. Materials Used in Sheet Metal Stamping
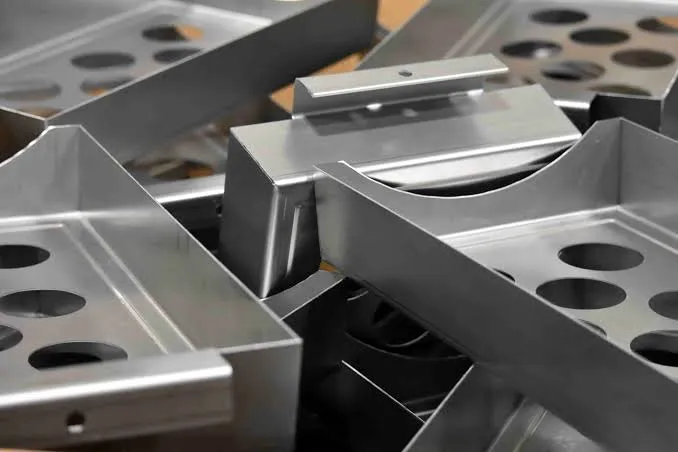
Advanced sheet metal stamping shapes high strength steel without causing structural cracking or tears
7.1 Carbon steel
7.1.1 Cost-effective structural and bracket parts
Cold-rolled carbon steel (such as SPCC and commercial quality steel) provides an economical foundation for automotive and industrial stamping. Its balance of mechanical strength and affordability makes it the standard material for structural brackets, gussets, and equipment chassis.
7.1.2 Good strength and formability
Hot-rolled steel (SPHC) and deep-drawing quality cold-rolled steels (SPCD, SPCE) offer high percentage elongation. This allows the metal to undergo complex multi-axis bends and forming operations without localized thinning or cracking.
7.2 Stainless steel
7.2.1 Corrosion-resistant stamped parts
Austenitic grades (SUS304, SUS316) and ferritic grades (SUS430) offer inherent resistance to chemical exposure, salt spray, and oxidation. They maintain structural integrity in corrosive environments without requiring secondary protective platings.
7.2.2 Industrial and automotive applications
Stainless steel stamping is widely used for automotive exhaust brackets, heat shield baffles, fuel delivery components, food-grade processing equipment, and marine hardware subject to elevated mechanical and thermal stress.
7.3 Aluminum
7.3.1 Lightweight stamped components
Aluminum alloys (such as 5052-H32, 6061-T4/T6, and 3003) offer a density of ~ 2.70 g/cm³, roughly one-third that of steel. Stamping aluminum allows engineers to reduce component mass while preserving structural rigidity.
7.3.2 EV and mobility applications
In electric mobility, aluminum sheet metal stamping manufactures battery module structural frames, thermal management heat sinks, inverter shield covers, and lightweight body closures, supporting extended vehicle driving range.
7.4 Galvanized steel
7.4.1 Corrosion protection for exposed components
Hot-dip galvanized (GI) and electro-galvanized (SECC, SGCC) steel sheets incorporate a sacrificial zinc barrier layer. This coating prevents red rust formation along sheared edges and surface scratches during outdoor service.
7.4.2 Automotive and appliance applications
Galvanized steel stampings are extensively used in automotive body-in-white (BIW) inner reinforcements, commercial HVAC duct housings, refrigerator wrapper panels, and outdoor electrical distribution cabinets.
7.5 Material selection criteria
7.5.1 Strength and formability
Selecting an alloy requires balancing tensile strength against ductile elongation. High-strength materials provide superior load capacity but require larger bend radii and higher press tonnage to avoid tearing during forming.
7.5.2 Thickness and springback behavior
Raw stock with higher yield-to-tensile strength ratios exhibits higher elastic recovery after press strokes. Tool designers factor in material-specific springback characteristics to incorporate appropriate bend compensation into the die geometry.
7.5.3 Surface finish and corrosion resistance
Operating environments dictate the required raw material surface quality. Parts exposed to moisture require stainless or galvanized steel, while parts intended for aesthetic applications demand clean, scratch-free mill surfaces suitable for powder coating.
8. Sheet Metal Thickness and Tolerance Requirements
8.1 Material thickness control
8.1.1 Thickness range based on part function
Sheet metal stamping processes stock ranging from thin precision foils (0.1 mm to 0.5 mm) for electrical terminals up to heavy structural plate (4.0 mm to 6.0 mm+) for automotive chassis links and engine mounting brackets.
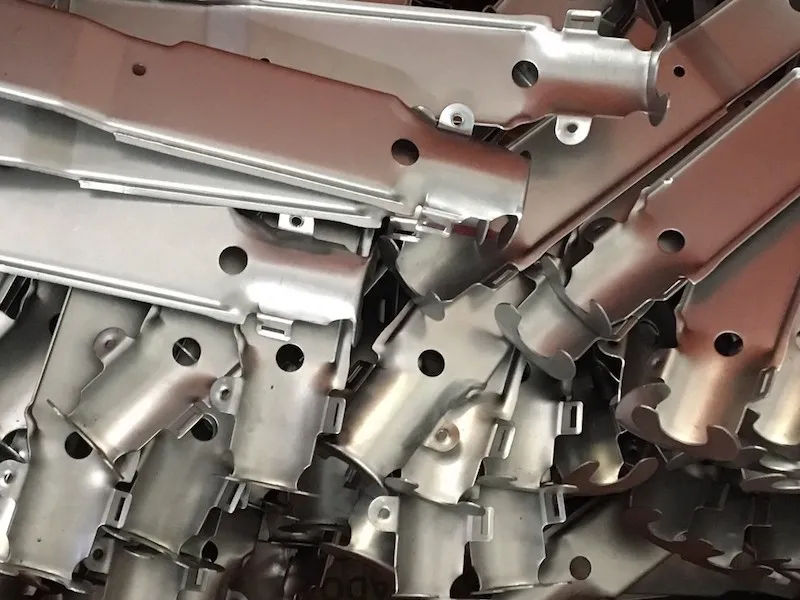
Many global original equipment manufacturers rely on sheet metal stamping for vehicle chassis parts
8.1.2 Impact on press tonnage and tooling design
Material thickness directly governs punch-to-die cutting clearances, which typically range between 5% and 12% of material thickness per side. Thicker plates require higher press tonnage, robust nitrogen stripping springs, and hardened tool steels to manage cutting loads.
8.2 Dimensional tolerance requirements
8.2.1 Standard tolerance for stamped sheet metal parts
Standard industrial sheet metal stampings maintain linear dimensional tolerances between ± 0.10 mm and ± 0.25 mm, with hole center-to-center distances held within ± 0.08 mm. These tolerance bands ensure proper fitment for general commercial enclosures and hardware.
8.2.2 Tight tolerance requirements for automotive parts
Precision automotive assemblies require tighter tolerances, holding critical hole diameters, flange locations, and planar datum faces within ± 0.02 mm to ± 0.05 mm. Achieving these limits requires rigid press guideways and precision carbide die inserts.
8.3 Springback control
8.3.1 Material behavior after forming
When mechanical forming pressure is released, the elastic strain within the sheet metal causes the material to partially return toward its original flat shape. High-strength steels and structural aluminum alloys exhibit notable springback angles that must be controlled.
8.3.2 Die compensation and process adjustment
Toolmakers counteract springback by over-bending the metal in the die cavity, using bottoming (coining) techniques, or integrating relief beads along the bend line. In-die sensors monitor press stroke depth to maintain consistent bend angles across varying coil batches.
8.4 Burr and edge quality control
8.4.1 Burr formation during cutting and piercing
As punches pierce through sheet metal, material undergoes initial elastic deformation, plastic shear, and final fracture. If punch-to-die clearances are excessive or cutting edges become dull, metal tears unevenly, producing exit burrs along part perimeters.
8.4.2 Deburring and edge finishing methods
To maintain edge safety and ensure proper assembly mating, stampings undergo vibratory tumbling, centrifugal barrel finishing, or automated edge-sanding processes. High-precision progressive dies utilize secondary shaving stations to produce smooth, burr-free edges directly within the press tool.
9. Sheet Metal Stamping Tooling
9.1 What is sheet metal stamping tooling?
9.1.1 Stamping die design and manufacturing
Sheet metal stamping tooling comprises custom-engineered die assemblies, punches, strippers, and die blocks mounted inside stamping presses to shape sheet metal workpieces. Tooling development involves 3D CAD parametric modeling, finite element metal-forming simulation, and high-precision CNC milling, surface grinding, and wire EDM machining of vacuum heat-treated tool steels.
9.1.2 Tooling impact on accuracy and repeatability
The structural rigidity, guiding precision, and wear resistance of stamping dies directly dictate finished part accuracy. High-precision die assemblies equipped with ball-bearing guide posts eliminate lateral deflection during press impacts, ensuring that part dimensions remain within micron-level tolerances over hundreds of thousands of press cycles.
9.2 Types of stamping dies
9.2.1 Simple dies
Simple single-operation dies perform a single cutting or forming task (such as blanking, piercing, or simple 90-degree bending) with each press stroke. They feature lower tooling costs and faster fabrication lead times, making them suitable for low-volume production or initial prototype validation.
9.2.2 Compound dies
Compound dies perform multiple cutting operations such as simultaneous external blanking and internal hole piercing in a single press stroke at one work station. Because all cuts are executed concurrently, compound dies produce flat parts with high dimensional concentricity and edge flatness.
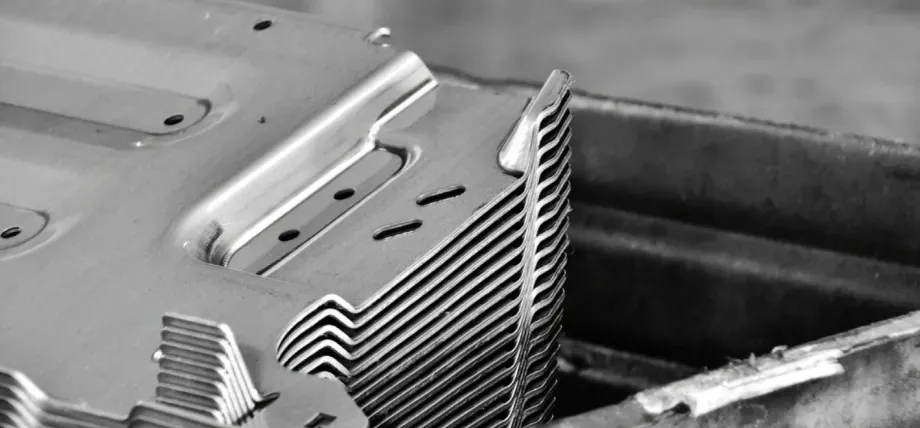
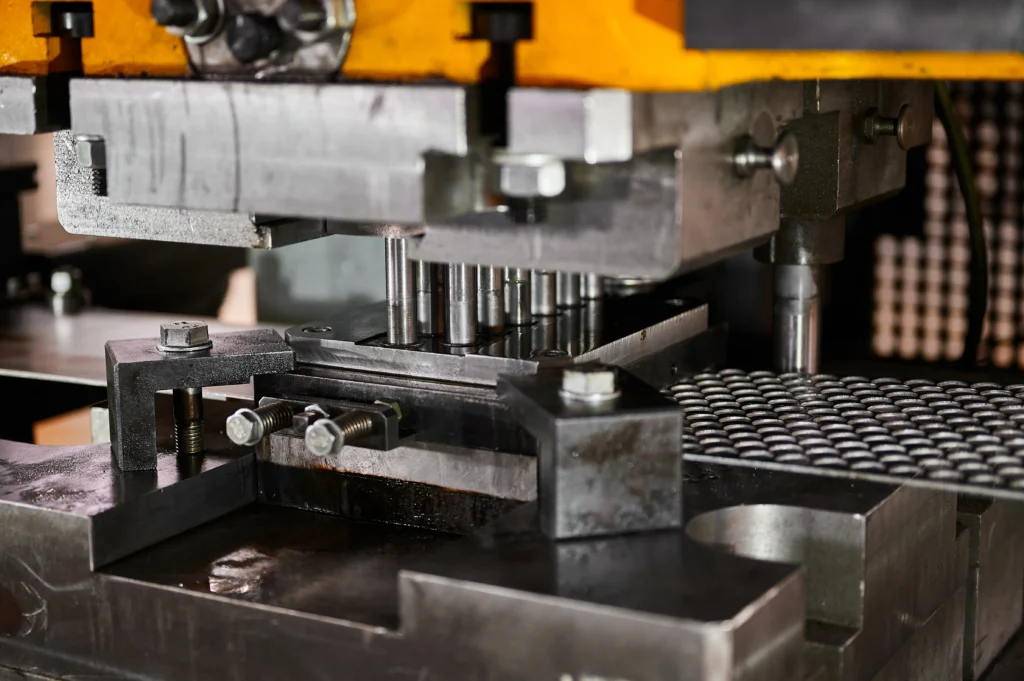
Sheet metal stamping operations typically include blanking, piercing, bending, and deep drawing processes
9.2.3 Progressive dies
Progressive dies integrate multiple sequential forming, piercing, bending, and shearing stations into a single continuous die block. The sheet metal strip feeds automatically through successive stations with each press stroke, completing a finished part at the final cutoff station at high operational speeds (100 to 500+ strokes per minute).
9.2.4 Transfer dies
Transfer dies operate on pre-cut discrete sheet metal blanks rather than continuous coil strips. Mechanical transfer rails or multi-axis robotic fingers physically move the individual workpieces across separate forming stations, making them ideal for large structural panels, deep housings, and heavy-gauge parts.
9.3 Die design considerations
9.3.1 Part geometry and material thickness
Die designers determine cutting clearances, punch radii, and station progression based on raw material gauge and tensile strength. Thicker sheets require larger punch-to-die clearances and heavy-duty nitrogen gas springs to prevent punch chipping and ensure clean slug discharge.
9.3.2 Forming sequence and springback control
Staging forming operations sequentially prevents excessive material thinning and uncontrolled plastic strain. Designers integrate calculated over-bending angles, bottoming relief steps, or localized coining beads into the die geometry to counteract material springback and hold exact final bend angles.
9.3.3 Tool life and maintenance strategy
Selecting high-grade tool steels (D2, SKD11, DC53) or tungsten carbide inserts, paired with physical vapor deposition (PVD) wear coatings such as TiAlN, significantly extends die operating life. Tool layouts incorporate modular inserts to allow rapid replacement of high-wear cutting edges without requiring complete die disassembly.
9.4 Tooling maintenance
9.4.1 Preventive die maintenance
Preventive tooling maintenance follows scheduled press stroke intervals. Technicians disassemble die sets to clean internal cavities, lubricate moving guide pillars, inspect stripper springs, and evaluate cutting punch sharpness under magnification before surface fatigue creates part defects.
9.4.2 Wear monitoring and repair
Operators track punch edge rounding and cutting burr height growth during production. When burr heights exceed acceptable thresholds, toolmakers perform micro-precision surface grinding on punch faces and die blocks to restore crisp cutting edges and maintain drawing clearances.
9.4.3 Tooling cost optimization
Tooling expenditures are optimized through modular die architectures, standardized component catalogs, and in-house toolroom regrinding capabilities. Standardizing die components across multiple part families reduces upfront toolmaking capital and shortens spare parts lead times.
10. Automotive Sheet Metal Stamping Applications
10.1 Automotive sheet metal parts
10.1.1 Brackets and mounting plates
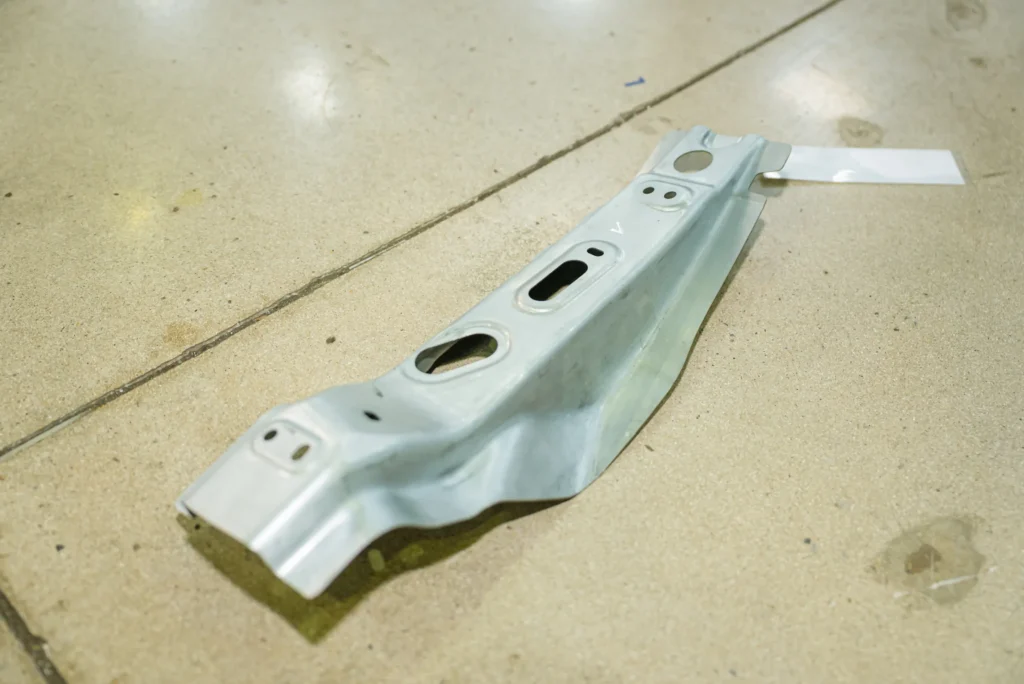
Automotive brackets and mounting plates serve as vital anchor points across vehicle chassis, powertrain compartments, and interior structures. Stamped from high-strength carbon steel or structural aluminum, these parts secure wire harnesses, sensors, radiator modules, and fluid lines against continuous dynamic vibrations.
10.1.2 Reinforcement components
Reinforcement components are structural stampings engineered to absorb impact energy and reinforce vehicle safety zones during collisions. Stamped from ultra-high-strength steel (UHSS) or advanced high-strength steel (AHSS), these parts reinforce bumper beams, door intrusion beams, B-pillar assemblies, and roof headers.
10.1.3 Covers, guards, and panels
Protective sheet metal covers, splash guards, and heat shield panels safeguard sensitive mechanical and electronic sub-assemblies from road debris, moisture, and extreme thermal radiation. Multi-stage stamping dies form complex three-dimensional contours, ventilation louvers, and stiffening ribs to maximize component rigidity.
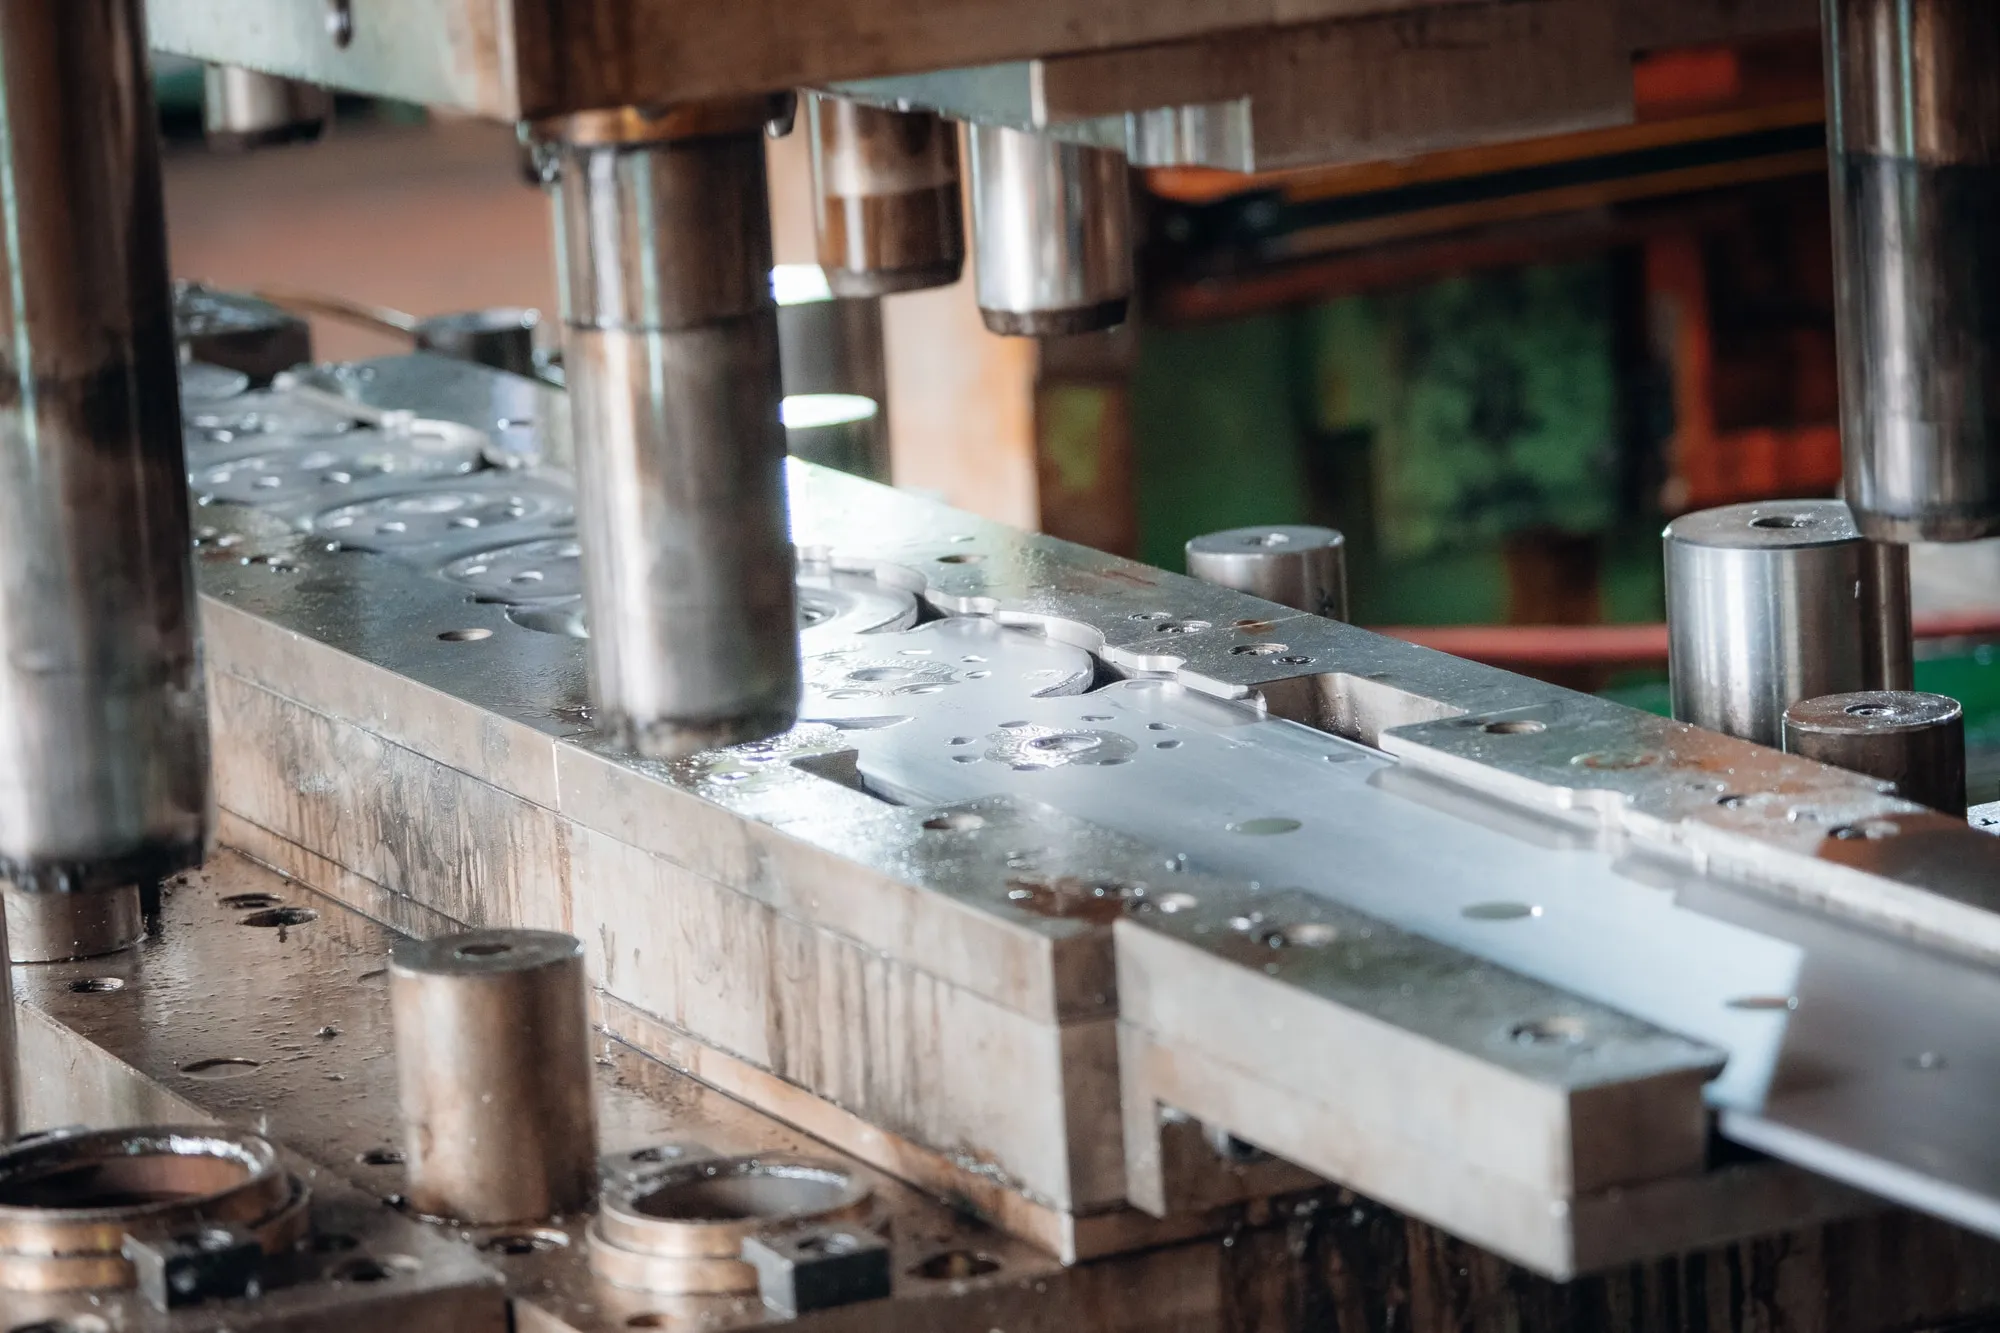
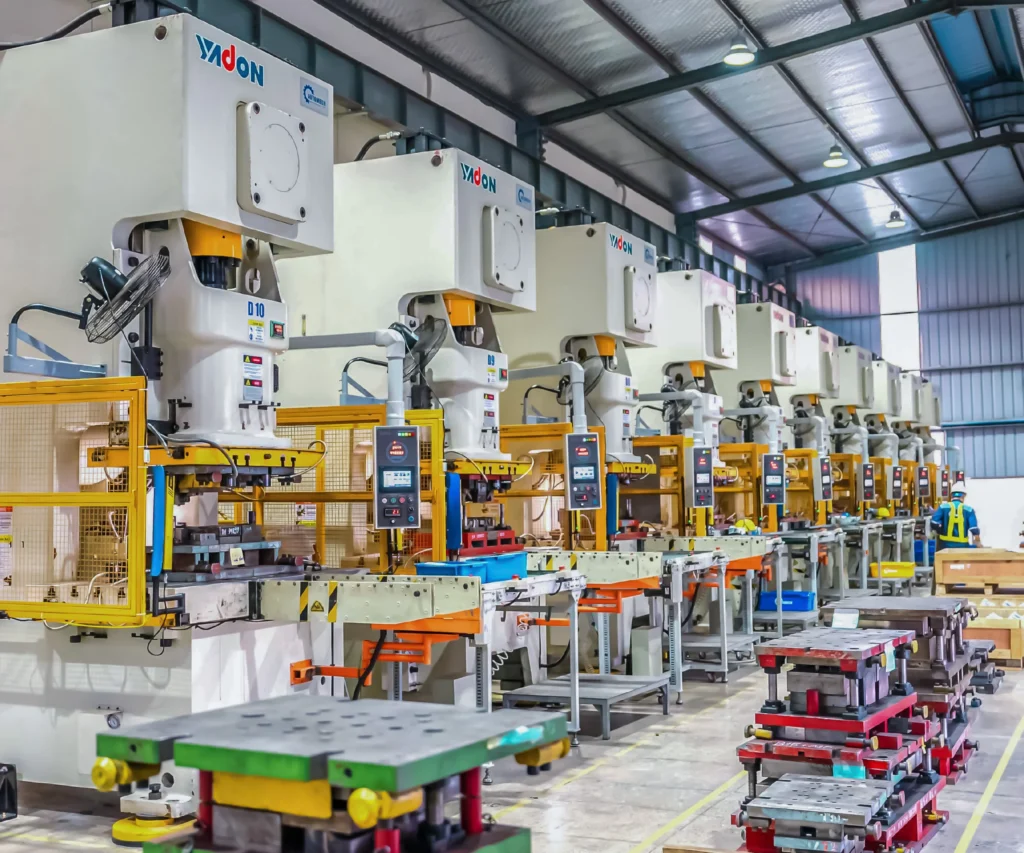
Precision dies enable automated sheet metal stamping lines to run at elevated cycle speeds
10.2 Automotive bracket stamping
10.2.1 Mounting brackets
Mounting brackets require precise hole positions and formed flange angles to align auxiliary components within tight vehicle packaging spaces. High-speed progressive stamping dies produce mounting brackets with integrated fastener clearance holes and locating slots held to tight positional tolerances.
10.2.2 Structural brackets
Structural brackets carry severe mechanical and torsional loads between suspension subframes and body-in-white (BIW) nodes. Stamped from heavy-gauge structural steel (2.0 mm to 6.0 mm thick), these components undergo high-tonnage piercing, flanging, and coining to deliver high fatigue endurance.
10.2.3 Custom OEM bracket components
Custom OEM bracket programs require custom tooling engineered to complex customer 3D models and strict GD&T callouts. Automotive contract manufacturers manage custom bracket production from initial soft-tool prototyping through high-volume automated progressive die runs.
10.3 Automotive structural and assembly parts
10.3.1 Sheet metal sub-components
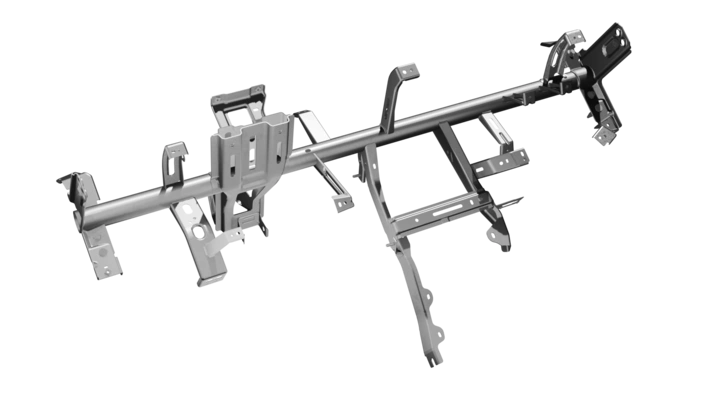
Automotive sub-components including seat frame crossmembers, instrument panel supports, and pedal bracket assemblies comprise multiple stamped sheet metal elements. High-precision stamping ensures that each sub-component fits into downstream welding fixtures without mechanical distortion.
10.3.2 Stamped parts integrated into welded assemblies
Individual stamped sheet metal components are assembled into rigid vehicle modules using automated resistance spot welding, MIG welding, or structural adhesives. Accurate flange contours and burr-free edges ensure continuous contact surfaces and high weld joint integrity.
10.3.3 BIW-related stamped components
Body-in-white (BIW) stamped assemblies form the unpainted, load-bearing structural skeleton of modern passenger cars and commercial vehicles. Stamped panels must maintain surface flatness, dimensional stability, and precise door/window aperture geometries to support automated robotic assembly lines.
10.4 OEM sheet metal stamping parts
10.4.1 Custom parts based on OEM drawings
OEM metal stamping contracts demand custom components manufactured strictly to customer-supplied 2D engineering drawings, CAD geometry, and material specifications. Dedicated stamping suppliers maintain strict process control and traceability to satisfy stringent OEM supplier qualification standards.
10.4.2 Prototype to mass production support
Comprehensive stamping partners assist OEM engineering teams throughout every product lifecycle stage. Suppliers support initial design validation with soft-tool prototype stampings before building hardened progressive or transfer dies capable of delivering millions of parts over multi-year vehicle production platforms.
11. Sheet Metal Stamping Assembly
11.1 Stamping plus welding integration
11.1.1 Spot welding
Resistance spot welding joins overlapping stamped sheet metal parts by applying localized electric current and mechanical clamping pressure. It is widely used in automotive body construction and sheet metal enclosure fabrication to join brackets, reinforcements, and panels cleanly without adding filler material weight.
11.1.2 MIG/TIG welding
MIG (GMAW) and TIG (GTAW) welding provide continuous, high-strength welded joints across thicker structural stampings and heavy chassis assemblies. These welding processes create leak-tight seals and high load-bearing joints on engine cradles, suspension links, and industrial equipment frames.
11.1.3 Robotic welding support
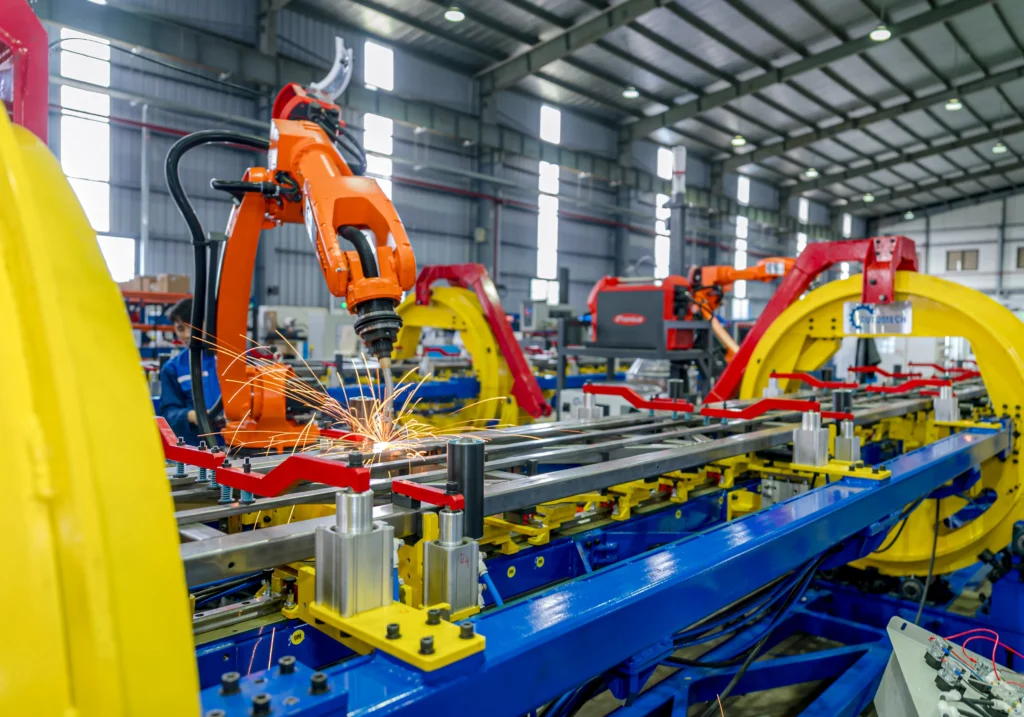
Automated robotic welding cells integrate multi-axis articulated robots with rotary positioning tables. Robotic automation maintains consistent weld bead geometry, minimizes thermal distortion across thin sheet metal assemblies, and significantly increases production throughput for large OEM orders.
11.2 Fixture-controlled assembly
11.2.1 Assembly fixture design
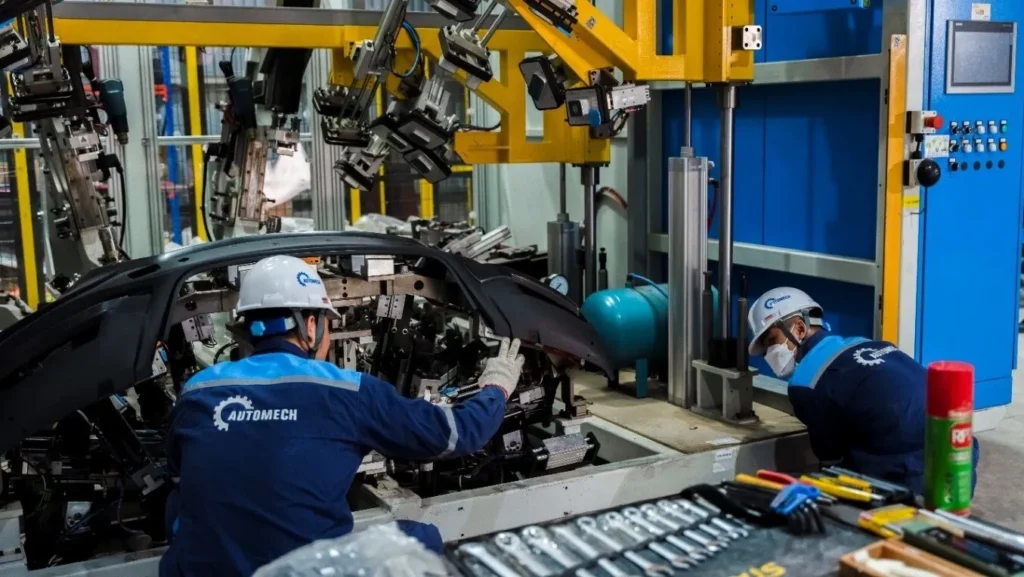
Precision welding and assembly fixtures utilize CNC-machined locating blocks, hardened dowel pins, and pneumatic toggle clamps to hold stamped sub-components in exact spatial alignment. High-accuracy fixture design prevents part shifting under heat and mechanical clamping forces.

Automotive engineers select sheet metal stamping to manufacture lightweight structural aluminum components
11.2.2 Dimensional consistency control
Fixture-controlled assembly eliminates operator alignment variations, ensuring that multi-component welded modules maintain uniform dimensional relationships across production batches. Consistent sub-assembly geometry prevents downstream line assembly issues at vehicle production plants.
11.2.3 Final assembly inspection
Completed welded or mechanically fastened assemblies undergo comprehensive dimensional verification. Coordinate Measuring Machines (CMM) and custom checking fixtures inspect overall part envelopes, mounting hole true positions, and weld seam penetration against customer quality requirements.
11.3 Benefits of integrated stamping assembly
11.3.1 Reduced supplier complexity
Consolidating sheet metal stamping, hardware insertion (PEM nuts, studs), and secondary welding under a single contract manufacturer simplifies supply chain logistics. Single-source management lowers procurement administration costs, minimizes shipping transit risks, and streamlines supplier accountability.
11.3.2 Better production control
In-house assembly integration enables quality teams to monitor manufacturing across all stages from raw coil slitting and press stamping to welding and surface coating. Detecting stamping variations early prevents defective parts from entering assembly cells.
11.3.3 Improved quality consistency
Synchronizing stamping press outputs directly with automated assembly lines establishes a smooth lean manufacturing flow. Coordinated production controls eliminate handling damage, shorten manufacturing lead times, and maintain uniform quality standards across finished modules.
12. Quality Control Systems for Sheet Metal Stamping
12.1 Incoming material inspection
12.1.1 Material certificate verification
Quality assurance begins by verifying raw coil and sheet shipments against mill test reports (EN 10204 3.1 MTR). Quality control inspectors verify chemical composition, tensile strength, yield point, and percentage elongation to confirm raw stock compliance before staging coils at press lines.
12.1.2 Thickness and surface inspection
Inspectors measure sheet metal thickness across coil widths using calibrated digital micrometers and ultrasonic gauges to verify gauge tolerances. Visual and optical inspections confirm that coil surfaces are free of rust, scale, roller marks, pitting, and edge lamination defects.
12.2 First article inspection
12.2.1 Initial part validation
Before authorizing mass production press runs, quality inspectors perform a comprehensive First Article Inspection (FAI) on initial stamped parts off the tool. FAI verification confirms that die alignment, press shut height, and feeder pitch produce compliant components.
12.2.2 Dimensional and functional verification
Quality engineers inspect all drawing dimensions, bend angles, hole centers, and functional GD&T features using CMMs and optical profile projectors. Production commences only after full FAI dimensional approval is formally documented.
12.3 In-process quality control
12.3.1 Dimensional checks during production
Statistical Process Control (SPC) protocols govern continuous production runs. Press operators extract sample parts at defined hourly intervals to verify critical dimensions using dedicated check fixtures, height gauges, and go/no-go plug gauges, logging data into control charts Cpk >= 1.67.
12.3.2 Burr, crack, and surface defect monitoring
Inspectors continually examine stamped edges and drawn radii for micro-fractures, localized necking, scratching, and exit burr heights. Monitoring edge wear ensures that die maintenance and punch sharpening are scheduled before parts exceed drawing limits.
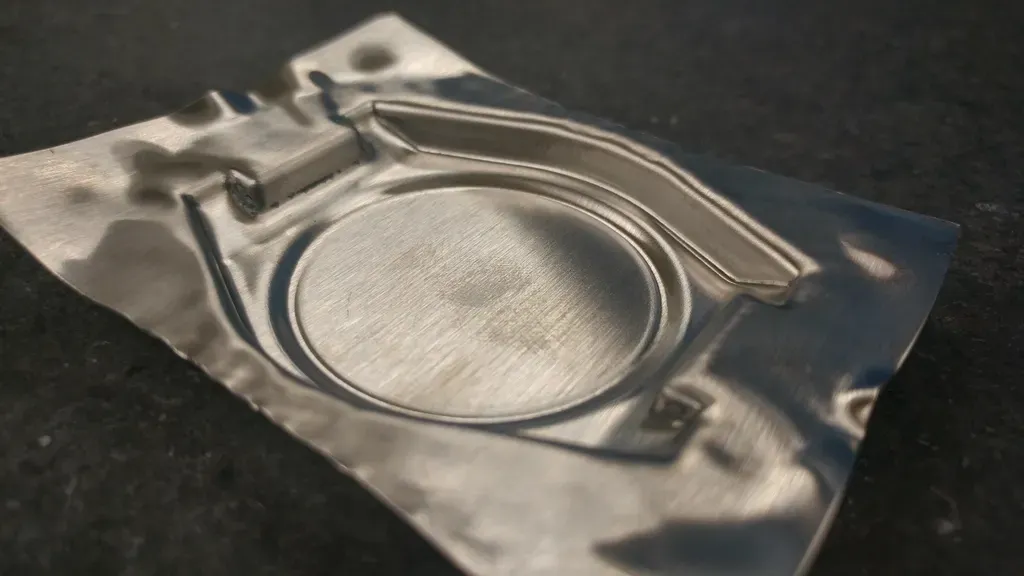
Contract manufacturers integrate sheet metal stamping with automated robotic welding cells
12.3.3 Press and die condition monitoring
Modern press systems utilize in-die tonnage monitors, acoustic sensors, and proximity switches to track dynamic stamping forces. Detecting abnormal tonnage spikes halts the press automatically, preventing tool damage from double-blank feeds or misaligned strips.
12.4 Final inspection
12.4.1 CMM inspection
Coordinate Measuring Machines (CMM) located in climate-controlled quality laboratories (~ 20 °C) inspect finished production lots. High-precision tactile probes measure multi-axis true positions, surface profiles, and hole-to-hole center distances against 3D CAD nominals.
12.4.2 Gauge inspection
Custom attribute checking fixtures and receiver gauges provide fast 100% functional verification for high-volume automotive parts. These gauges simulate real-world vehicle mating points to ensure immediate, zero-defect installation on customer assembly lines.
12.4.3 Visual inspection and packaging check
Final visual checks verify proper surface finishing, plating thickness, complete deburring, and clean packaging. Stamped components are then cleaned, count-verified, and packed into corrosion-inhibiting (VCI) bags or customer-specified returnable containers.
12.5 Traceability and documentation
12.5.1 Batch traceability
Every production batch receives a unique lot tracking number. Critical automotive parts feature laser-etched 2D DataMatrix barcodes or stamped lot codes linking each finished component directly to its raw material master coil, press machine ID, operator shift, and die maintenance records.
12.5.2 Inspection reports
Final shipment packages include complete quality assurance documentation such as CMM dimensional reports, raw material test certificates (MTR), coating thickness logs, and Certificate of Conformance (CoC) records.
12.5.3 Production records for OEM buyers
Digital quality management systems archive inspection logs, SPC trend charts, and material certifications for 10 to 15 years, providing full audit readiness and long-term warranty traceability for international OEM buyers.
13. ISO 9001 and IATF 16949 Requirements
13.1 ISO 9001 for sheet metal stamping suppliers
13.1.1 Quality management system
An ISO 9001 certification establishes a systematic Quality Management System (QMS) across all sheet metal stamping operations. It mandates documented standard operating procedures, regular equipment calibration, structured employee training, and management review frameworks to ensure consistent production standards.
13.1.2 Process standardization
Under ISO 9001, process standardization ensures that die setup, raw material loading, press operation, and quality inspection follow identical, audited procedures during every production run, minimizing operator-induced manufacturing variations.
13.1.3 Continuous improvement
ISO 9001 drives structured continuous improvement initiatives (Plan-Do-Check-Act cycle). Stamping facilities systematically track machine uptime, scrap generation rates, and tool wear trends to implement corrective actions that optimize production efficiency.
13.2 IATF 16949 for automotive stamping suppliers
13.2.1 Automotive-specific quality requirements
IATF 16949 extends basic QMS requirements by introducing rigorous automotive-specific standards focused on defect prevention, supply chain variation reduction, and comprehensive risk management across all stamping stages.
13.2.2 OEM supplier qualification
Global automotive OEMs and Tier 1 suppliers require contract stamping facilities to hold active IATF 16949 certification prior to issuing production contracts. Certification demonstrates a supplier’s capability to deliver zero-defect parts under demanding delivery schedules.
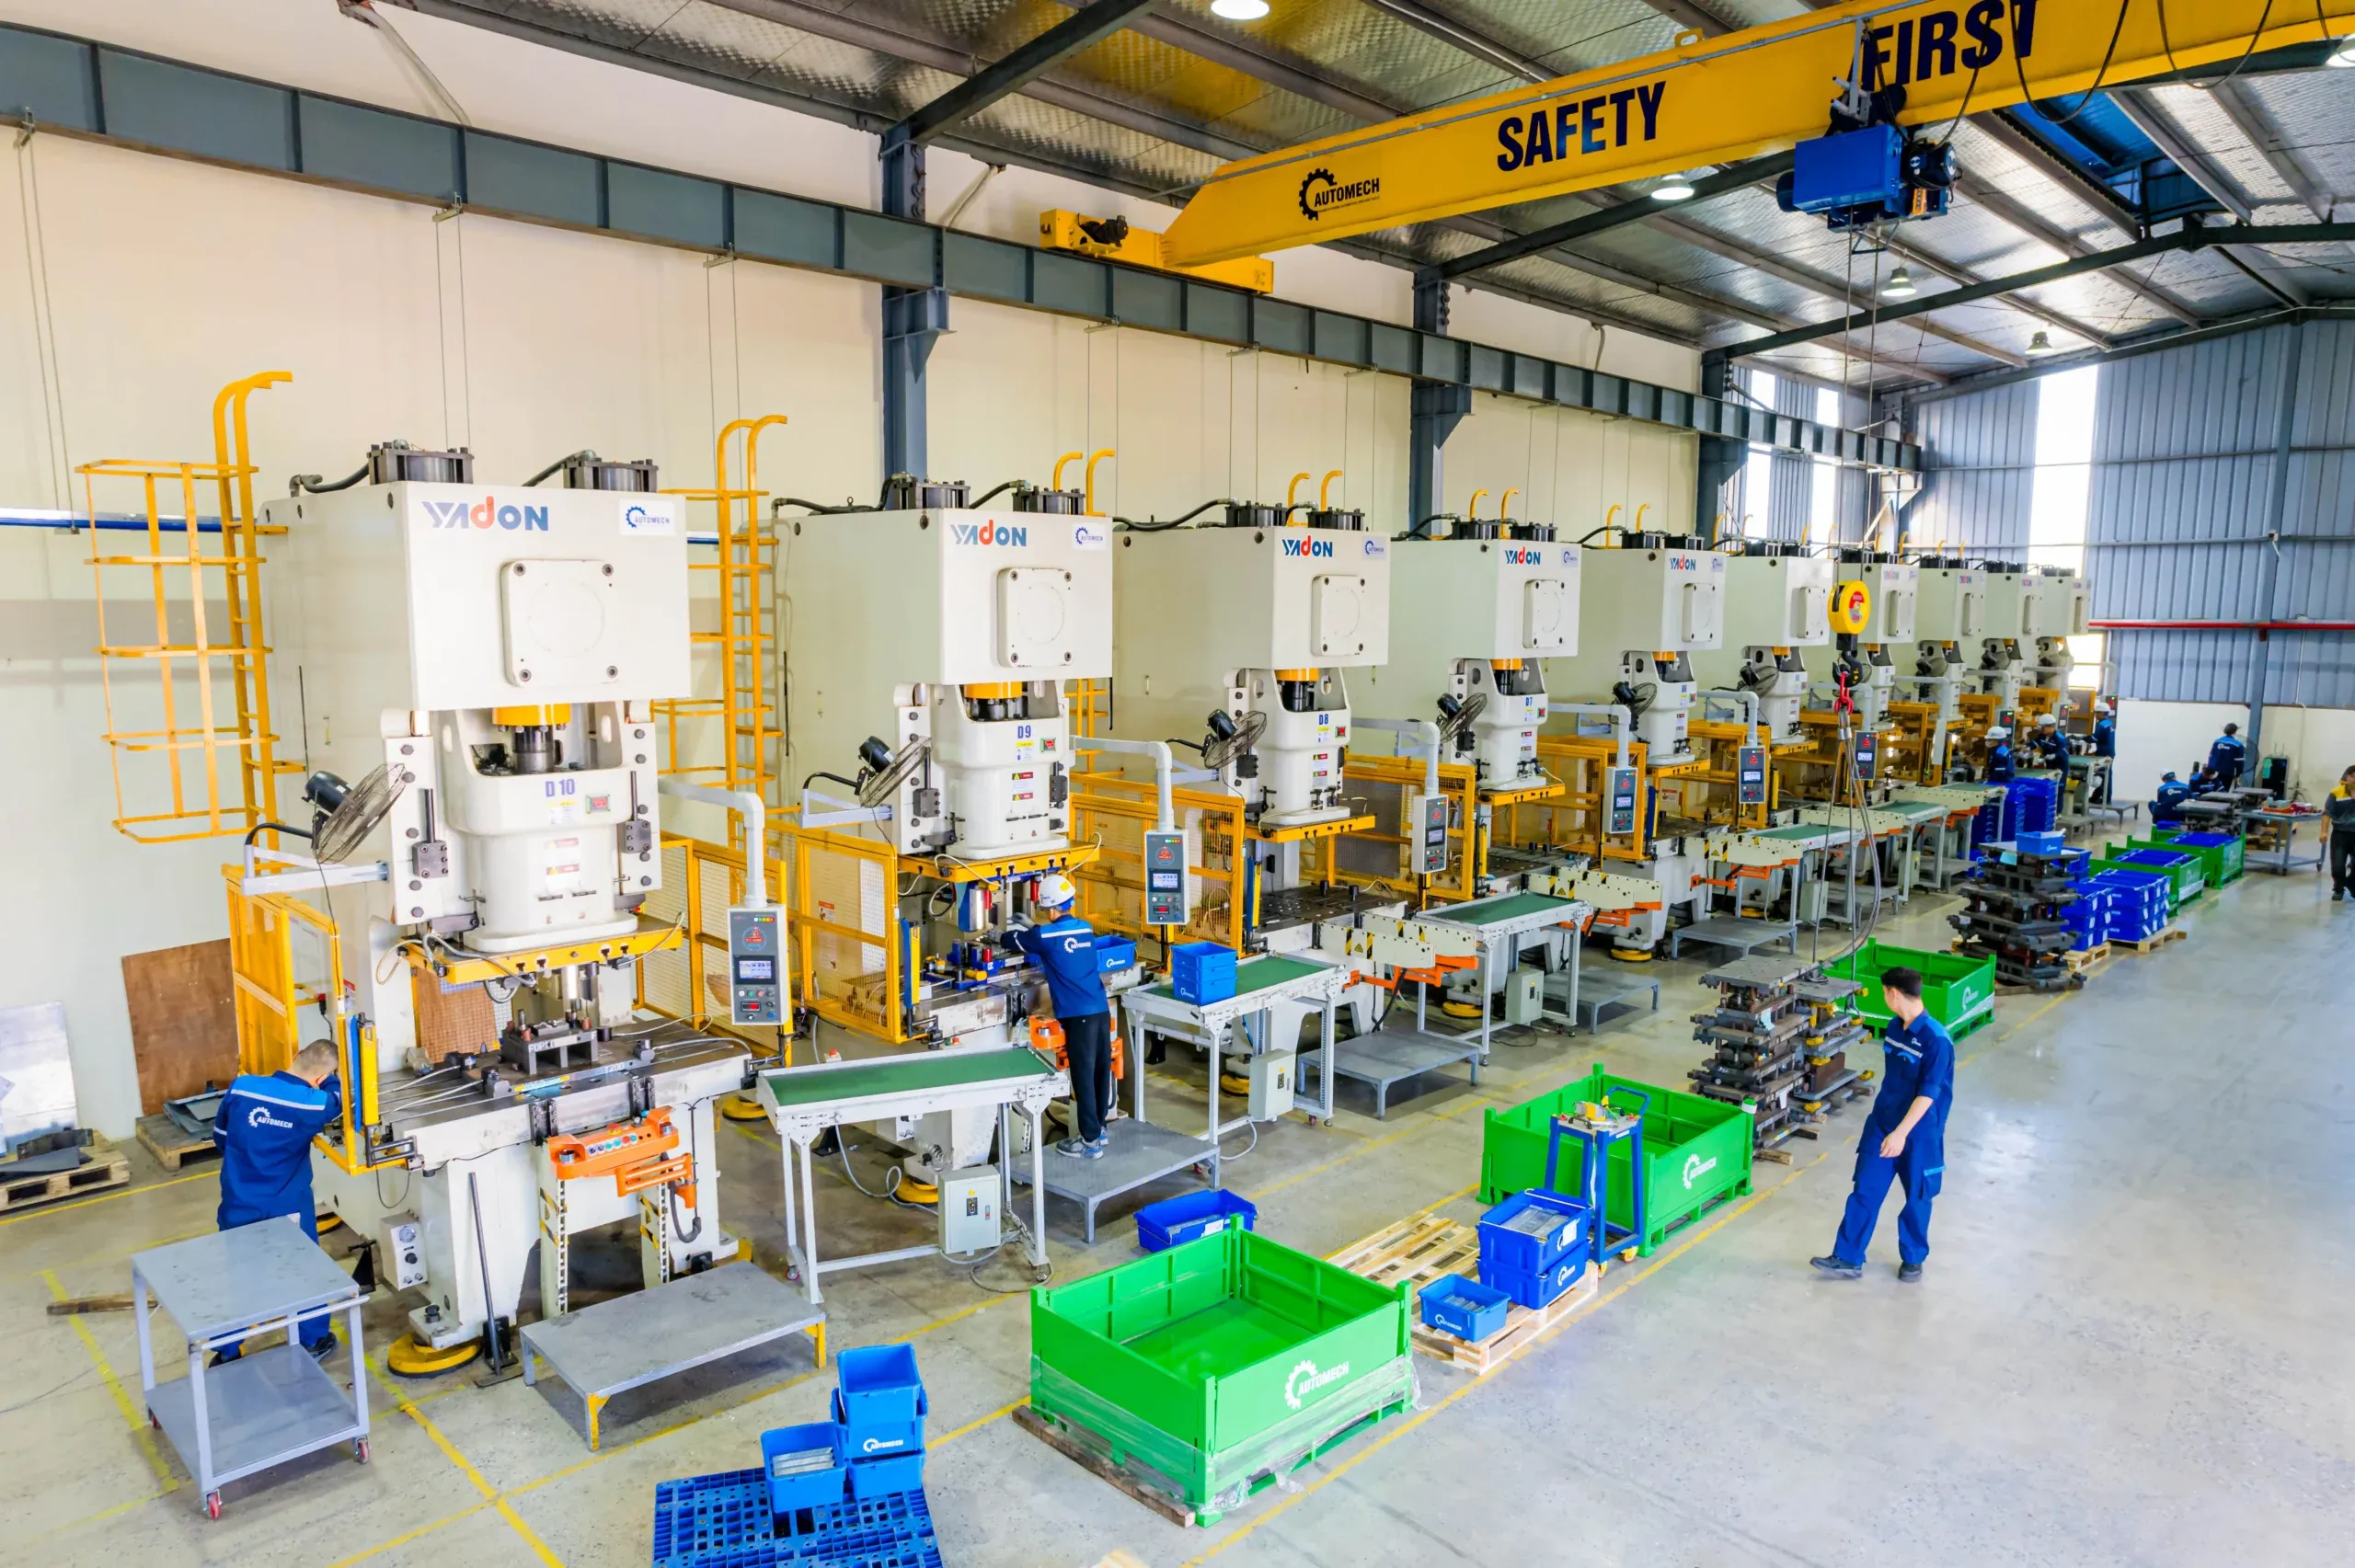
Cold sheet metal stamping forms complex three dimensional contours from flat metal coil stock
13.2.3 Defect prevention and traceability
IATF 16949 mandates advanced error-proofing (Poka-Yoke) systems within stamping dies, automated sensor-based part ejection monitoring, and complete lot traceability from raw steel coils through final vehicle integration.
13.3 Automotive core tools
13.3.1 PPAP
The Production Part Approval Process (PPAP) validates that the supplier’s manufacturing process can consistently produce parts meeting all engineering drawing requirements at full production press speeds. Level 3 PPAP packages include sample parts, complete CMM dimensional results, gauge R&R studies, process flow diagrams, and raw material certifications.
13.3.2 APQP
Advanced Product Quality Planning (APQP) provides a structured project management framework from initial die concept design through full-scale mass production launch. APQP aligns engineering, toolmaking, production, and quality teams to identify and resolve manufacturing risks early.
13.3.3 Control plan
A Control Plan defines specific inspection checkpoints, measuring instruments, sample frequencies, and reaction plans across every stage of production including incoming coil receiving, blanking, forming, deburring, plating, and packaging.
13.3.4 FMEA
Failure Mode and Effects Analysis (Design FMEA and Process FMEA) proactively identifies potential failure modes in tooling design or press operations. Engineering teams implement corrective tool modifications and automated sensor interlocks to eliminate high-risk failure modes before production tooling is finalized.
14. Sheet Metal Stamping Pricing Factors
14.1 Main cost drivers
14.1.1 Material type and thickness
Raw material selection establishes the baseline cost of any stamped part. Premium alloy grades such as SUS304 stainless steel or specialized 6061-T6 aluminum carry higher raw material costs than standard commercial cold-rolled carbon steel (SPCC). Increasing sheet thickness also requires higher press tonnage and heavier raw coil weight per thousand parts.
14.1.2 Part complexity
The physical geometry of the part directly determines the number of stamping stages and die stations required. Complex profiles featuring deep draw recesses, compound flanges, dense piercing patterns, or tight embossed ribs require larger progressive die sets, which increases upfront engineering and tooling budgets.
14.1.3 Tolerance and surface finish requirements
Achieving tight dimensional tolerances (down to ± 0.02 mm) demands precision-ground carbide die inserts, automated in-die sensor monitoring, and complete CMM dimensional inspection. Specialized cosmetic requirements such as mirror polishing, burr-free edge shaving, or pre-painted coil handling add process controls that influence final unit pricing.
14.1.4 Production volume
Total order volume significantly influences component piece pricing. Large production runs amortize non-recurring engineering (NRE) setup and tooling expenses across hundreds of thousands of parts, delivering lower per-unit manufacturing costs compared to prototype or low-volume batches.
14.2 Tooling cost factors
14.2.1 Die complexity
Tooling costs depend on the number of sequential cutting, bending, and forming stations integrated into the die block. Complex three-dimensional contours require multi-axis CAM programming, precision CNC milling, and specialized wire EDM machining of hardened tool steels.
14.2.2 Progressive die vs simple die
Progressive dies integrate multiple forming stages into a single continuous tool set, requiring higher initial toolmaking capital. Simple single-operation dies cost significantly less to design and build upfront, but require manual part transfers that increase piece-part labor expenses.
14.2.3 Expected tool life and maintenance
Dies manufactured from premium tool steels (D2, DC53, SKD11) or tungsten carbide inserts withstand millions of press strokes before requiring maintenance. High-grade tooling materials increase initial tool investment, but eliminate unexpected press downtime and frequent sharpening stops.
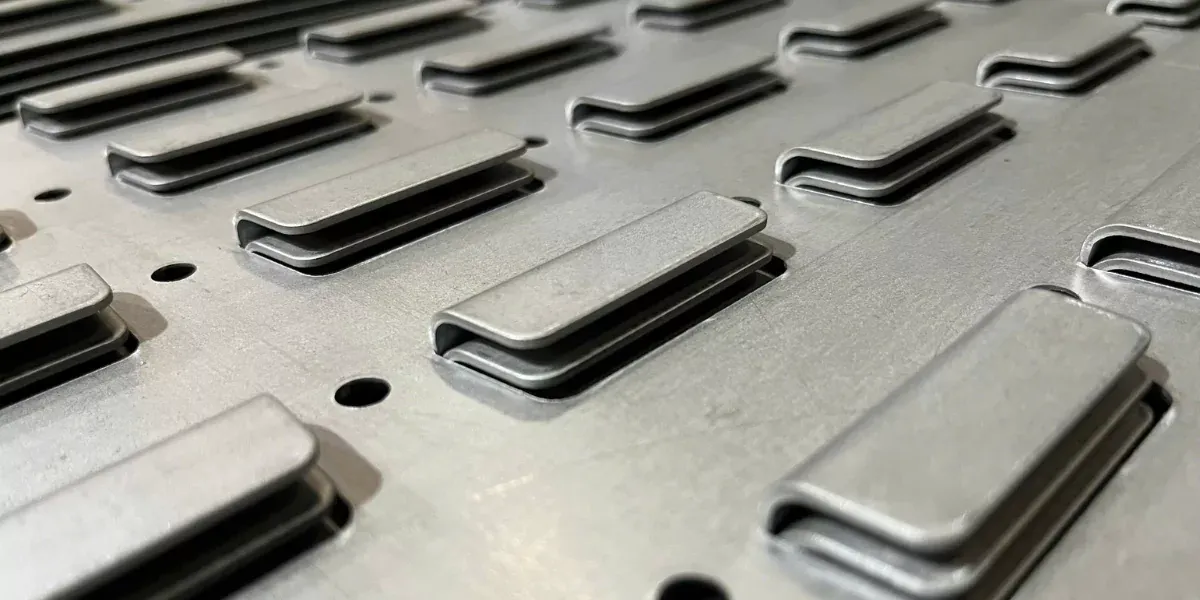
Modern electric vehicle battery pack enclosures require high precision sheet metal stamping
14.3 Production cost factors
14.3.1 Press time
Press time reflects machine hourly rates based on press tonnage and operational stroke speeds. Automated high-speed mechanical presses operating at 150 to 300+ strokes per minute achieve maximum efficiency, substantially lowering the press processing cost per component.
14.3.2 Setup time
Before initiating production runs, technicians must install upper and lower die shoes, calibrate servo feeder pitches, and verify press shut-height settings. For short production runs, lengthy setup procedures increase the allocated hourly overhead cost per batch.
14.3.3 Secondary operations such as welding or deburring
Post-stamping processing steps such as vibratory deburring, barrel washing, spot welding, fastener insertion, and powder coating add handling time to the manufacturing sequence. Streamlining secondary operations through automated cells helps control total finished part costs.
14.4 Cost optimization methods
14.4.1 Design for Manufacturability
Conducting Design for Manufacturability (DFM) reviews early in part development simplifies tooling geometry. Standardizing bend radii, maintaining adequate hole-to-edge clearances, and avoiding narrow web sections reduce tooling complexity and shorten production cycle times.
14.4.2 Material utilization improvement
Optimizing strip layouts through automated blank nesting software minimizes scrap skeleton generation between adjacent parts. Improving strip utilization rates directly lowers raw material expenditure per finished component.
14.4.3 Tooling strategy optimization
Matching die architecture to projected product lifecycles prevents over-engineering. Short-run or prototype programs benefit from modular single-operation tooling, whereas multi-year OEM mass production programs justify full progressive die automation.
14.4.4 Volume-based pricing
Consolidating annual component demand into larger, scheduled production releases enables suppliers to run continuous automated press cycles. Bulk material coil purchasing and uninterrupted machine runs yield significant volume-tiered cost savings.
15. Why Choose Vietnam for Sheet Metal Stamping
15.1 Vietnam manufacturing advantages
15.1.1 Competitive production cost
Vietnam provides an advantageous cost structure for labor-intensive and high-precision metal stamping operations. Favorable operational overheads and competitive labor costs allow contract manufacturers to deliver high-quality stamped components at competitive global pricing.
15.1.2 Growing metal forming and tooling capability
Vietnam’s industrial manufacturing sector has made substantial technological advancements in precision toolmaking, die design, and automated pressworking. Contemporary facilities feature high-tonnage mechanical presses, precision wire EDM machining, and automated robotic welding cells.
15.1.3 Skilled manufacturing workforce
Vietnam maintains a deep talent pool of mechanical engineers, CAD/CAM programmers, toolmakers, and quality assurance professionals. Local technical expertise enables smooth execution of complex progressive die programs and precision contract manufacturing projects.
15.2 Vietnam for US and European buyers
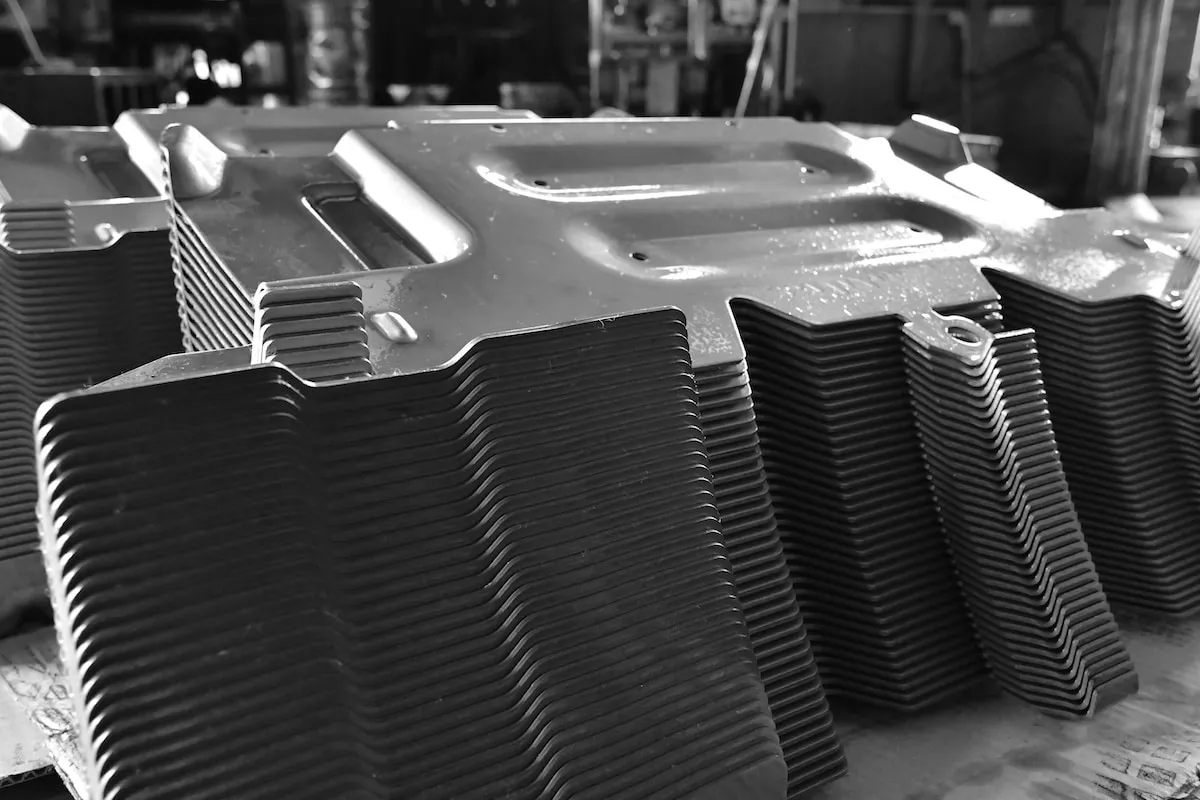
Sheet metal stamping minimizes raw material waste through optimized coil strip layout designs
15.2.1 Export manufacturing readiness
Vietnamese precision metal stamping exporters possess extensive experience serving OEM and Tier buyers across North America and Europe. Suppliers understand international engineering standards, technical documentation requirements, and protective export packaging methods.
15.2.2 Supply chain diversification from China
Global manufacturing enterprises actively pursue supply chain diversification strategies to reduce reliance on single-country sourcing. Sourcing stamped sheet metal parts from Vietnam mitigates trade disruption risks while maintaining production quality and schedule continuity.
15.2.3 Cost-quality balance for OEM production
Vietnam offers a balanced combination of competitive manufacturing costs and strict compliance with international engineering standards. Buyers obtain certified quality systems (such as ISO 9001 and IATF 16949) at competitive production rates.
15.3 Vietnam as an alternative China stamping supplier
15.3.1 Reduced single-country sourcing risk
Relying entirely on a single manufacturing origin creates operational risks from regional disruptions and tariff fluctuations. Diversifying stamping production lines into Vietnam provides supply chain resilience.
15.3.2 Stable manufacturing environment
Vietnam provides a stable socio-economic, regulatory, and industrial climate supported by national investments in deep-water ocean ports, expressways, and specialized industrial zones. This stability ensures predictable freight transit timelines to Western markets.
15.3.3 Stronger China+1 sourcing strategy
Integrating Vietnamese contract stamping facilities into an established China+1 sourcing framework provides maximum supply flexibility. International buyers maintain dual-sourcing options without sacrificing toolmaking capability or part quality.
16. How to Choose a Sheet Metal Stamping Supplier
16.1 Technical capability checklist
16.1.1 Press capacity and tonnage
Verify that the supplier operates a diverse press fleet ranging from 40-ton precision presses to 800+ ton heavy-tonnage mechanical, hydraulic, or tandem press lines to accommodate both thin precision parts and heavy structural plates.
16.1.2 Material thickness capability
Confirm the supplier’s experience in processing required metal gauges, spanning thin precision strips (0.1 mm) up to heavy plate (6.0 mm+) across cold-rolled steel, stainless steel, aluminum, and galvanized coils.
16.1.3 Tooling design and maintenance capability
Prioritize stamping partners with in-house tool and die design capabilities, wire EDM machining equipment, and structured preventive die sharpening programs to maximize tool operating lifespans.
16.2 Quality system checklist
16.2.1 ISO 9001 certification
Ensure active ISO 9001 certification to verify that standard operating procedures, raw material verification, and measurement equipment calibrations are audited systematically.
16.2.2 IATF 16949 capability for automotive projects
For automotive programs, require IATF 16949 capability to ensure strict defect prevention, process risk management, and automated error-proofing across all active stamping lines.
16.2.3 PPAP and APQP readiness
Confirm the supplier’s engineering team is trained in Advanced Product Quality Planning (APQP) and capable of submitting complete Level 3 PPAP packages prior to launching mass production.

Toolmakers optimize sheet metal stamping tooling to counteract material springback and hold tolerances
16.3 Engineering support checklist
16.3.1 DFM support
Select a supplier offering upfront Design for Manufacturability (DFM) reviews to optimize bend radii, hole clearances, and blank profiles before freezing die designs.
16.3.2 Tooling feasibility review
Ensure the engineering team performs simulation reviews regarding strip stretch limits, springback behavior, and punch tonnage demands during the initial quotation stage.
16.3.3 Stamping cost optimization
An experienced partner proactively suggests material thickness optimizations, standardized hole configurations, and efficient die layouts to lower unit piece prices.
16.4 Export readiness checklist
16.4.1 Experience serving US/EU buyers
Verify a proven track record of exporting stamped components to North America and Europe, ensuring clear technical communication, Milestone management, and schedule adherence.
16.4.2 Export documentation capability
Ensure the supplier provides complete export compliance documentation, including Mill Test Reports (MTR), CMM dimensional verification data, and Certificates of Conformance.
16.4.3 Packaging and logistics capability
Confirm that parts are protected using Vapor Corrosion Inhibitor (VCI) bags, custom returnable dunnage, and ocean-freight palletizing to prevent transport rust or physical handling damage.
17. Sheet Metal Stamping RFQ Process
17.1 How to request a sheet metal stamping quote
17.1.1 Submit 2D drawings and 3D CAD files
Provide STEP or IGES 3D CAD models for geometry analysis, along with detailed 2D PDF technical drawings indicating critical tolerances, hole centers, thread callouts, and GD&T requirements.
17.1.2 Provide material, thickness, tolerance, and volume requirements
Explicitly define raw material specifications (e.g., SPCC carbon steel, SUS304 stainless steel), sheet thickness, allowable dimensional tolerances, and projected annual production volumes.
17.1.3 Specify surface finish and secondary operations
State all required secondary processes upfront including vibratory deburring, zinc plating, E-coating, spot welding, or self-clinching fastener installation.
17.2 Engineering review process
17.2.1 Tooling feasibility analysis
Engineers analyze 3D models to evaluate material flow, draw depths, internal corner radii, and springback risks, determining whether progressive, compound, or transfer tooling is required.
17.2.2 Stamping process planning
Manufacturing teams map out the complete operational sequence from raw coil decoiling and strip punching to secondary cleaning, plating, and final quality inspection.
17.2.3 Cost and lead time estimation
Based on press cycle speeds, raw material tonnage, tooling fabrication hours, and quality checks, suppliers issue transparent piece-price quotations and tooling delivery schedules.
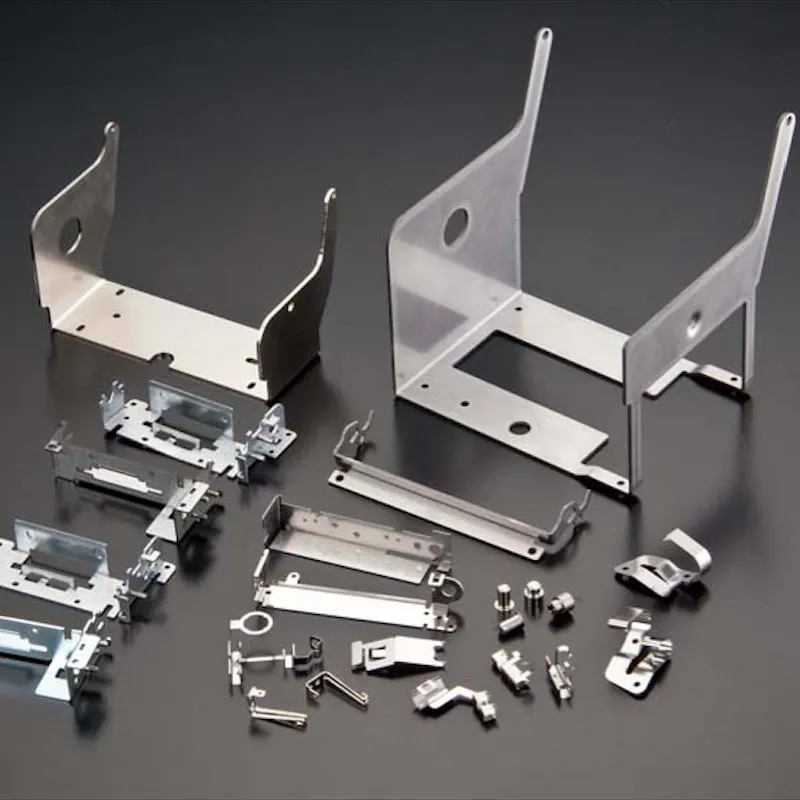
Automotive supply chains depend on sheet metal stamping for mass production of safety components
17.3 What buyers should prepare
17.3.1 Technical drawings
Fully dimensioned technical drawings with clean line geometry allow toolmakers to accurately calculate punch clearances, press tonnage requirements, and strip progressions.
17.3.2 Annual volume forecast
Providing prototype requirements alongside 1-year and 3-year production forecasts helps suppliers recommend optimal tooling strategies and volume-tiered piece pricing.
17.3.3 Quality and inspection requirements
Define required quality deliverables upfront such as First Article Inspection (FAI) reports, CMM measurement logs, or full Level 3 PPAP submission packages.
17.3.4 Packaging and delivery requirements
Specify custom packaging needs, such as VCI anti-rust wrapping, individual carton labeling, or returnable plastic dunnage trays suitable for automated assembly lines.
17.4 Faster RFQ best practices
17.4.1 Clear tolerance requirements
Distinguish critical functional mating dimensions from general non-critical features. Avoid applying unnecessarily tight tolerances across non-functional part edges to prevent excess tooling costs.
17.4.2 Defined material specifications
Specify standard ASTM, EN, or JIS material grades to help suppliers immediately verify local raw coil availability and current market steel pricing.
17.4.3 Early communication with engineering team
Engaging the supplier’s engineering team during early design stages identifies cost-saving geometry adjustments before freezing production drawings.
18. Trusted Sheet Metal Stamping Supplier in Vietnam – Automech
18.1 Automech sheet metal stamping capability
18.1.1 Sheet metal stamping for OEM components
Established in 2020, Automech (Automech Mechanical Equipment and Solutions Joint Stock Company) provides comprehensive sheet metal stamping services for OEM components. The company processes flat sheets and coils into structural, functional, and decorative components using modern press equipment.
18.1.2 Precision metal stamping support
Automech delivers precision metal stamping solutions with micro-level tolerance control and zero-burr edge quality. Advanced press systems and rigid die sets produce tight-tolerance components for electronics, appliances, and industrial machinery.
18.1.3 Progressive die stamping capability
Capitalizing on high-speed automated press lines, Automech designs and operates progressive die systems that execute continuous piercing, bending, and forming in single tool sets for high-volume orders.
18.2 Tooling and engineering support
18.2.1 Metal stamping tooling support
Automech offers turnkey tool and die support. Factory 1 in Bac Ninh (10,500 m²) features dedicated tooling areas, CNC machining centers, wire EDM machines, and tryout presses for die manufacturing.
18.2.2 Die design and manufacturing support
Automech’s in-house engineering and R&D team designs and manufactures cold stamping dies, welding jigs, assembly fixtures, and inspection gauges tailored to complex customer CAD models.
18.2.3 Tooling feasibility review
Before hardening die components, Automech conducts thorough DFM and tool feasibility reviews to analyze metal stretch, springback compensation, and press tonnage distribution, ensuring smooth mass production launch.
18.3 Automotive stamping experience
18.3.1 Automotive sheet metal parts
Automech produces automotive structural sheet metal components, electric bus frame structures, interior panels, and body reinforcements. Factory 2 (10,000 m², inaugurated June 2026) is dedicated to high-volume automotive component manufacturing with an 80% target automation rate.

Sheet metal stamping shapes carbon steel, stainless steel, and aluminum for industrial machinery components
18.3.2 Automotive bracket stamping
Automech manufactures motor mounts, suspension brackets, sensor holders, and chassis gussets. Multi-station stamping dies yield precise hole patterns and formed flange angles across mass batches.
18.3.3 Automotive stamping assembly
Automech integrates individual stamped parts into complete automotive sub-assemblies. The company combines progressive press stamping with automated welding, riveting, and fastener insertion for leading clients including VinFast, VinES, Hoa Phat, Kim Long Motors, and Seojin.
18.4 Welding and assembly capability
18.4.1 Stamped part assembly
Automech operates dedicated assembly zones where stamped components are assembled with mechanical hardware, bushings, and fasteners under strict fixture control.
18.4.2 Welding integration
Automech integrates robotic welding cells, spot welding stations, laser welding, and ultrasonic welding systems. Applications include automated 800-1300 ton tandem stamping lines with ABB robots and electric bus frame welding with KUKA robots and Fronius power sources.
18.4.3 Fixture-controlled assembly
To ensure zero-clearance fitment, Automech builds precision welding jigs and inspection fixtures (Jigs) in-house. Custom clamping fixtures align stamped parts accurately during robotic joining.
18.5 Quality and inspection systems
18.5.1 CMM inspection
Automech utilizes Coordinate Measuring Machines (CMM) and optical measuring systems in climate-controlled laboratories (~ 20 °C). Dimensional checks validate complex GD&T parameters directly against customer CAD models.
18.5.2 First article inspection
Strict quality protocols require complete First Article Inspection (FAI) approval before launching mass production press runs. Inspectors verify all drawing dimensions, form angles, and hole locations.
18.5.3 In-process quality control
Quality control is embedded across all manufacturing stages. Statistical sampling, in-die sensor monitoring, and automated vision checks track part dimensions to maintain process stability.
18.5.4 Traceability and QA documentation
Automech provides complete quality documentation packages including material certificates, heat treatment logs, CMM dimensional reports, and batch traceability data required by global OEM auditors.
18.6 Export manufacturing capability
18.6.1 Experience serving US/EU buyers
Automech’s modern production facilities and engineering systems are structured to serve international Tier 1 and OEM buyers across North America, Europe, and Asia. The engineering team adheres to international standards and B2B project management practices.
18.6.2 Export-ready production and documentation
Automech prepares export orders with protective VCI anti-rust packaging, wooden palletizing, clear shipping labels, and comprehensive customs clearance documentation.
18.6.3 RFQ support for international buyers
International buyers can initiate project inquiries by submitting technical drawings and CAD files. Automech’s solution engineering team delivers prompt DFM feedback, tooling feasibility reviews, and competitive quotations tailored to global production demands.
19. AI Overview & Featured Snippet Section
19.1 People Also Asked questions
19.1.1 What is sheet metal stamping?
Sheet metal stamping is a cold-forming manufacturing process that uses mechanical or hydraulic presses equipped with custom die sets to cut, bend, form, or draw flat metal sheets and coils into finished components. It enables high-volume manufacturing of durable, precision parts with minimal cycle times.
19.1.2 How does sheet metal stamping work?
The sheet metal stamping process begins with feeding raw metal sheets or uncoiled strips into a press. Hardened upper and lower dies descend under high mechanical force to shear, pierce, bend, or draw the material into exact contours. The finished workpieces are then ejected, deburred, inspected, and packaged.
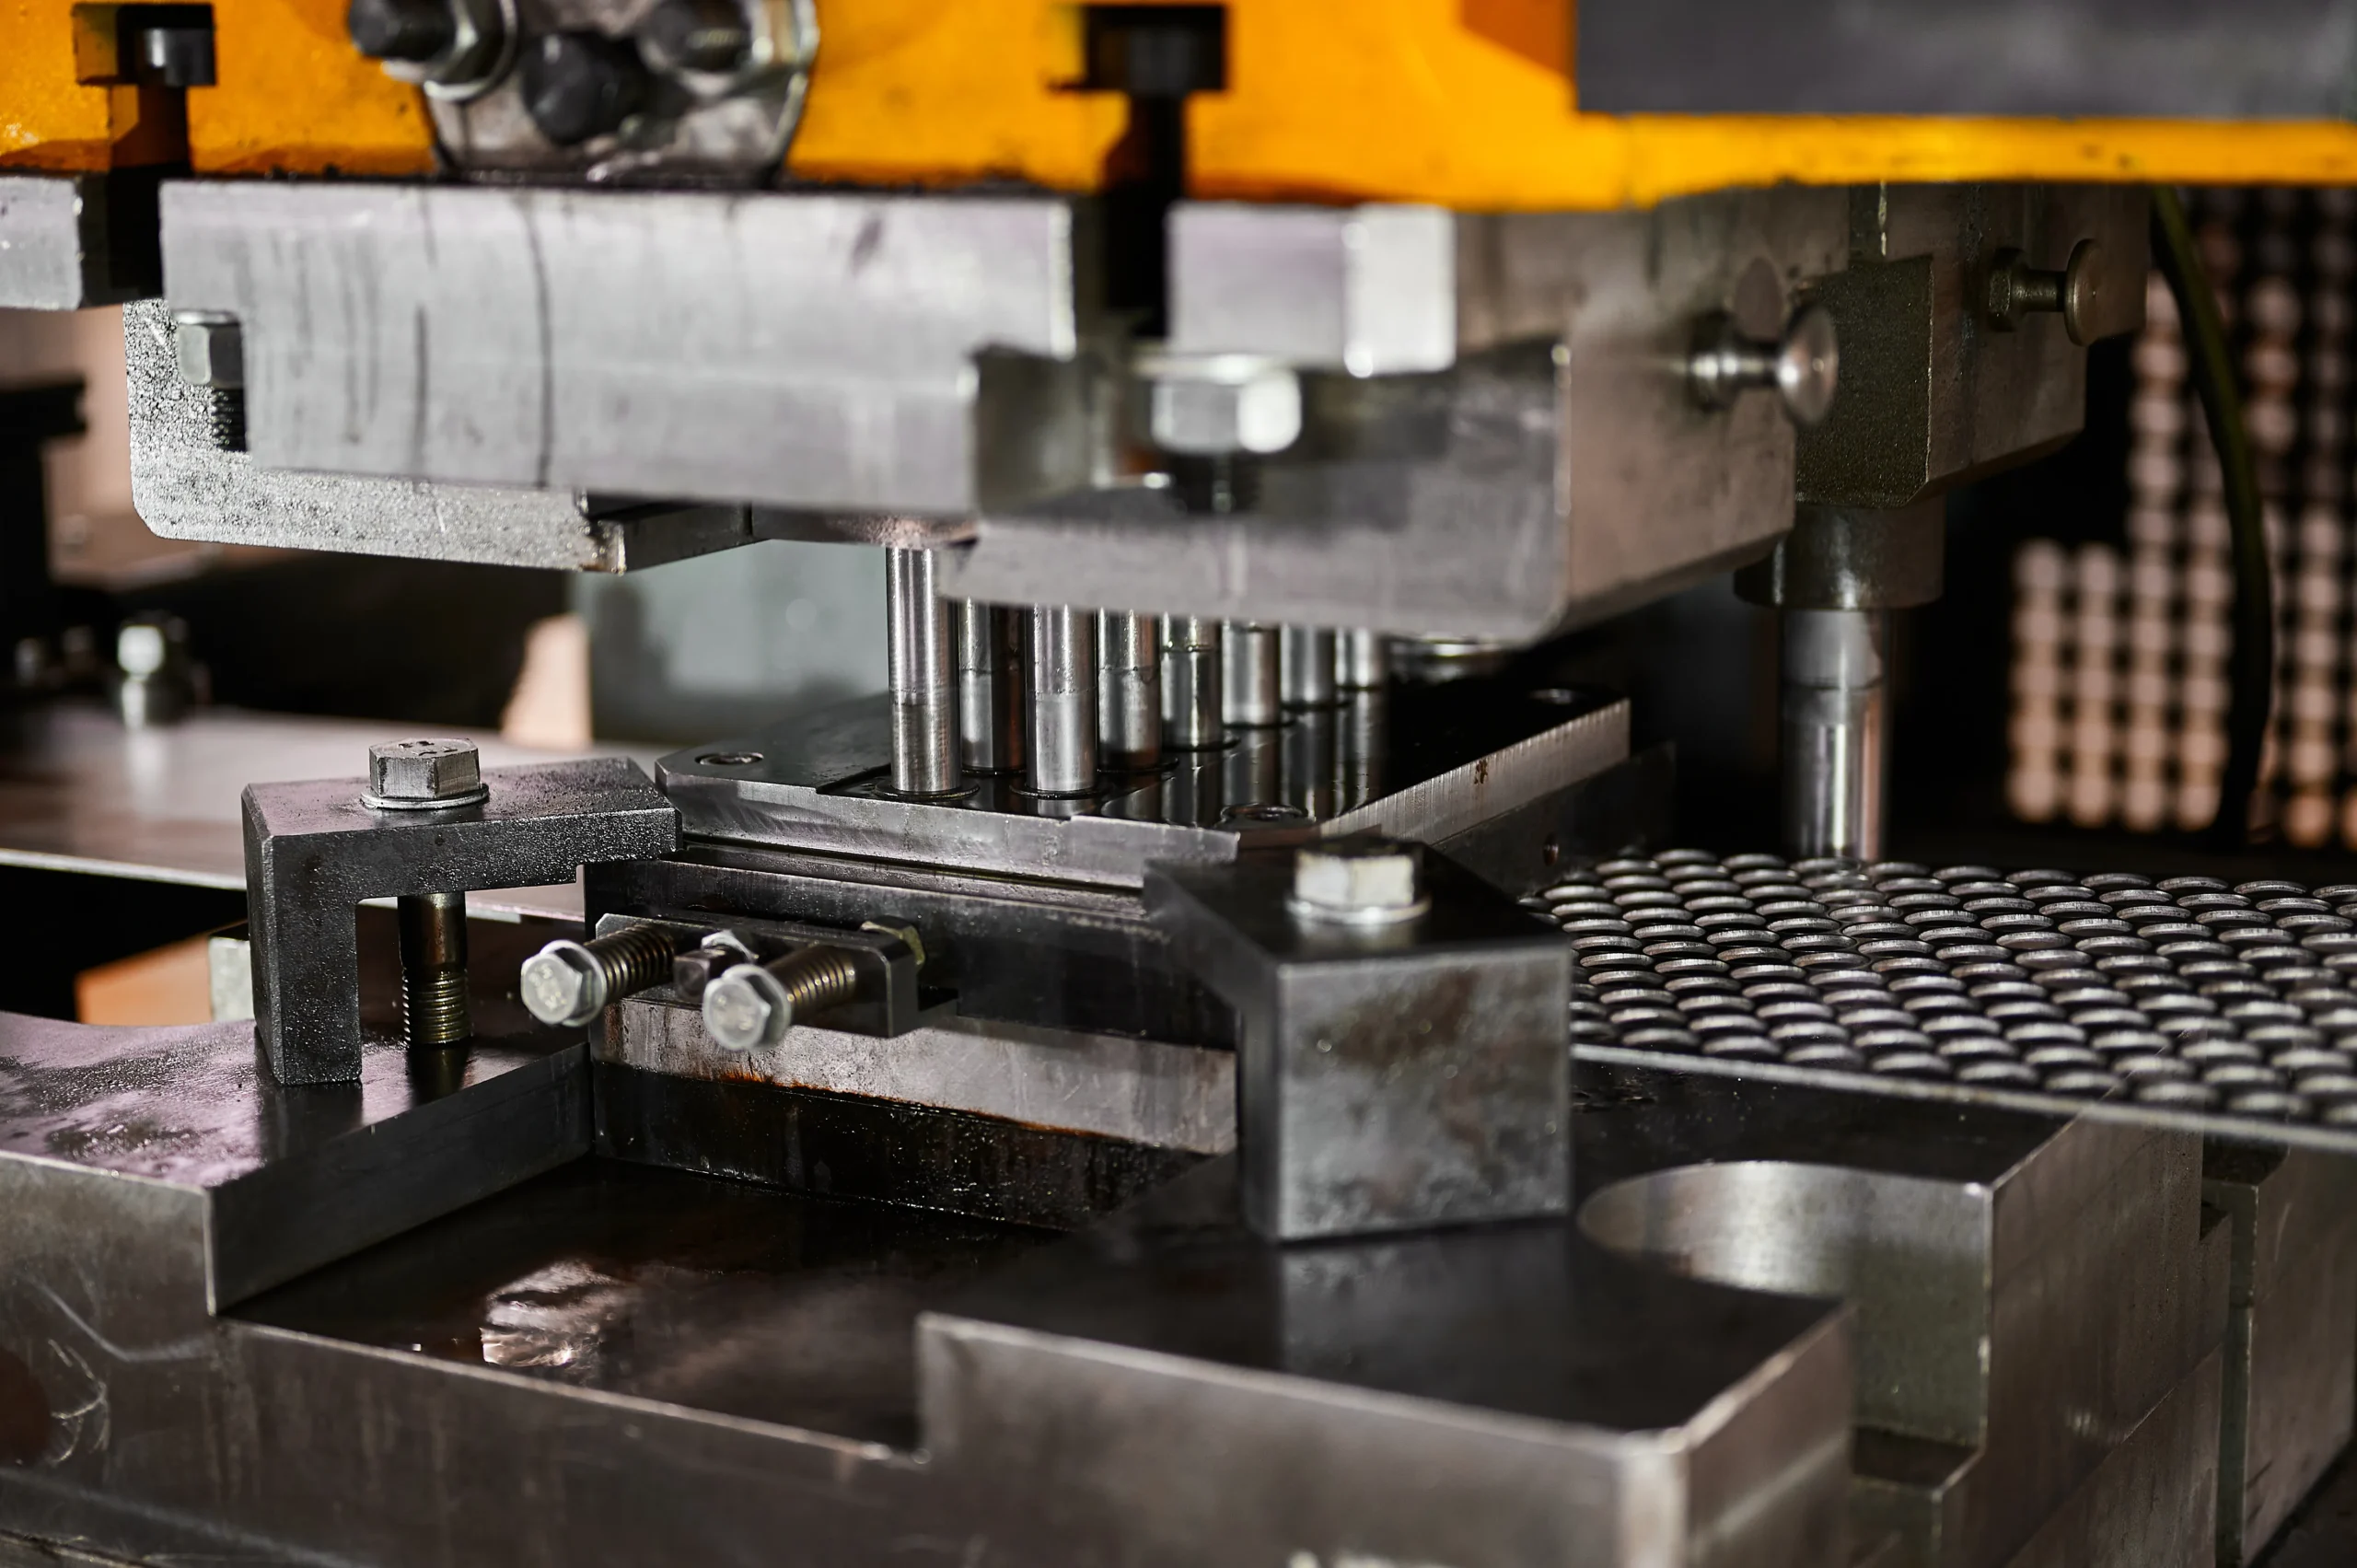
Manufacturers combine sheet metal stamping with robotic spot welding to build structural assemblies
19.1.3 What materials are used in sheet metal stamping?
Standard stamping materials include cold-rolled steel (SPCC), hot-rolled steel (SPHC), stainless steel (SUS304, SUS316), aluminum alloys (5052, 6061-T6), electro-galvanized steel (SECC), hot-dip galvanized steel (SGCC), brass, and copper strips. Material choice depends on tensile strength, corrosion resistance, and formability requirements.
19.1.4 What is the difference between sheet metal stamping and progressive die stamping?
Sheet metal stamping is a broad term encompassing all sheet-based press-forming operations, including single-stage and compound dies. Progressive die stamping is a specialized high-speed method that feeds a continuous strip through sequential inline stations inside a single die block, performing cutting, punching, and forming steps concurrently.
19.1.5 What industries use sheet metal stamping?
Sheet metal stamping is utilized across automotive body-in-white (BIW) and chassis manufacturing, electric vehicle (EV) battery systems, industrial machinery, HVAC enclosures, commercial electrical panels, consumer appliances, and precision electronics hardware.
19.1.6 How do I choose a sheet metal stamping supplier?
Select a supplier based on press tonnage range (e.g., 40T to 800T+), in-house die design and wire EDM toolroom capabilities, active quality certifications (ISO 9001 and IATF 16949), Level 3 PPAP submission readiness, DFM engineering support, and proven export packaging experience.
19.1.7 How do I request a sheet metal stamping RFQ?
To request an RFQ, provide 3D CAD models (STEP/IGES) and 2D engineering drawings (PDF) detailing critical tolerances and thread callouts. Specify the raw material grade, coil thickness, required surface plating or coating, secondary welding or assembly needs, annual volume forecasts, and delivery expectations.
19.2 Short answer blocks
19.2.1 Sheet metal stamping definition
Sheet metal stamping is an automated subtractive and cold-forming process that converts flat metal coils or sheets into custom components using press machines and matched die sets. The technology delivers high dimensional precision, repeatable batch quality, and low piece-part costs for scalable production runs.
19.2.2 Sheet metal stamping supplier selection summary
Selecting a reliable contract stamping partner requires assessing press machine versatility, in-house progressive die toolmaking capabilities, certified quality systems (ISO 9001 / IATF 16949), climate-controlled CMM inspection labs, and experienced B2B export logistics management.
19.2.3 Sheet metal stamping from Vietnam summary
Vietnam has established itself as an advantageous global hub for sheet metal stamping, combining cost-effective production, modern press lines, advanced wire EDM toolrooms, and skilled mechanical engineering talent. Sourcing from Vietnam provides international buyers with a de-risked “China+1” manufacturing base.
19.3 Featured snippet opportunities
19.3.1 Definition snippet: What is sheet metal stamping?
Sheet metal stamping is a precision metalworking process that shapes flat metal sheets or continuous coils using high-tonnage stamping presses and custom dies. The process performs operations such as blanking, piercing, bending, forming, and drawing to mass-produce automotive, industrial, and consumer components with tight tolerance repeatability.
19.3.2 List snippet: Sheet metal stamping process steps
The complete sheet metal stamping process follows five primary steps:
- Engineering & DFM Review: CAD model validation, bend radius analysis, and forming simulation.
- Tooling & Die Fabrication: CNC milling, vacuum heat treatment, and precision wire EDM die machining.
- Material Preparation: Uncoiling, roll-leveling, and automated servo strip feeding.
- Press Stamping Operations: Shearing, punching, bending, drawing, and in-die sensing.
- Quality Inspection & Finishing: CMM dimensional verification, deburring, plating, and VCI packaging.
19.3.3 Table snippet: Sheet metal stamping vs progressive die stamping
| Feature | Standard Sheet Metal Stamping | Progressive Die Stamping |
| Tooling Setup | Single-stage, compound, or modular dies | Integrated multi-station progressive die block |
| Production Speed | 10 to 40 parts per minute | 100 to 500+ parts per minute |
| Piece-Part Cost | Moderate at lower volumes | Lowest unit cost at mass scale |
| Optimal Order Volume | 1,000 to 20,000 units/year | 50,000+ units/year |
| Automation Level | Manual or automated robotic part manipulation | Fully automated continuous coil feeding |
19.3.4 Checklist snippet: How to choose a sheet metal stamping supplier
When evaluating a contract sheet metal stamping supplier, buyers should verify:
- Press Fleet Capacity: Range of mechanical, hydraulic, and servo presses (40T to 800T+).
- Toolroom Support: In-house CAD/CAM die design, wire EDM machining, and preventive die maintenance.
- Quality Certifications: Active ISO 9001 and IATF 16949 compliance with Level 3 PPAP submission readiness.
- Secondary Integration: In-house robotic welding, hardware insertion, and protective surface finishing.
- Export Capability: Proven track record serving US/EU buyers, VCI anti-corrosion packaging, and full customs documentation.
20. Internal Linking Strategy
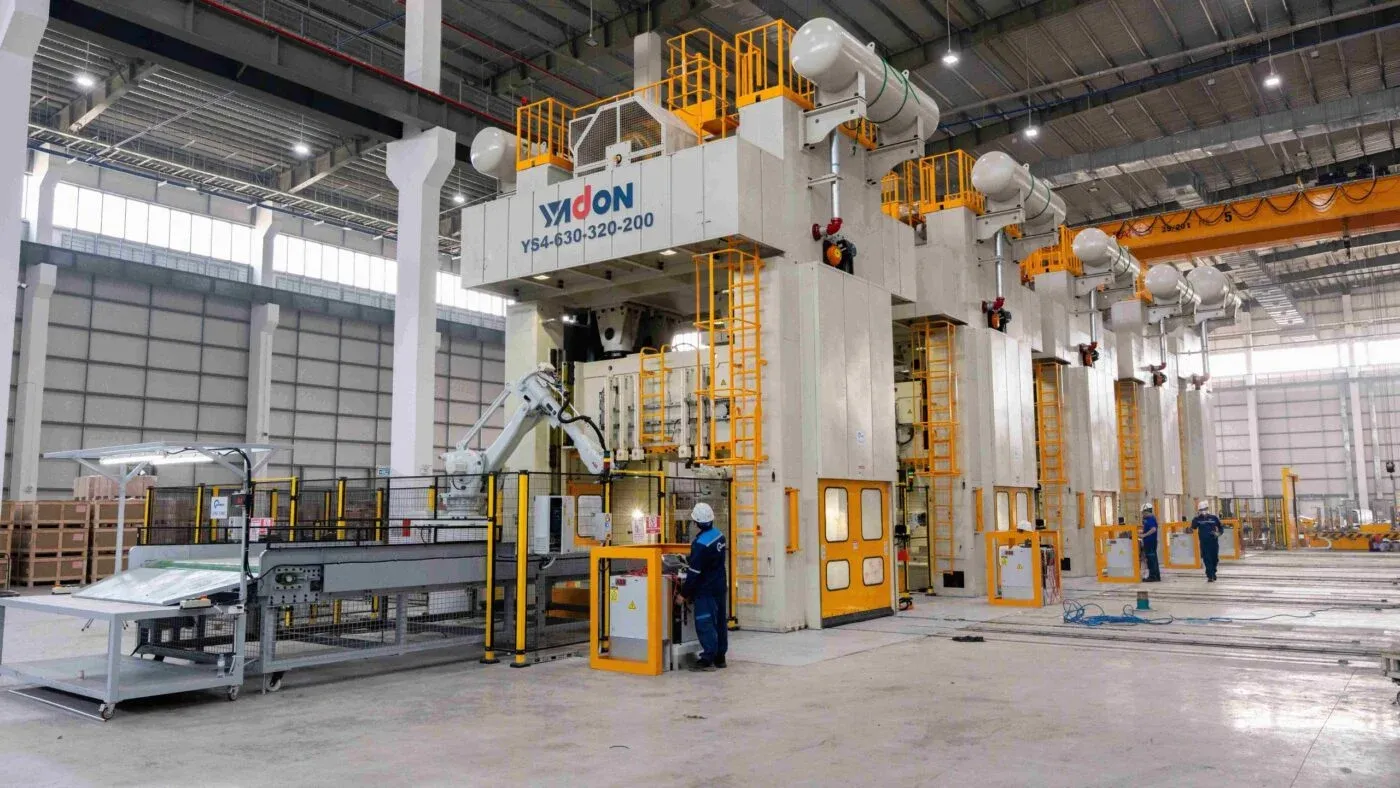
Sheet metal stamping delivers uniform edge quality and minimal burrs using sharp cutting dies
20.1 Parent service link
20.1.1 Metal stamping services
Explore our comprehensive [Metal Stamping Services] pillar page to understand the broader capabilities of cold-forming manufacturing, pressworking technologies, and turnkey tooling solutions for global industrial supply chains.
20.2 Metal stamping cluster links
20.2.1 Automotive metal stamping
Discover how high-tonnage press lines process body-in-white reinforcements, seat frame sub-assemblies, and EV battery structures on our dedicated [Automotive Metal Stamping] resource page.
20.2.2 Precision metal stamping
Learn about micro-tolerance capabilities, tungsten carbide die insert applications, and zero-burr edge quality standards on our [Precision Metal Stamping] cluster page.
20.2.3 Progressive die stamping
Review continuous coil-feeding workflows, stroke speed optimization, and multi-station tooling advantages in our detailed [Progressive Die Stamping] guide.
20.2.4 Metal stamping tooling
Understand die steel selection, springback compensation design, and preventive toolroom maintenance by reading our technical guide on [Metal Stamping Tooling].
20.3 Automotive stamping links
20.3.1 Automotive bracket stamping
See how high-speed stamping presses process thick-gauge carbon steel into rigid engine mounts, chassis gussets, and sensor brackets on our [Automotive Bracket Stamping] page.
20.3.2 Automotive stamping assembly
Explore integrated manufacturing workflows combining press forming with robotic spot welding, riveting, and automated hardware insertion on our [Automotive Stamping Assembly] resource.
20.3.3 RFQ automotive stamping supplier
Streamline your procurement timeline by accessing our step-by-step submission checklist and technical drawing requirements at [RFQ Automotive Stamping Supplier].
20.4 Supplier and sourcing links
20.4.1 Automotive stamping supplier Vietnam for US
Discover how Vietnamese contract manufacturers comply with US engineering standards, tariff regulations, and transoceanic shipping protocols at [Automotive Stamping Supplier Vietnam for US].
20.4.2 Automotive stamping supplier Vietnam for Europe
Learn about VCI anti-rust packaging, EN material standards, and Euro-centric quality compliance on our page for [Automotive Stamping Supplier Vietnam for Europe].
20.4.3 Alternative China stamping supplier
Examine supply chain resilience, risk mitigation, and dual-sourcing benefits in our strategic report on [Alternative China Stamping Supplier].
20.5 Tool and die links
20.5.1 Tool and die export manufacturer
Review in-house toolroom capabilities, CNC/wire EDM machining, and export die trial validation at [Tool and Die Export Manufacturer].
20.5.2 Automotive progressive die supplier Vietnam
Explore custom multi-station progressive die design and high-volume press production capabilities at [Automotive Progressive Die Supplier Vietnam].
21. Conversion Section: Request Sheet Metal Stamping RFQ
21.1 Why global buyers choose reliable sheet metal stamping suppliers
21.1.1 Lower production risk
Partnering with an experienced contract sheet metal stamping supplier mitigates production risks through standardized tool design, in-die sensor monitoring, and structured quality management systems. Standardized procedures prevent non-conforming parts from reaching customer assembly lines, eliminating downtime for global OEMs.
21.1.2 Better dimensional consistency
High-precision press systems equipped with rigid die shoes and precision guide pins ensure identical feature locations across millions of press cycles. Dimensional consistency simplifies automated robotic assembly and eliminates line fitment issues across complex vehicle and machinery assemblies.
21.1.3 Stronger tooling and quality control
Professional stamping partners maintain dedicated toolrooms for scheduled die inspection, punch regrinding, and preventive maintenance. In-house CMM laboratories and Level 3 PPAP documentation provide complete transparency and batch-to-batch traceability.
21.2 RFQ CTA strategy

Factory automation connects sheet metal stamping presses directly with downstream inspection systems
21.2.1 Request RFQ
Initiate your project quotation today by submitting your component requirements through our online portal to receive a detailed piece-price and tooling estimate from our engineering team.
21.2.2 Upload technical drawings
Share your 3D CAD models (STEP, IGES) alongside 2D PDF technical drawings with fully defined tolerances, material specifications, and surface finish callouts for instant engineering review.
21.2.3 Contact engineering team
Connect directly with Automech’s toolmakers and mechanical engineers to discuss custom die configurations, alloy formability, press tonnage demands, and production scheduling.
21.2.4 Request tooling feasibility review
Obtain an upfront tooling feasibility assessment analyzing strip stretch limits, springback behavior, punch clearances, and tonnage distribution prior to capital commitment.
21.2.5 Request stamping cost analysis
Request a comprehensive cost optimization analysis evaluating coil nesting layouts, material utilization rates, and progressive vs single-stage die economics.
21.2.6 Get sheet metal stamping quotation
Contact Automech today to receive a competitive, volume-tiered quotation for prototype development, pre-series runs, or mass-production sheet metal stamping projects in Vietnam.
22. FAQ Section
22.1 What is sheet metal stamping?
22.1.1 Sheet metal stamping is a manufacturing process that uses presses and dies to cut, bend, form, or draw sheet metal into specific shapes.
Sheet metal stamping is an automated cold-forming manufacturing operation where mechanical or hydraulic press machines drive custom-engineered tool and die sets into flat sheet metal stock. The process executes blanking, piercing, bending, forming, and drawing operations to produce durable, high-precision three-dimensional components with rapid cycle times.
22.2 What materials are used in sheet metal stamping?
22.2.1 Common materials include carbon steel, stainless steel, aluminum, galvanized steel, and other sheet metal grades.
Contract stamping facilities process a broad range of sheet alloys: cold-rolled commercial steel (SPCC), hot-rolled steel (SPHC), austenitic stainless steel (SUS304, SUS316), structural aluminum alloys (5052-H32, 6061-T6), electro-galvanized steel (SECC), hot-dip galvanized steel (SGCC), brass, and copper strips.
22.3 What is the difference between sheet metal stamping and progressive die stamping?
22.3.1 Sheet metal stamping is a broad forming method, while progressive die stamping uses multiple die stations for high-volume production.
Sheet metal stamping refers to the overarching category of pressworking operations using various die configurations (including single-stage and compound dies). Progressive die stamping is a specialized high-speed method that integrates sequential piercing, bending, and forming stations into a single continuous tool set, feeding continuous coils to complete a part at the final station.
22.4 What industries use sheet metal stamping?
22.4.1 Automotive, industrial machinery, electronics, appliances, and precision manufacturing industries use sheet metal stamping.
Sheet metal stamping is essential for automotive body-in-white (BIW) frameworks, EV battery enclosures, industrial machinery guards, commercial electrical control panels, consumer appliances, medical devices, and precision hardware assemblies.
22.5 How do I request a sheet metal stamping RFQ?
22.5.1 Submit technical drawings, CAD files, material specifications, thickness, tolerance, annual volume, surface finish, and delivery requirements.
To receive an accurate quotation, submit your 3D CAD files (STEP/IGES) and 2D engineering drawings (PDF) detailing critical tolerances and thread specifications. Specify exact raw material grades, sheet thickness, required surface finishing, secondary welding or assembly requirements, annual volume forecasts, and target delivery schedules.
Automech Mechanical Equipment and Solutions Joint Stock Company
Head Office: No. 285 Phuc Loi Street, Phuc Loi Ward, Hanoi City
Da Nang Branch: No. 20 Nguyen Sinh Sac Street, Hoa Khanh Ward, Da Nang City
Ho Chi Minh Branch: No. 84, Street No. 10, Van Phuc Urban Area, Hiep Binh Ward, Ho Chi Minh City
Factory No. 1: Automech Automation Equipment, Mold & Tool Manufacturing Factory – Automech Demo Center: Dinh Tram Industrial Park, Nenh Ward, Bac Ninh City, Vietnam
Factory No. 2: Automech Parts Manufacturing & Component Fabrication Factory: Viet Nhat Industrial Cluster, Xuan Cam Commune, Bac Ninh City, Vietnam
Hotline: 0987 899 347
Website: https://automechmfg.com/
Fanpage: https://www.facebook.com/automech.mfg/
YouTube: https://www.youtube.com/@Automechmfg